Manufacture of ready-to-install CNC long and short turned parts Ø 4–42 mm including secondary machining, hardening and surface technology.
Anton Huber Drehteile GmbH und Co. KG
Nusplingen (Baden-Württemberg)New on Amplifa
Machining with passion – turned parts since 1961
Anton Huber Drehteile GmbH und Co. KG manufactures ready-to-install long and short turned parts to drawing in Nusplingen. The range includes CNC long turned parts with diameters of 4 to 20 mm and CNC short turned parts from 6 to 42 mm, complemented by secondary machining such as drilling, milling, threading, burnishing and knurling work, grinding and polishing. In addition, the company offers downstream hardening processes (including case hardening, hardening and tempering, nitrocarburizing, induction hardening) as well as a wide range of surface treatments such as zinc plating, nickel plating, anodizing, phosphating and Delta-Tone. Materials include free-cutting and tempering steels, structural steels, case-hardening steels, stainless steels, brass, aluminium and engineering plastics such as POM, PA6 and PA6 GF. Customers come from the automotive industry (OEMs and suppliers), medical technology, electrical engineering and the furniture industry. On request, part cleaning, assembly of sub-assemblies, SPC-monitored production, first article inspection reports and IMDS entries are provided. The family business, founded in 1961, has been run since 2022 by Linda and Thomas Essigbeck in the third generation.
- Site
- Nusplingen
- Processes
- CNC long turning, CNC short turning, Cross drilling, Cross tapping, Milling, Thread cutting, Burnishing, Knurling
- Materials
- Free-cutting and tempering steels, Structural steels, Case-hardening steels, Stainless steels, Brass and special alloys, Aluminium, POM, PA6
- Certificates
- DIN EN ISO 9001:2015, ISO 9001 (DIN EN ISO 9001:2015)
- Founded
- 1961
- Industries
- Automotive industry (OEMs and suppliers), Medical technology, Electrical engineering, Furniture industry
- 01
Consulting/design optimization
- 02
CNC long turning Ø 4–20 mm
- 03
CNC short turning Ø 6–42 mm
- 04
Secondary machining (drilling, milling, threading, burnishing, knurling,
- 05
Grinding/polishing/blasting
- 06
Hardening processes
- 07
Surface treatment
- 08
Part cleaning
- 09
Assembly
- 10
Inspection and shipping
Materials and processes
Free-cutting and tempering steels
Standard materials for economical turned parts in series production.
Structural steels
For mechanically stressed components manufactured to drawing.
Case-hardening steels
Suitable for case-hardened, wear-resistant turned parts.
Stainless steels
For corrosion-exposed applications, e.g. in medical technology and electrical engineering.
Brass and special alloys
For electrically conductive and decorative turned parts.
Aluminium
Lightweight components, optionally anodized.
POM
Engineering polymer for precise, unreinforced plastic turned parts.
PA6 / PA6 GF
Tough-elastic or glass-fibre-reinforced polymers for technical applications.
Hardening processes
Case hardening/carbonitriding, hardening/tempering, hardening and tempering, annealing, nitrocarburizing, induction hardening.
Surface treatment
Zinc plating, nickel plating, copper plating, anodizing, phosphating, Delta-Tone/Geomet and more.
Part cleaning
Enclosed washing system using hydrocarbons with vapour degreasing.
Nusplingen site
Nusplingen
DEProduction and administration (headquarters)
- Materials
- Steels, stainless steels, brass, aluminium, POM, PA6
- CNC long turning machines Ø 4–20 mm
- CNC short turning machines Ø 6–42 mm
- Enclosed washing system (hydrocarbons, vapour degreasing)
- Secondary machining machines (drilling, milling, threading)
- Grinding machines
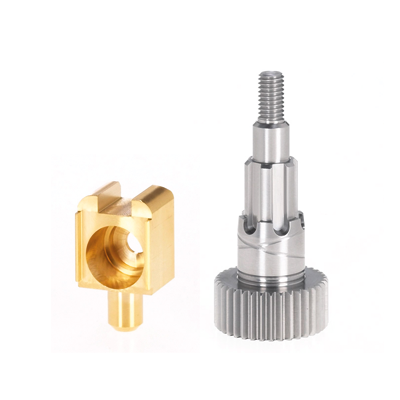
Turned parts and assemblies
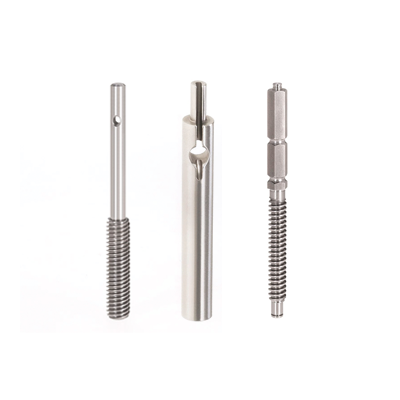
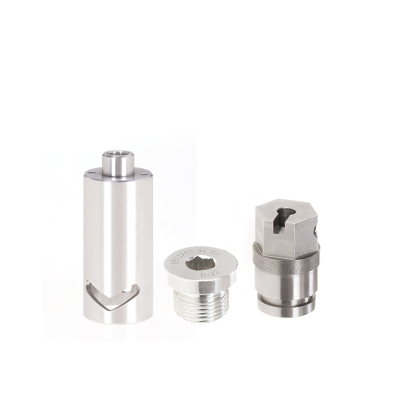
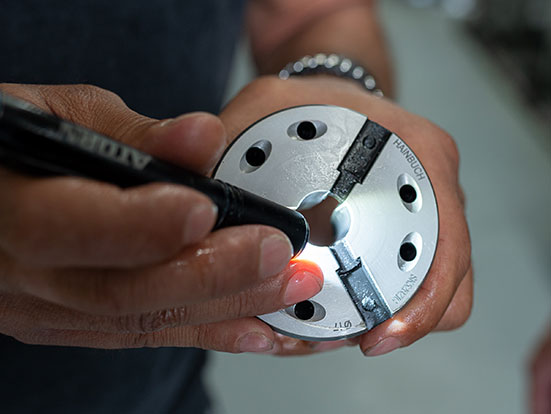
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| CNC long turningMachining | – | – | – | – | Free-cutting and tempering steels, Structural steels, Case-hardening steels, Stainless steels, Brass and special alloys, Aluminium, POM, PA6, PA6 GF |
| CNC short turningMachining | – | – | – | – | Free-cutting and tempering steels, Structural steels, Case-hardening steels, Stainless steels, Brass and special alloys, Aluminium, POM, PA6, PA6 GF |
| Cross drillingMachining | – | – | – | – | – |
| Cross tappingMachining | – | – | – | – | – |
| MillingMachining | – | – | – | – | – |
| Thread cuttingMachining | – | – | – | – | – |
| BurnishingMachining | – | – | – | – | – |
| KnurlingForming | – | – | – | – | – |
| ReamingMachining | – | – | – | – | – |
| Thread rollingForming | – | – | – | – | – |
| External and internal grindingMachining | – | – | – | – | – |
| Plunge and through-feed grindingMachining | – | – | – | – | – |
| Vibratory finishingSurface | – | – | – | – | – |
| Glass bead blastingSurface | – | – | – | – | – |
| High-gloss polishingSurface | – | – | – | – | – |
| Case hardening/carbonitridingHeat treatment | – | – | – | – | – |
| Hardening and temperingHeat treatment | – | – | – | – | – |
| Hardening and tempering (Vergüten)Heat treatment | – | – | – | – | – |
| AnnealingHeat treatment | – | – | – | – | – |
| NitrocarburizingHeat treatment | – | – | – | – | – |
| Induction hardeningHeat treatment | – | – | – | – | – |
| Sand blastingSurface | – | – | – | – | – |
| Blackening (burnishing)Surface | – | – | – | – | – |
| Phosphating (zinc/manganese phosphating)Surface | – | – | – | – | – |
| PaintingSurface | – | – | – | – | – |
| Gold platingSurface | – | – | – | – | – |
| Zinc plating (Fe/ZN, Fe/Ni, Cr6-free)Surface | – | – | – | – | – |
| Nickel plating (electroplated and electroless)Surface | – | – | – | – | – |
| Copper plating / copper-nickelSurface | – | – | – | – | – |
| SealingSurface | – | – | – | – | – |
| AnodizingSurface | – | – | – | – | Aluminium |
| Delta-Tone®, Delta-Seal®, Delta-Coll®, Geomet®, Hart-Coat®, Durni-Coat®Surface | – | – | – | – | – |
| Part cleaning with hydrocarbons (washing system, vapour degreasing)Surface | – | – | – | – | – |
| Assembly of sub-assembliesAssembly | – | – | – | – | – |
| Inspection: first article inspection reports, outgoing goods inspection to AQL, machine capabilityInspection | – | – | – | – | – |
| Design optimization/consulting in planning and developmentEngineering | – | – | – | – | – |
3 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| CNC long turning machine | – | – | Turning diameter Ø 4–20 mm | – | Nusplingen |
| CNC short turning machine | – | – | Turning diameter Ø 6–42 mm | – | Nusplingen |
| Enclosed washing system (hydrocarbons, vapour degreasing) | – | – | – | – | Nusplingen |
Additional services
Quality
The company is certified to DIN EN ISO 9001:2015 and works according to the TQM approach. On request, SPC-monitored production, first article inspection reports, outgoing goods inspection to AQL, machine capability studies and IMDS entries are available.
| Evidence | Nusplingen |
|---|---|
| ISO 9001 (DIN EN ISO 9001:2015) |
Company history
- 1961
Company founded by Anton Huber in Nusplingen; workshop in a residential house.
- 1978
Relocation to the thoroughly renovated corduroy factory in Nusplingen.
- 1986
Barbara Butz joins the company and takes over management of the commercial department.
- 1991
Roland Butz joins the company.
- 1993
Relocation to the factory hall of the former Götz company in Nusplingen, first conversion.
- 1995
Expansion: finished parts warehouse, offices, meeting and training rooms.
- 1999
Company taken over by Barbara and Roland Butz (2nd generation).
- 2016
Thomas Essigbeck joins; realignment of production planning and digitalization.
- 2022
Linda and Thomas Essigbeck take over the company as of 01.01.2022 (3rd generation).