Tungsten carbide-tipped wear tools, tool systems and wear protection solutions – from in-house carbide production to assembly
BETEK GmbH & Co. KG
78733 Aichhalden (DE) · Charlotte, NC (USA) · Taicang (CN)New on Amplifa
Tungsten carbide tools from in-house production
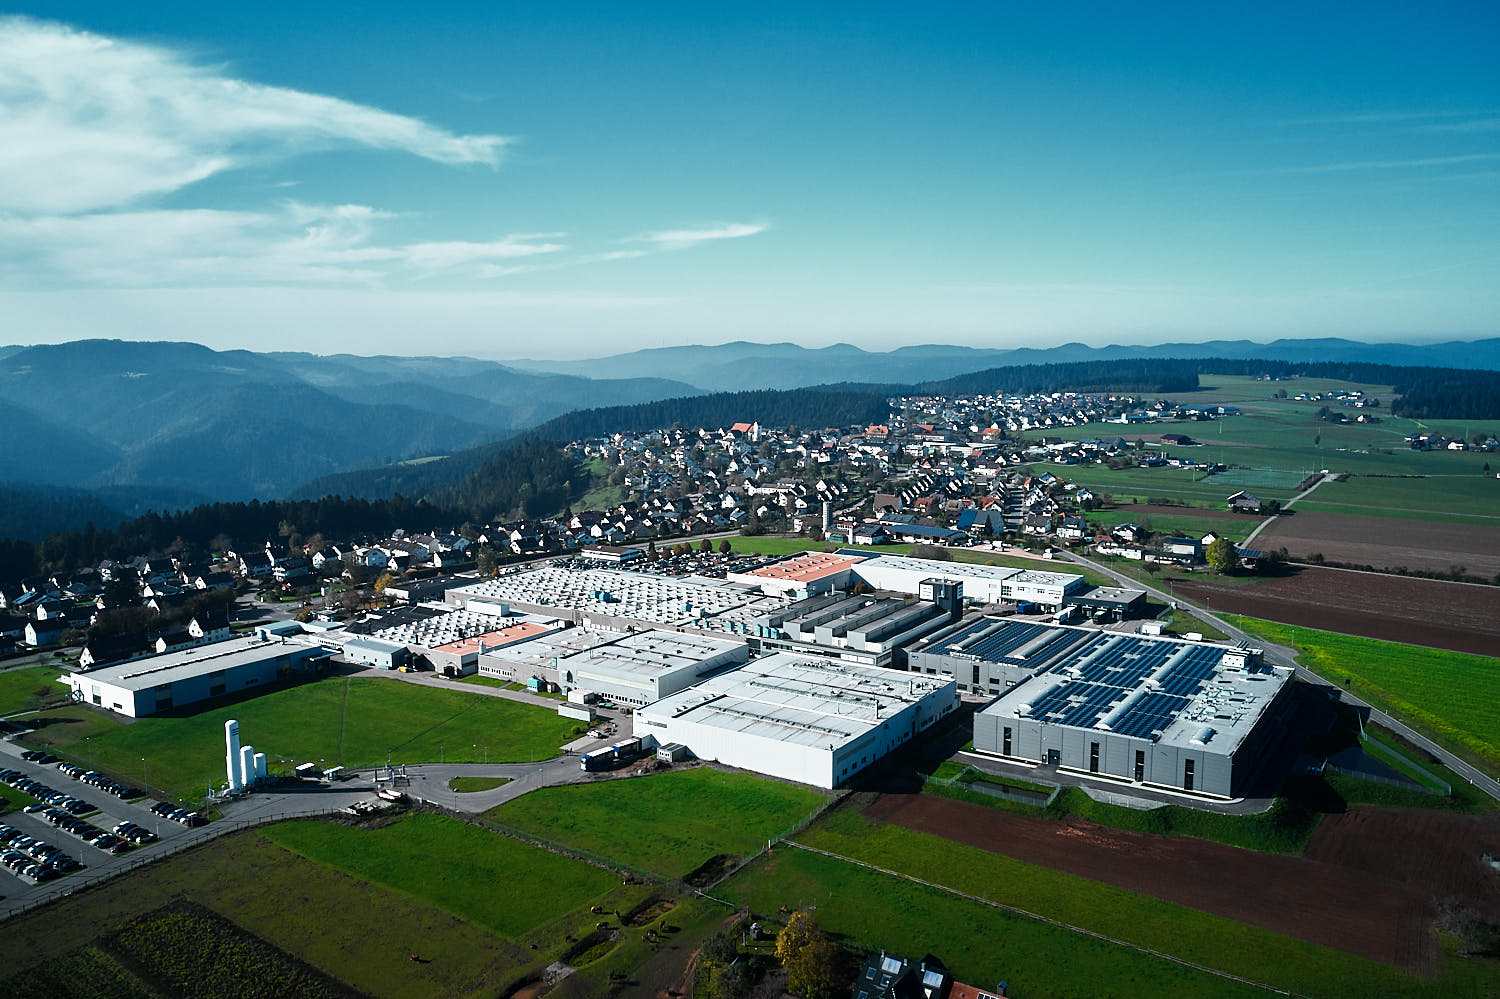
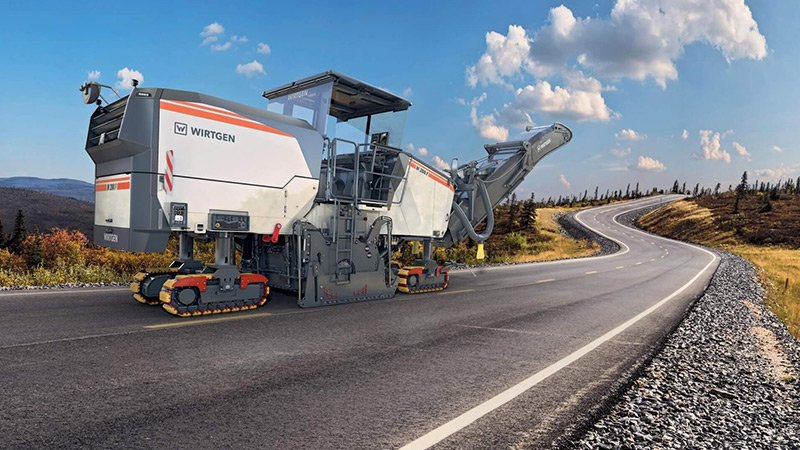
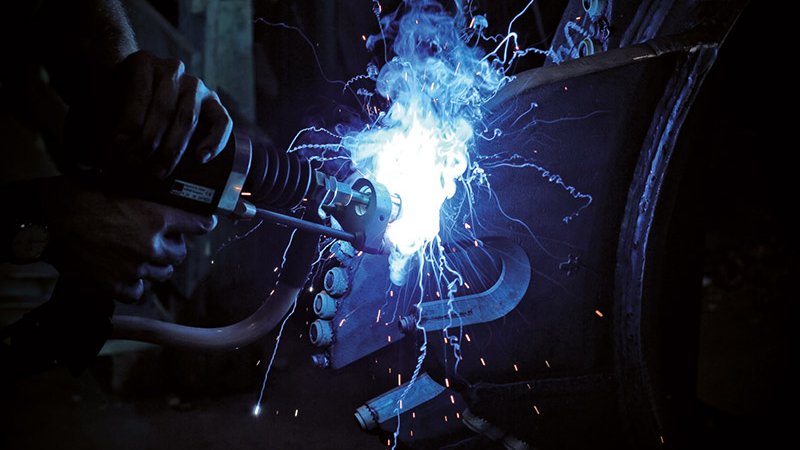
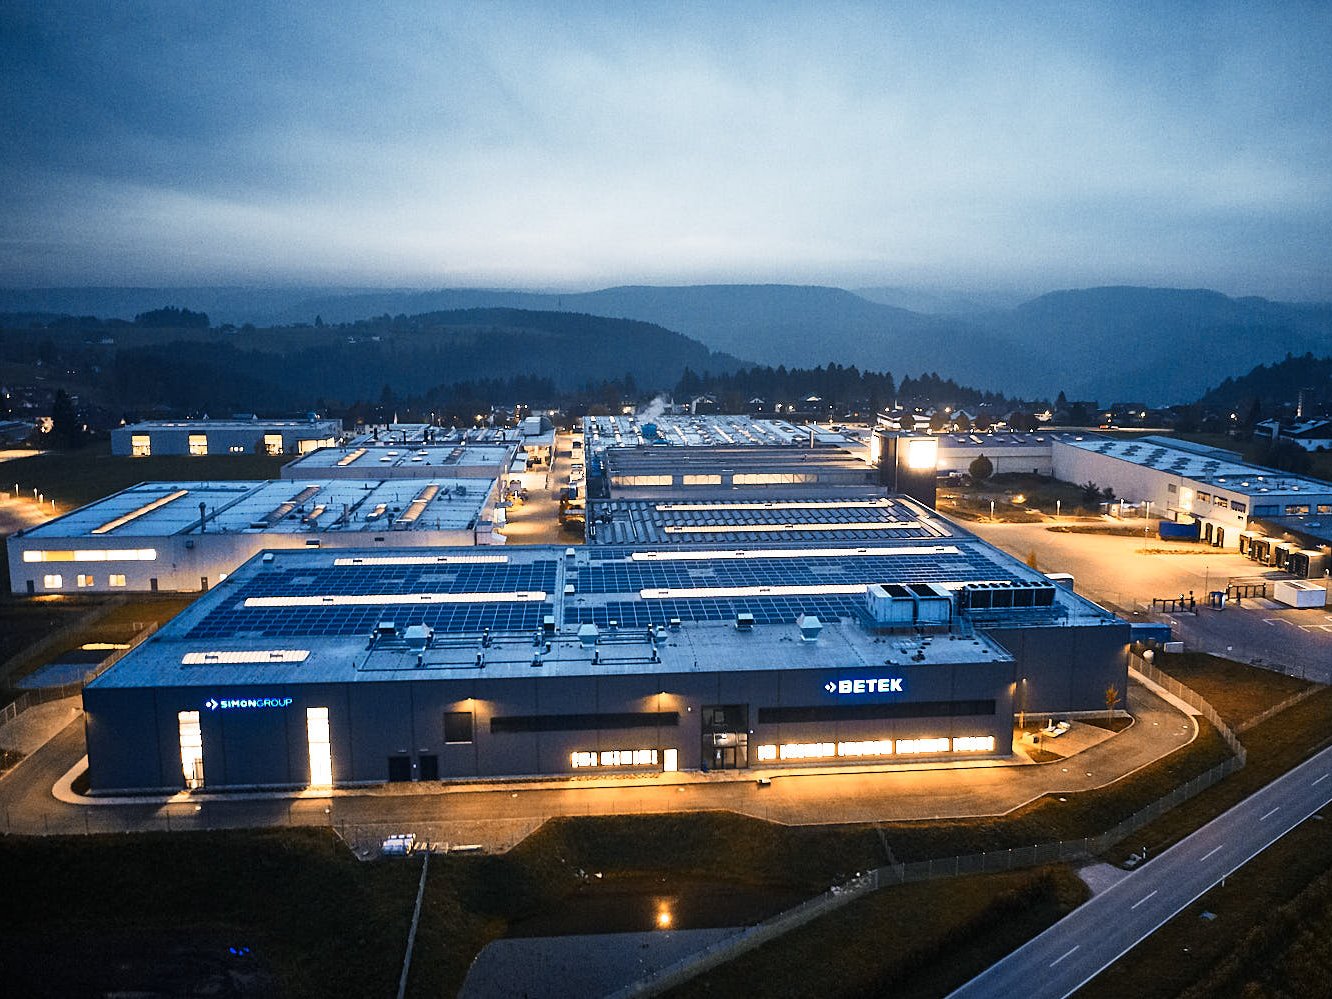
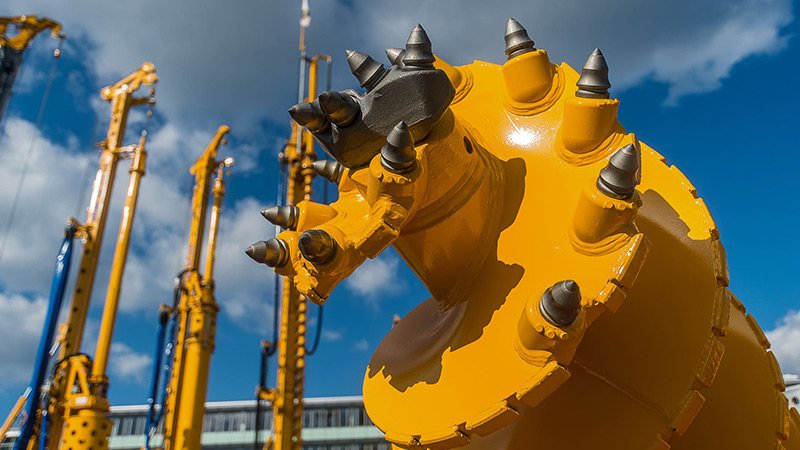
BETEK GmbH & Co. KG is a manufacturer of tungsten carbide-tipped wear tools, tool systems and wear protection solutions headquartered in Aichhalden in the Black Forest. At its headquarters, the company carries out the entire manufacturing process: carbide is milled from tungsten carbide, spray-dried, pressed with press forces of up to 120 t and sintered in HIP sintering furnaces. Subsequently, carbide tips are joined to steel carriers using automated brazing technology at 750 °C to 1,100 °C, given wear protection via the BeCoat® PTA process, assembled and packaged automatically. Customers are machinery manufacturers from road construction, mining, tunneling, special civil engineering, agricultural technology, mineral extraction and recycling, including Wirtgen, CLAAS and Lemken. Under the SITEK brand, spikes for winter tires are also produced; an in-house carbide recycling operation processes around 80 t per year. A production facility in Taicang (China) and a sales office in Charlotte (USA) complement the Aichhalden site.
- Site
- Aichhalden
- Processes
- Carbide production (milling process), Spray drying (spray tower), Carbide pressing (press force up to 120 t), Sintering (HIP sintering furnaces, up to 36 hours), QA inspection (testing laboratory), High-pressure sintering process, Brazing (manual, partially and fully automated, 750 °C to 1,100 °C), Adhesive bonding techniques
- Materials
- Tungsten carbide (hard metal), Tungsten carbide (tungsten carbide), Steel, Carbide powder, Iron powder, Carbide grit, Silver brazing alloy, Copper brazing alloy
- Certificates
- ISO 9001:2015, ISO 14001:2015, ISO 45001:2018, ISO 50001:2018, IATF 16949:2016, ISO 9001, ISO 14001, ISO 45001, ISO 50001, IATF 16949
- Founded
- 1981
- Industries
- Road construction, Mining, Tunneling, Special civil engineering, Agricultural technology, Mineral extraction / crushing & mixing
- 01
Material/recipe development
- 02
Carbide production (milling process, spray drying)
- 03
Pressing (up to 120 t press force)
- 04
HIP sintering (up to 36 hours)
- 05
Toolmaking
- 06
Brazing (750–1,100 °C, manual/partially/fully automated)
- 07
BeCoat® PTA wear protection coating
- 08
Hardening and tempering process (heat treatment)
- 09
Assembly (fully and semi-automated)
- 10
Automated packaging
- 11
Carbide recycling
Materials and processes
Tungsten carbide (hard metal)
Wear-resistant tool tips for milling, crushing and cutting tools
Steel / chromium and manganese steel
Tool shafts and sleeves as carrier material for the carbide tipping
Silver brazing alloy
Joining compound between carbide tip and steel shaft with stress-compensating behavior
Copper brazing alloy
Brazing material for joining at temperatures of 750 °C to 1,100 °C
Polycrystalline diamond (PCD)
Tool tips for surface layer rehabilitation and fine milling applications
BeCoat® PTA coating
Plasma Transferred Arc wear protection with iron powder and carbide grit
Carbide powder / granulate
In-house powder and granulate production for carbide manufacturing and for sale
Locations
Aichhalden
DEHeadquarters, development and production
- Materials
- Carbide, tungsten carbide, steel
- Carbide presses (up to 120 t press force)
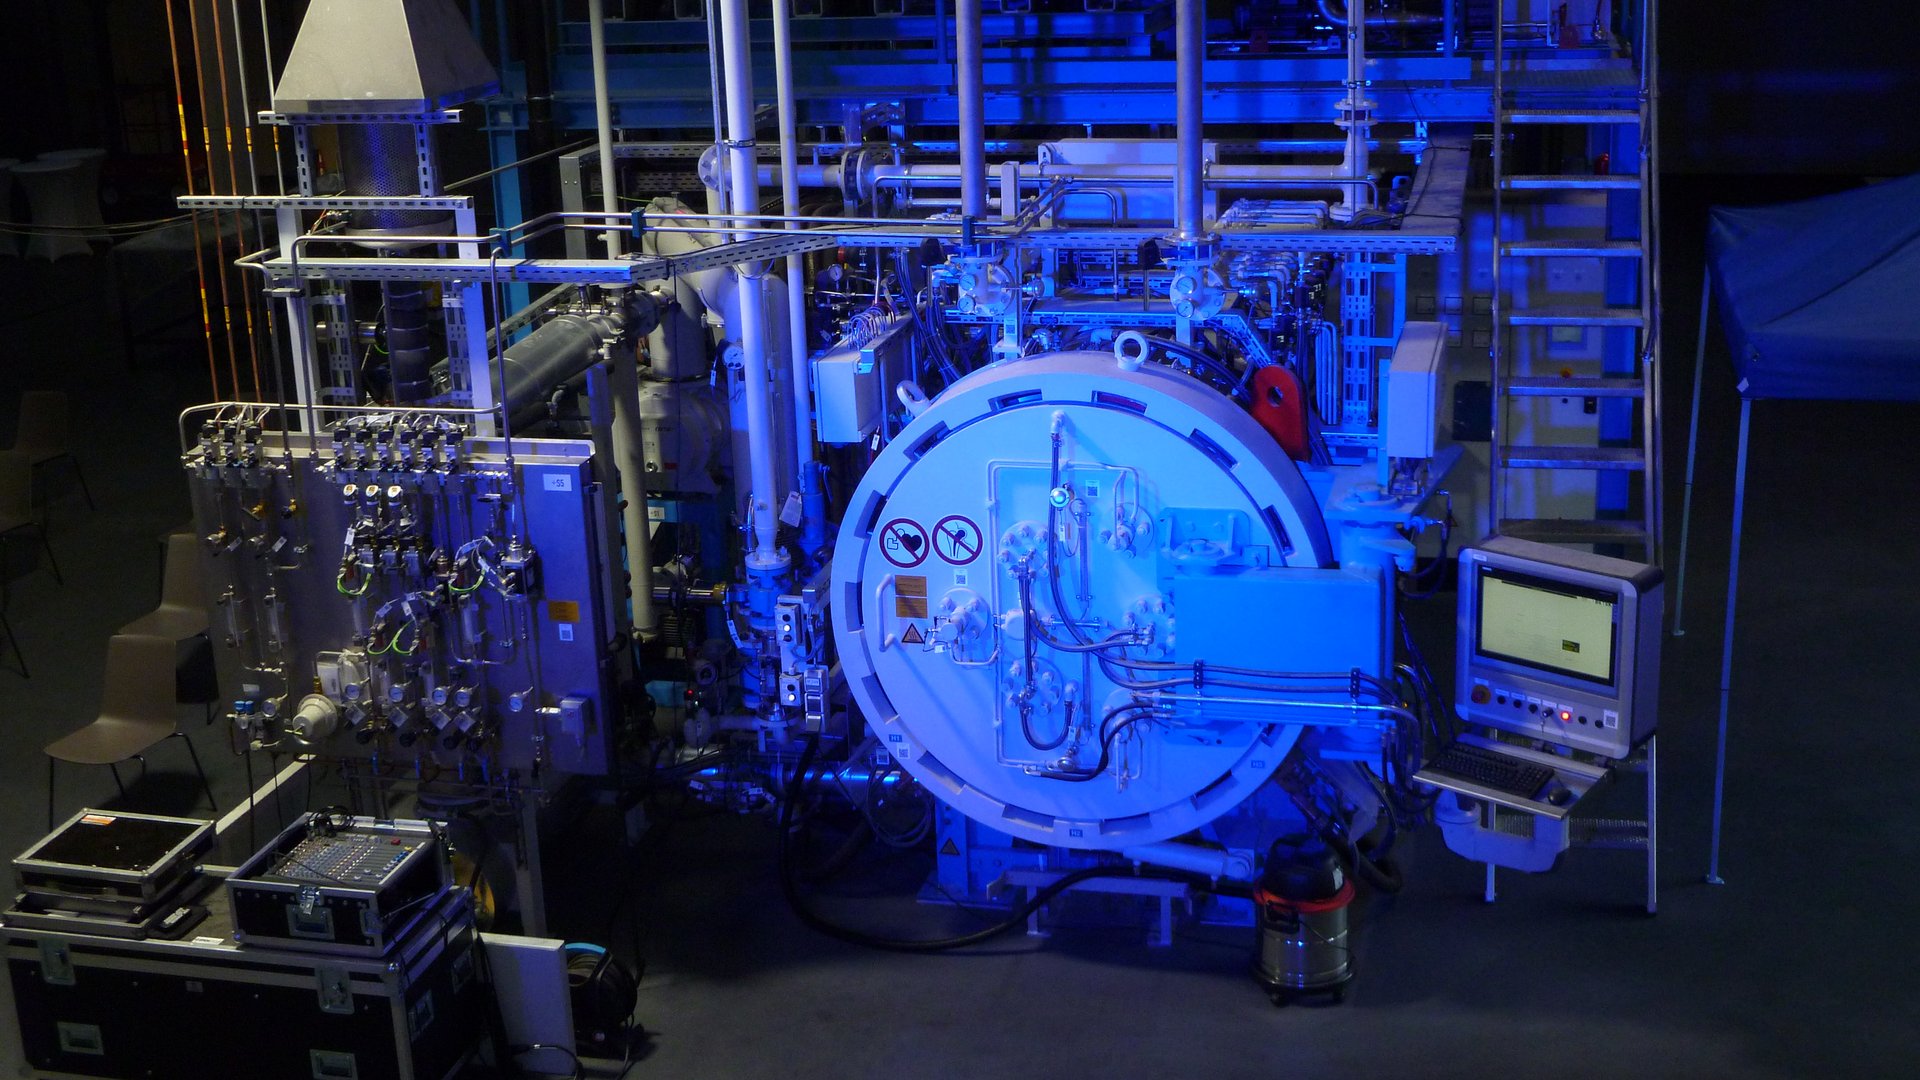
- HIP sintering furnaces (sintering process up to 36 hours)
- Spray towers
- 49 rotary indexing automation machines (SITEK)
- more than 20 brazing systems (750–1,100 °C)
- Robot-assisted brazing
- PTA welding systems (BeCoat®)
- Assembly machines
- Packaging robots (24/7)
- Camera and laser measurement technology
- Test benches
Charlotte, NC
USAWarehouse and sales office (BETEK Tools, Inc.)
Taicang
CNProduction facility (BETEK Tools Taicang Ltd.)
Components and tools
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Carbide production (milling process)Engineering | – | – | – | – | Carbide, Tungsten carbide |
| Spray drying (spray tower)Engineering | – | – | – | – | Carbide powder, pressable granulate |
| Carbide pressing (press force up to 120 t)Forming | – | – | – | – | Carbide |
| Sintering (HIP sintering furnaces, up to 36 hours)Casting | – | – | – | – | Carbide |
| QA inspection (testing laboratory)Testing | – | – | – | – | – |
| High-pressure sintering processCasting | – | – | – | – | Carbide |
| Brazing (manual, partially and fully automated, 750 °C to 1,100 °C)Joining | – | – | – | – | Carbide, Steel |
| Adhesive bonding techniquesJoining | – | – | – | – | Carbide, Steel |
| WeldingJoining | – | – | – | – | Carbide, Steel |
| Tipping (brazing preparation)Assembly | – | – | – | – | Carbide, Steel |
| Sand blastingSurface | – | – | – | – | Carbide, Steel |
| BeCoat® wear protection (PTA process, Plasma Transferred Arc)Surface | – | – | – | – | Iron powder, Carbide powder, Carbide grit |
| Assembly (fully and semi-automated assembly machines)Assembly | – | – | – | – | Carbide, Steel |
| Assembly (press-fitting of carbide studs, press-fit assemblies)Assembly | – | – | – | – | Carbide, Steel |
| Hardening and tempering processHeat treatment | – | – | – | – | Carbide, Steel |
| Automated packaging, labeling, palletizingAssembly | – | – | – | – | – |
| Cold extrusion pressingForming | – | – | – | – | Steel |
| Carbide recycling (de-brazing, grade-pure recycling)Engineering | – | – | – | – | Carbide, Steel |
| Coating removal process (stripping of PVD and CVD coatings)Surface | – | – | – | – | Carbide |
| Zinc recycling processSurface | – | – | – | – | Carbide, Zinc |
| Material/recipe developmentEngineering | – | – | – | – | Carbide |
| Granulate preparation (carbide powder)Engineering | – | – | – | – | Carbide powder |
| Manufacture of carbide studsCasting | – | – | – | – | Carbide |
| Sleeve productionAssembly | – | – | – | – | Steel |
| ToolmakingEngineering | – | – | – | – | – |
| Maintenance, building of samples, production of small seriesEngineering | – | – | – | – | – |
| Manufacture of sintered partsCasting | – | – | – | – | Sintered parts |
| Corrosion testingTesting | – | – | – | – | – |
| Climate testingTesting | – | – | – | – | – |
| Coating thickness measurementsTesting | – | – | – | – | – |
| Wear testing of carbide gradesTesting | – | – | – | – | Carbide |
| Brazing (brazing process under inert protective gas)Joining | – | – | – | – | tungsten carbide, steel |
| Brazing shear strength testingTesting | – | – | – | – | tungsten carbide, steel |
12 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| Carbide presses | – | – | Press force up to 120 t | – | Aichhalden |
| HIP sintering furnaces | – | – | Sintering process up to 36 hours | – | Aichhalden |
| Spray towers | – | Several | – | – | Aichhalden |
| Rotary indexing automation machines | – | 49 | – | – | Aichhalden (SITEK) |
| Brazing systems | – | über 20 | Temperature range 750 °C to 1,100 °C | – | Aichhalden |
| Assembly machines | – | – | fully and semi-automated | – | Aichhalden |
| Packaging robots | – | – | Millions-of-parts range, 24/7 | – | Aichhalden |
| PTA welding systems (Plasma Transferred Arc) | – | – | – | – | Aichhalden |
| Camera and laser measurement technology | – | – | – | – | Aichhalden (SITEK) |
| Robots for robot-assisted brazing | – | – | – | – | Aichhalden |
| Milling processes (milling balls) | – | – | – | – | Aichhalden |
| Test benches | – | – | – | – | Aichhalden (SITEK) |
Additional services
Reference customers
Quality management
At BETEK, the entire manufacturing chain undergoes continuous quality inspection, including automated camera and laser measurement, brazing shear strength tests and wear testing of the carbide grades. In the in-house testing laboratory SIMON Analytics, corrosion, climate and coating thickness tests as well as special tests are performed.
| Evidence | Aichhalden |
|---|---|
| ISO 9001 | |
| ISO 14001 | |
| ISO 45001 | |
| ISO 50001 | |
| IATF 16949 |
History
- 1918
Founding of the company Karl Simon (refinement of components for the local clock industry)
- 1962
Start of spike production (later under SITEK)
- 1981
Betek emerges from the company Karl Simon; first orders: carbide tools for coal mining
- 1989
Spike business is transferred to SITEK
- 1992
SIMON GROUP (and thus BETEK) becomes a subsidiary of INDUS Holding AG
- 2015
Establishment of an in-house production facility in Taicang, China