Manufacturer of rolling mill rolls in composite cast, chilled cast iron, cast steel and semi-steel for rolling mills worldwide.
Eisenwerk Sulzau-Werfen R. & E. Weinberger Aktiengesellschaft
Tenneck (Werfen), AustriaNew on Amplifa
Our Tradition – Shaping the Future
Eisenwerk Sulzau-Werfen (ESW) is a manufacturer of rolls for steel forming with origins dating back to 1770. The company produces composite cast rolls using the horizontal centrifugal casting process: a highly alloyed shell sleeve is spun into a rotating forged steel mould and subsequently filled with core material by static casting. In addition to composite cast rolls, chilled cast iron, cast steel and semi-steel rolls are produced. The value chain covers melting of the charge materials in five induction furnaces (3 to 24 t), heat treatment, machining by turning, milling and grinding, fully automatic ultrasonic testing as well as assembly of accessory parts and technical after-sales service. Finished rolls weigh up to 42 tonnes with lengths up to 9 m and diameters up to 1,500 mm. The rolls are used in hot strip mills (HSM), casting and rolling plants (CSP/ESP), heavy plate and Steckel mills. The site is located in Tenneck (Werfen), Austria; with 299 employees the export share is 98.1 percent.
- Site
- Tenneck
- Processes
- Composite cast rolls by horizontal centrifugal casting (shell sleeve) with static casting of the, Melting of charge materials (steel and roll scrap, pig iron, alloying elements) in, Chilled cast iron rolls by static casting, Cast steel and semi-steel rolls, Heat treatment (annealing) of rolls, Machining: turning, milling, grinding of rolls, Assembly of accessory parts (rings & accessories) on rolls, Ultrasonic testing (fully automatic testing system)
- Materials
- Roll shell iron (highly alloyed), Chilled cast iron, Cast steel, Semi-steel, Pig iron, Forged steel (moulds), Wear-resistant alloy as shell material
- Certificates
- ISO 9001:2015, ISO 14001:2015, EcoVadis Bronze Medal
- Founded
- 1770
- Employees
- 299
- Industries
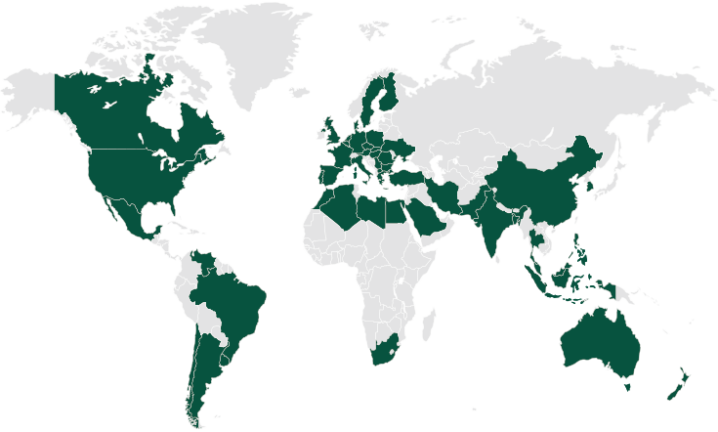
- Steel industry, Hot strip mills (HSM), Casting and rolling plants (CSP/ESP), Heavy plate rolling mills, Steckel mills, Casting and rolling plants (CSP/ESP)
- 01
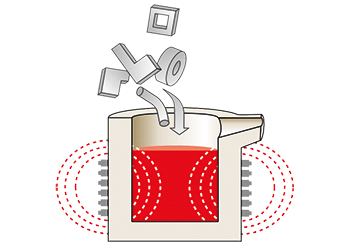
Melting of the charge materials (steel and roll scrap, pig iron,
- 02
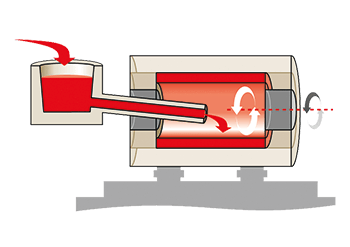
Horizontal centrifugal casting of the shell sleeve from highly alloyed roll
- 03
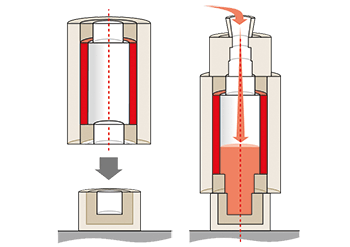
Static casting of the core material into the solidified shell sleeve
- 04
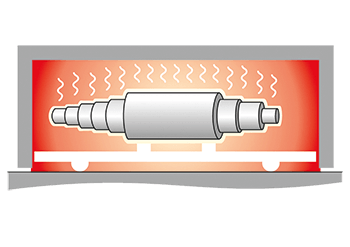
Heat treatment (annealing), depending on roll type up to six weeks
- 05
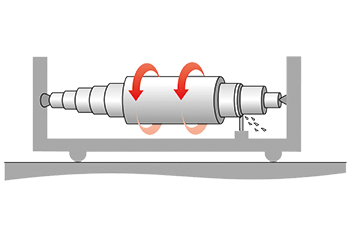
Machining: turning, milling, grinding
- 06
Ultrasonic testing and final inspection
- 07
Assembly of rings and accessory parts
- 08
Technical after-sales service and application consulting
Materials and Processes
Chilled cast iron
Wear-resistant material for rolls produced since 1850, manufactured by static casting.
Cast steel
Material for cast steel rolls, primarily for the steel industry.
Semi-steel
Material for semi-steel rolls combining the properties of steel and cast materials.
Roll shell iron (highly alloyed)
Shell material processed by horizontal centrifugal casting as the shell sleeve for a wide range of applications.
Pig iron
Charge material for melting in the induction furnace.
Forged steel (moulds)
Material of the rotating moulds for the horizontal centrifugal casting process.
Wear-resistant alloy as shell material
Various alloys for the roll shell, tailored to the respective application.
Locations
Tenneck (Werfen)
ATHeadquarters, foundry and production
- Part weight / size
- Raw weight up to 60 t, finished machined up to 42 t; length
- Lot size
- Customer-specific single-part and small-batch production
- Materials
- Chilled cast iron, cast steel, semi-steel, highly alloyed roll shell iron, pig iron, forged steel
- 5 induction furnaces (capacity 3 to 24 t)
- Horizontal centrifugal casting facility for strip rolls
- Machining centre for turning/milling/drilling with two independent tools (2018)
- Fully automatic ultrasonic testing system (1997)
- Foundry dedusting system with 340,000 m³/h volume flow
- Annealing shop (heat treatment)
- Mechanical workshops
- ESW-Academy training workshop (approx. 1,000 m²)
Components
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Composite cast rolls by horizontal centrifugal casting (shell sleeve) with static casting of theCasting | – | 9 m | 60 t (raw weight) / 42 t (finished | – | Roll shell iron (highly alloyed), Core material, various alloys |
| Melting of charge materials (steel and roll scrap, pig iron, alloying elements) inCasting | – | – | 3 t – 24 t | – | Steel scrap, Roll scrap, Pig iron, Alloying elements |
| Chilled cast iron rolls by static castingCasting | – | – | – | – | Chilled cast iron |
| Cast steel and semi-steel rollsCasting | – | – | – | – | Cast steel, Semi-steel |
| Heat treatment (annealing) of rollsHeat treatment | – | – | – | – | Roll materials |
| Machining: turning, milling, grinding of rollsMachining | Dimensional accuracy checked to 1/1000 mm | 9 m × Diameter up to 1,500 mm | 42 t | – | Roll materials (cast steel, cast), Forged steel (moulds) |
| Assembly of accessory parts (rings & accessories) on rollsAssembly | – | – | – | – | – |
| Ultrasonic testing (fully automatic testing system)Testing | – | – | – | – | – |
| Metallography, melting and casting inspection, final inspectionTesting | – | – | – | – | – |
5 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| Induction furnace | – | 5 | Capacity 3 to 24 tonnes | – | Tenneck |
| Horizontal centrifugal casting facility | – | – | Strip rolls | 1971 (Inbe | Tenneck |
| Machining centre for turning/milling/drilling (simultaneous machining by two independent | – | – | – | 2018 | Tenneck |
| Fully automatic ultrasonic testing system | – | – | – | 1997 | Tenneck |
| Foundry dedusting system | – | – | Volume flow 340,000 m³/hour | 1998 | Tenneck |
Additional services
Quality
The quality of every roll is monitored by inspections accompanying production; key control points are melting, casting, metallography, heat treatment, ultrasonic testing, machining and final inspection. The dimensional accuracy of the finished rolls is checked to 1/1000 mm.
| Evidence | Tenneck (Werfen) |
|---|---|
| ISO 9001:2015 | |
| ISO 14001:2015 | |
| EcoVadis Bronze Medal |
History
- 1770
Erection of a blast furnace and hammer mill at the present site by Prince-Archbishop Sigismund Count of Schrattenbach.
- 1850
First production of chilled cast iron rolls by static casting.
- 1899
Acquisition of the Eisenwerkgesellschaft Sulzau-Werfen by the Weinberger family.
- 1960
Discontinuation of mining and shutdown of the blast furnace operation after depletion of the local ore deposits.
- 1965
Start of production of cast steel and semi-steel rolls, primarily for the steel industry.
- 1971
Commissioning of a horizontal centrifugal casting facility for strip rolls.
- 1976
Introduction of computerised numerical control (CNC) for machine tools.
- 1987
Expansion of the foundry, annealing shop and mechanical workshops (1982–1987).
- 1993
Introduction of a company-wide database for all order-related information.
- 1997
Installation of a fully automatic ultrasonic testing system, modernisation and expansion of the machine park.
- 1998
Environmental Award of Austrian Industry, construction of the foundry dedusting system (340,000 m³/h), ISO 9001 certification.
- 1999
100 years of Eisenwerk Sulzau-Werfen owned by the Weinberger family.
- 2009
Acquisition of the American specialty foundry Miller Centrifugal Casting (MCC).
- 2010
Environmental protection measures, modernisation of the machine park, expansion of melting and annealing capacity.
- 2018
Installation and commissioning of a machining centre for turning/milling/drilling with simultaneous machining by two independent tools.
- 2022
Anniversary "250+2 years" (1770) with a celebration at Salzburg Airport.
- 2024
Opening of the ESW-Academy (training workshop, approx. 1,000 m²) and 125 years owned by the Weinberger family.