Iron castings for small and medium series: spheroidal graphite iron, ADI and grey cast iron with heat treatment, machining and coating
Fürstenwalder Guss GmbH
Fürstenwalde (Spree) · GermanyNew on Amplifa
Customer Castings as a Passion
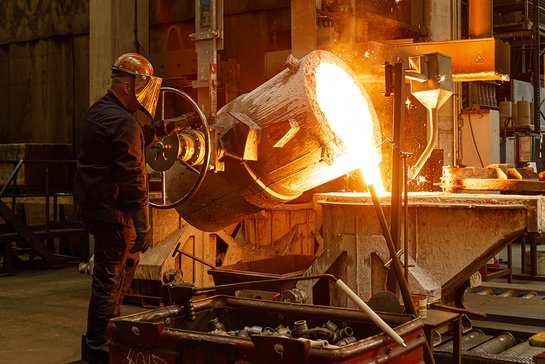
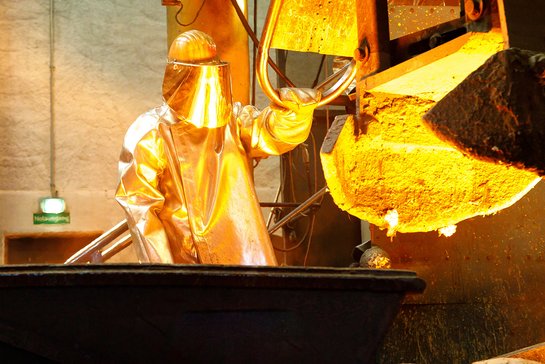
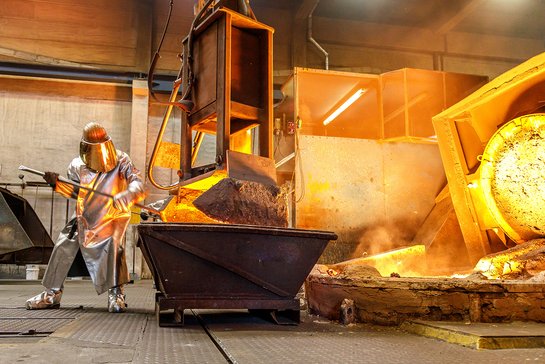
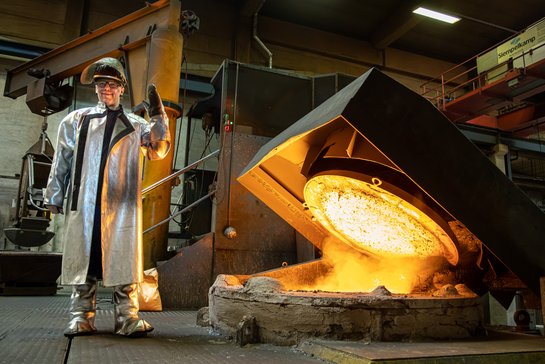
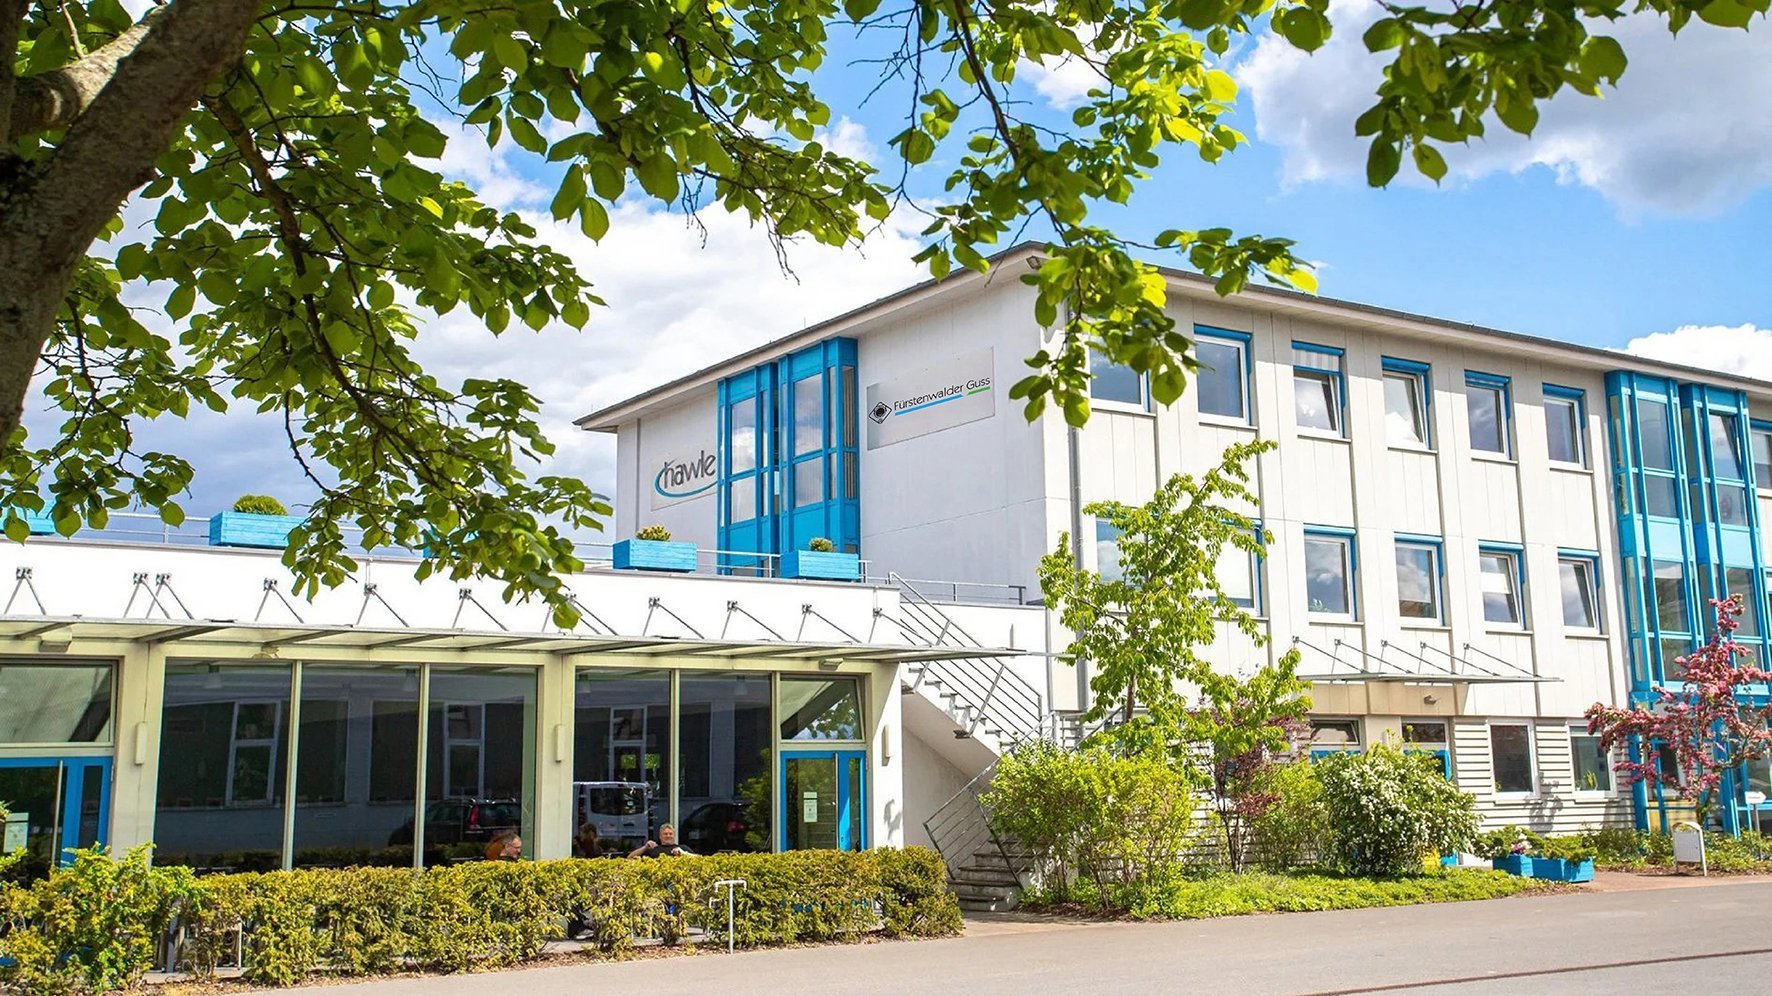
Fürstenwalder Guss is a customer-oriented foundry in Fürstenwalde (Spree) with more than 100 years of foundry tradition at the site and, for almost 30 years, part of the Hawle Group. Around 230 employees produce castings in spheroidal graphite iron (ductile iron), ausferritic ductile iron (ADI) and grey cast iron with lamellar graphite in small and medium series with component weights from 3 to 150 kg. The value chain includes melting operations in two medium-frequency induction crucible furnaces with a capacity of eight tonnes each, a cold-box core shop, machine moulding with flask sizes up to 1000 x 800 x 350/350 mm, heat treatment, machining, shot blasting as well as priming, painting and KTL coating. Customers include the valve and railway technology sectors as well as drive technology, construction machinery, conveying technology, agricultural machinery, mechanical engineering and compressor manufacturers; a major customer is the sister company Hawle Armaturen. Solidification simulation, 3D metrology and non-destructive testing safeguard quality.
- Site
- Fürstenwalde (Spree)
- Processes
- Casting production (customer castings, small and medium series), Heat treatment, Machining, Priming and painting, KTL coating, Magnetic particle testing according to DIN EN 1369, Visual inspection according to DIN EN 1370, Ultrasonic testing according to DIN EN 12680
- Materials
- Grey cast iron with lamellar graphite, Spheroidal graphite cast iron, Ausferritic spheroidal graphite cast iron (ADI), EN-GJS-350-22 (RT/LT), EN-GJS-400-15, EN-GJS-400-18 (RT/LT), EN-GJS-450-10, EN-GJS-500-7
- Certificates
- DIN EN ISO 9001:2015, DIN EN ISO 14001:2015, EMAS, Q1 Deutsche Bahn Track Components, HPQ Deutsche Bahn Permanent Way Track Components, HPQ Deutsche Bahn Wheelset Bearing Housings, Lloyd's Register, ABS - Approval of Plants and Procedures, DNV Approval, Pressure Equipment Directive, Welding Procedure Qualification, ISO 9001, ISO 14001, Deutsche Bahn Q1 Track Components, Deutsche Bahn HPQ Permanent Way Track Components, Deutsche Bahn HPQ Wheelset Bearing Housings, ABS, DNV
- Employees
- 230
- Industries
- Valves, Drive technology, Construction machinery, Conveying technology, Rail vehicles/Railway technology, Agricultural machinery
- 01
Pattern-making coordination and solidification/mould-filling simulation
- 02
Melting operations
- 03
Core shop (cold box)
- 04
Moulding
- 05
Heat treatment
- 06
Machining
- 07
Shot blasting
- 08
Priming/Painting/KTL coating
- 09
Non-destructive testing and quality inspection
- 10
Transport with in-house forwarding
Materials and Processes
Spheroidal graphite cast iron (DIN EN 1563)
Ductile iron from EN-GJS-350-22 (RT/LT) to EN-GJS-700-2 including EN-GJS-500-14 (solution-strengthened) for highly stressed components.
Ausferritic ductile iron (ADI, DIN EN 1564)
Material EN-GJS-800-10 for the highest wear and strength requirements.
Grey cast iron with lamellar graphite (DIN EN 1561)
GJL-200 and GJL-250, among others, for machine and plant components.
Cold-box core shop
Core shooting machines from 5 to 40 litres volume for complex, dimensionally accurate component areas.
Heat treatment
Additional finishing of the castings to achieve the required material properties.
KTL coating
Cathodic dip painting including priming and painting for corrosion protection.
Non-destructive testing
X-ray, ultrasonic and magnetic particle testing for material assurance.
Locations
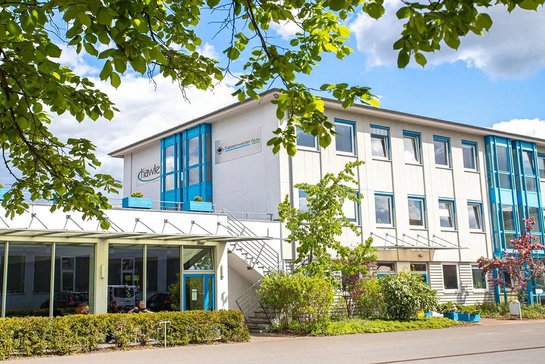
Fürstenwalde (Spree)
DEFoundry, production and administration
- Part weight / size
- 3–150 kg
- Lot size
- Small and medium series
- Materials
- Spheroidal graphite cast iron, ADI, grey cast iron with lamellar graphite
- 2x medium-frequency induction crucible furnace (8 t each)
- Cold-box core shooting machines: 2x 5 l, 1x 12 l, 2x 15 l, 1x 25 l, 1x 40 l
- Moulding lines HSP1: 650 x 500 x 250/250 mm; HSP3: 1000 x 800 x 350/350 mm
- 3D metrology
Castings
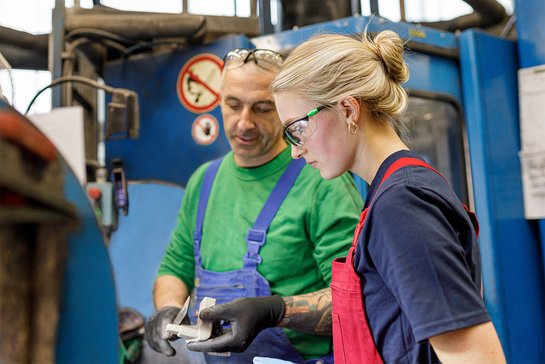
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Casting production (customer castings, small and medium series)Casting | – | HSP1: 650 x 500 x 250/250 mm; HSP3: | 3 kg – 150 kg | Small series – medium series | Grey cast iron with lamellar graphite (DIN EN 1561), Spheroidal graphite cast iron (DIN EN 1563), Ausferritic spheroidal graphite cast iron (DIN EN 1564) |
| Heat treatmentHeat treatment | – | – | – | – | – |
| MachiningMachining | – | – | – | – | – |
| Priming and paintingSurface | – | – | – | – | – |
| KTL coatingSurface | – | – | – | – | – |
| Magnetic particle testing according to DIN EN 1369Testing | – | – | – | – | – |
| Visual inspection according to DIN EN 1370Testing | – | – | – | – | – |
| Ultrasonic testing according to DIN EN 12680Testing | – | – | – | – | – |
| X-ray testing according to DIN EN 12681Testing | – | – | – | – | – |
| Materials testing (chemical and mechanical properties)Testing | – | – | – | – | – |
| 3D metrologyTesting | – | – | – | – | – |
| Shot blasting (batch-wise)Surface | – | – | – | – | – |
| Pattern making (via regional partner companies)Engineering | – | – | – | – | Plastics, Metal |
| Solidification and mould-filling simulation (design of feeding and gating systems)Engineering | – | – | – | – | – |
| Core shop (cold-box technology)Casting | – | – | – | – | – |
| Melting operations / ductile iron productionCasting | – | – | – | – | EN-GJS-350-22 (RT/LT), EN-GJS-400-15, EN-GJS-400-18 (RT/LT), EN-GJS-450-10, EN-GJS-500-7, EN-GJS-600-3, EN-GJS-700-2, EN-GJS-500-14 (solution-strengthened), EN-GJS-800-10 (ADI, DIN EN 1564), EN-GJL-200, EN-GJL-250 |
| Moulding (machine moulding for small and medium series)Casting | – | 650 x 500 x 250/250 mm (HSP1); 1000 x | 150 kg (raw weight) | – | – |
7 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| Medium-frequency induction crucible furnace | – | 2 | 8 tonnes capacity each | – | Fürstenwalde (Spree) |
| Core shooting machine (cold box) | – | 2 | 5 litre volume | – | Fürstenwalde (Spree) |
| Core shooting machine (cold box) | – | 1 | 12 litre volume | – | Fürstenwalde (Spree) |
| Core shooting machine (cold box) | – | 2 | 15 litre volume | – | Fürstenwalde (Spree) |
| Core shooting machine (cold box) | – | 1 | 25 litre volume | – | Fürstenwalde (Spree) |
| Core shooting machine (cold box) | – | 1 | 40 litre volume | – | Fürstenwalde (Spree) |
| Moulding line | Flask sizes HSP1: 650 x 500 x 250/250 mm; HSP3: 1000 x 800 x 350/350 mm | – | HSP1: 650 x 500 x 250/250 mm; HSP3: 1000 x 800 x 350/350 mm | – | Fürstenwalde (Spree) |
Additional services
Reference customers
Quality
Quality inspections extend across the entire process chain, from incoming goods inspection and monitoring of melting, treatment and moulding material parameters to 3D metrology. Non-destructive testing (magnetic particle testing DIN EN 1369, visual inspection DIN EN 1370, ultrasonic testing DIN EN 12680, X-ray testing DIN EN 12681) and consistent documentation ensure traceability.
| Evidence | Fürstenwalde (Spree) |
|---|---|
| ISO 9001 | |
| ISO 14001 | |
| EMAS | |
| Deutsche Bahn Q1 Track Components | |
| Deutsche Bahn HPQ Permanent Way Track Components | |
| Deutsche Bahn HPQ Wheelset Bearing Housings | |
| Lloyd's Register | |
| ABS | |
| DNV | |
| Pressure Equipment Directive |
History
- ca. 1920
The Fürstenwalde site looks back on more than 100 years of foundry tradition.
- 1995
EMAS certification of the company.
Part of the Hawle Group for almost 30 years; casting production for the sister company Hawle Armaturen complements external customers.