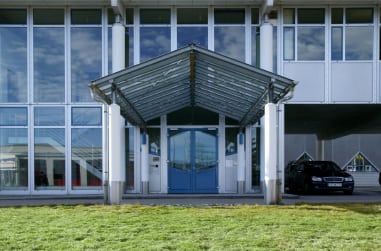
Manufacturing of ground precision turned parts made of steel: sliding-headstock turning, centerless grinding, superfinishing and induction hardening in series production
Güntert Präzisionstechnik GmbH
78052 Villingen-Schwenningen, Max-Planck-Str. 17New on Amplifa
Traditional family business since 1946
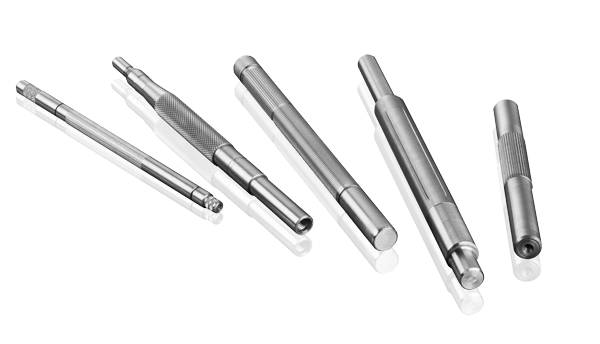
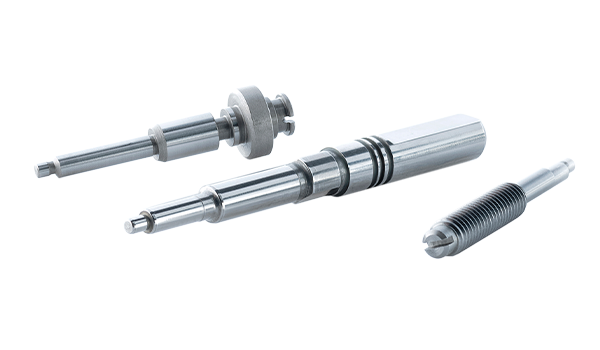
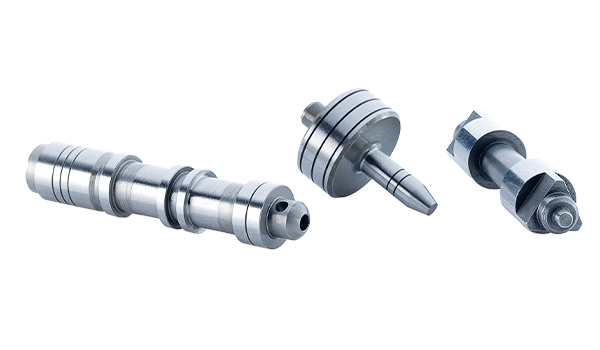
Güntert Präzisionstechnik GmbH is an owner-managed family business in Villingen-Schwenningen in the Black Forest that has been manufacturing precision parts since 1946. The focus is on ground, rotationally symmetric turned parts made of steel: The company machines the blanks by sliding-headstock, rear-spindle and hard turning and adds a wide range of grinding processes in-house, including centerless plunge and through-feed grinding as well as grinding between centers. In addition, honing, superfinishing and ball finishing, knurling and thread rolling as well as induction hardening for large-scale production are carried out; further heat treatment processes are handled with partners. On more than 6,380 m² of production space, among other things, more than 30 CNC sliding-headstock lathes (workpieces 4–30 mm diameter, up to 560 mm length) and a linked production line for long shafts with turning, hardening, straightening and grinding machines are in operation; annual capacity is around 1,900 t of steel and approx. 50 million round-ground turned parts. Customers are primarily the automotive industry including Tier-1 suppliers, mechanical engineering, the sensor and hydraulics industry, plant engineering as well as manufacturers of electric motors, with products ranging from hydraulic pistons and injection technology components to electric motor shafts.
- Site
- Villingen-Schwenningen
- Processes
- Sliding-headstock turning, Rear-spindle turning, Hard turning, Centerless plunge grinding, Centerless through-feed grinding, Grinding between centers, Special grinding processes, Grinding of shoulders, faces, control edges and concentric shoulders
- Materials
- Steel, Sliding-headstock turning, Hard turning, Centerless grinding (plunge and through-feed), Grinding between centers, Superfinishing and ball finishing, Induction hardening and tempering, Optical and tactile metrology
- Certificates
- ISO 9001:2015, ISO 50001:2018, ISO 14001:2015, IATF 16949:2016
- Founded
- 1946
- Industries
- Automotive (cars/trucks, Tier-1), Mechanical engineering, New Mobility / e-mobility, Sensor technology, Hydraulics, Plant engineering
- 01
Consulting and design for manufacturability
- 02
Prototype production and initial sample inspection report
- 03
Turning (sliding-headstock, rear-spindle, hard turning)
- 04
Induction hardening / heat treatment
- 05
Grinding (centerless plunge, through-feed, between centers)
- 06
Honing, superfinishing and ball finishing
- 07
Cleaning
- 08
Metrology and 100% inspection
- 09
Packaging according to customer specifications
- 10
Delivery
Materials and Manufacturing Processes
Steel
Raw material for all turned parts; up to 820 t of bar steel available in the company's own high-bay warehouse.
Sliding-headstock turning
More than 30 CNC sliding-headstock lathes produce workpieces from 4–30 mm diameter and up to 560 mm length.
Hard turning
Hard machining of hardened parts, since 2021 with an automated hard turning machine from DMG Mori.
Centerless grinding (plunge and through-feed)
Cylindrical grinding with diameter tolerances below 3 µm, roundness below 0.5 µm and roughness Rz <0.5.
Grinding between centers
Precision cylindrical grinding of longer parts with the same tolerances as in centerless grinding.
Superfinishing and ball finishing
Short-stroke cylindrical honing and shoulder/face finishing for roundness below 0.3 µm and line profiles of 2 µm.
Induction hardening and tempering
Induction hardening for large-scale production is integrated into the company's own manufacturing; further processes (e.g. case hardening, gas nitriding, bainitizing) with partners.
Optical and tactile metrology
100% inspection with eddy current, laser, air diameter and camera inspection, classification in diameter steps down to 0.5 µm.
Locations
Villingen-Schwenningen
DEHeadquarters and production
- Part weight / size
- Turned parts 4–30 mm diameter, up to 560 mm length
- Lot size
- Small to large series
- Materials
- Steel
- More than 30 CNC sliding-headstock lathes
- Mikrosa Kronos S125 centerless grinding machine
- Automated hard turning machine from DMG Mori
- Linked production line for long shafts (turning, hardening, straightening, grinding)
- Mahr metrology (optical shaft measuring systems, form and position metrology, surface and contour metrology)
- Inspection systems with eddy current, laser, air diameter and camera
- High-bay warehouse for up to 820 t of bar steel
Components
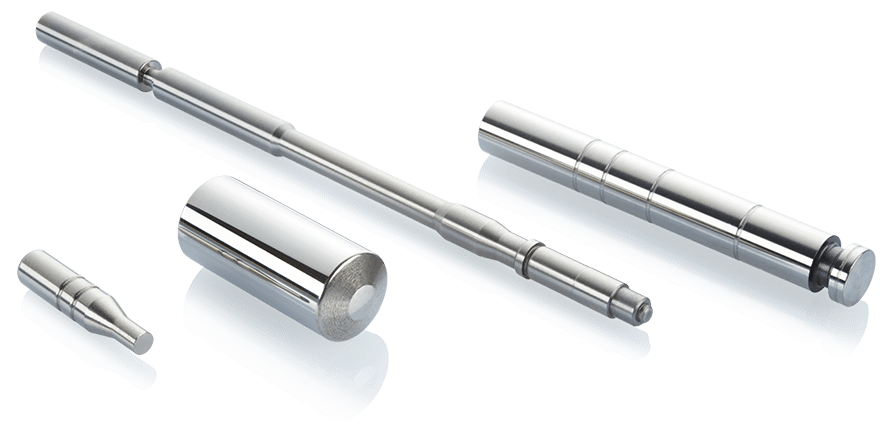
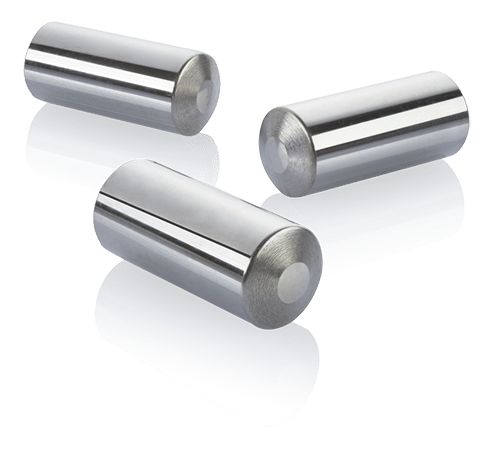
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Sliding-headstock turningMachining | – | 560 mm | – | – | Steel |
| Rear-spindle turningMachining | – | – | – | – | Steel |
| Hard turningMachining | – | – | – | – | Steel |
| Centerless plunge grindingMachining | <3 µm diameter tolerance, roundness <0.5 µm · Rz <0.5 | 400 mm (width of the grinding wheel) | – | – | Steel |
| Centerless through-feed grindingMachining | <3 µm diameter tolerance, roundness <0.5 µm · Rz <0.5 | – | – | – | Steel |
| Grinding between centersMachining | <3 µm diameter tolerance, roundness <0.5 µm · Rz <0.5 | – | – | – | Steel |
| Special grinding processesMachining | – | – | – | – | Steel |
| Grinding of shoulders, faces, control edges and concentric shouldersMachining | – | – | – | – | Steel |
| Superfinishing (short-stroke cylindrical honing, plunge and through-feed)Machining | Roundness <0.3 µm · Rz <0.3, Ra 0.02, Rmrmax (c1=0.1) >= 95% | – | – | – | Steel |
| Ball finishing (shoulder finishing and face finishing)Machining | Line profiles 2 µm · Rz 0.3 | – | – | – | Steel |
| HoningMachining | – | – | – | – | Steel |
| Cylindrical finishing by through-feed and plunge methodsMachining | – | – | – | – | Steel |
| Knurling and thread rollingForming | – | – | – | – | Steel |
| Induction hardeningHeat treatment | – | – | – | – | Steel |
| Tempering (in-house)Heat treatment | – | – | – | – | Steel |
| Case hardeningHeat treatment | – | – | – | – | Steel |
| Through hardeningHeat treatment | – | – | – | – | Steel |
| BainitizingHeat treatment | – | – | – | – | Steel |
| Vacuum hardeningHeat treatment | – | – | – | – | Steel |
| Protective gas hardeningHeat treatment | – | – | – | – | Steel |
| Gas nitridingHeat treatment | – | – | – | – | Steel |
| Gas nitrocarburizingHeat treatment | – | – | – | – | Steel |
| Deep-freezing (cryogenic treatment)Heat treatment | – | – | – | – | Steel |
| Further heat treatment processesHeat treatment | – | – | – | – | Steel |
| Drilling and milling (integrated in sliding-headstock turning)Machining | – | – | – | – | Steel |
| Straightening (linked production line for long shafts)Forming | – | – | – | – | Steel |
| Optical and tactile metrology (100% inspection, eddy current, laser, air diameter,Testing | Classification in diameter steps down to 0.5 µm | – | – | – | Steel |
| Assembly processes (integrated in measuring machines)Assembly | – | – | – | – | – |
| Cleaning of products after manufacturingSurface | – | – | – | – | Steel |
7 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| Sliding-headstock lathe (CNC) | – | über 30 | Workpieces 4–30 mm diameter, up to 560 mm length; 4–13 CNC axes | – | Villingen-Schwenningen |
| Centerless grinding machine | Mikrosa Kronos S125 | 1 | – | 2020 | Villingen-Schwenningen |
| Hard turning machine (automated) | DMG Mori | 1 | – | 2021 | Villingen-Schwenningen |
| Production line for long shafts (linked turning, hardening, straightening and grinding machines) | – | – | – | 2017 | Villingen-Schwenningen |
| Grinding machine (centerless, plunge, through-feed, between centers) | – | – | – | – | Villingen-Schwenningen |
| Optical shaft measuring systems, form and position metrology, surface and contour metrology | Mahr | – | – | – | Villingen-Schwenningen |
| Measuring machines (inductive length measuring systems, laser, air diameter inspection, camera | – | – | – | – | Villingen-Schwenningen |
Additional services
Quality and Certifications
A continuous quality management system according to ISO 9001, ISO 14001, ISO 50001 and IATF 16949 accompanies the entire process chain from design alignment to manufacturing according to the zero-defect philosophy. The measuring lines include optical shaft measuring systems as well as eddy current, laser, air diameter and camera inspection, with which products are cleaned, thoroughly inspected and packaged according to customer specifications.
| Evidence | Villingen-Schwenningen |
|---|---|
| ISO 9001:2015 | |
| ISO 14001:2015 | |
| ISO 50001:2018 | |
| IATF 16949:2016 |
Company History Milestones
- 1946
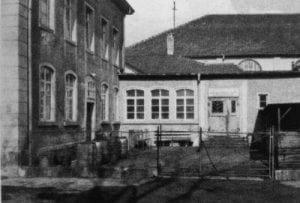
Founding of “Schwanog Schwarzwälder Normteile GmbH, Fabrik für Feinmechanik” by Oscar Güntert; premises at Bertholdstraße 8 in Villingen.
- 1954
Siegfried Güntert joins the company.
- 1960
Move to the new factory hall on Berliner Straße in Villingen; approx. 25 employees.
- 1987
Renaming to Güntert Präzisionstechnik GmbH.
- 1989
Move to Max-Planck-Str. 17 with 4,300 m² of production space; 75 employees.
- 1999
Construction of an additional hall for grinding plastic parts; Georg Güntert becomes managing director alongside his father.
- 2003
Expansion of manufacturing by 1,000 m².
- 2009
Construction of a high-bay warehouse for up to 820 t of bar steel.
- 2014
Expansion of manufacturing by 1,080 m².
- 2017
Set-up of a production line for long shafts with linked turning, hardening, straightening and grinding machines.
- 2020
Expansion of centerless plunge grinding with a Mikrosa Kronos S125.
- 2021
New automated hard turning machine from DMG Mori.