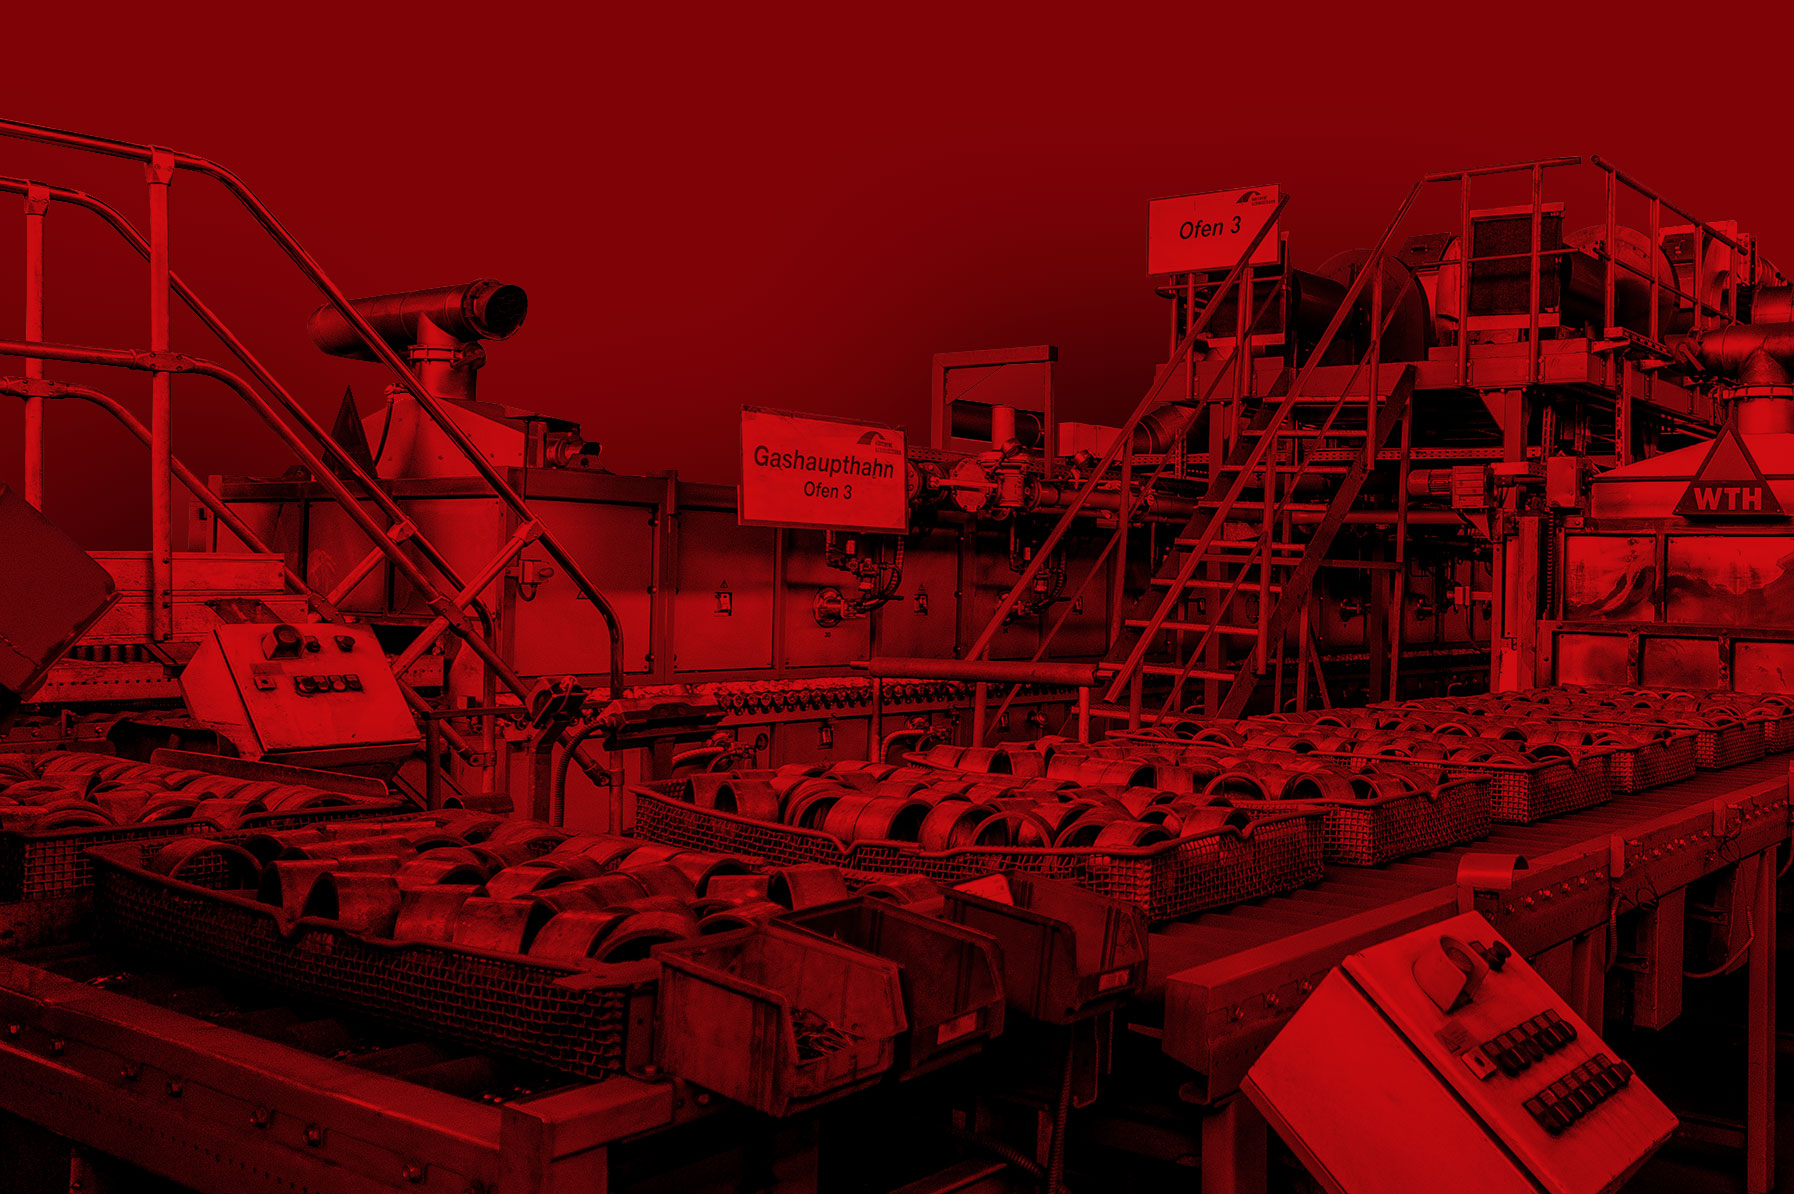
Heat treatment of metallic materials – hardening, tempering, annealing under and without protective gas up to 5,000 kg piece weight.
Härterei Schmidthaus GmbH
BreckerfeldNew on Amplifa
About Härterei Schmidthaus
Härterei Schmidthaus GmbH is a contract manufacturer specializing in the heat treatment of metallic materials, based in Breckerfeld. The service portfolio comprises hardening, tempering, normalizing, annealing (tempering), soft annealing, stress-relief annealing, ferritization, carbide decomposition annealing and isothermal annealing (FP) – in each case with and without protective gas atmosphere. In multipurpose chamber furnaces (furnace size 1050×3500 mm) workpieces up to 5,000 kg piece weight are treated; series-produced small parts up to 20 kg are processed on roller-hearth continuous furnaces. Quenching is performed up to 1150 °C in oil, polymer or water; on two centrifugal shot-blasting machines components are subsequently blasted and descaled. Customers come from automotive, marine/shipbuilding as well as pressure equipment and plant engineering, evidenced by IATF 16949, ABS approval as well as AD 2000 W0 and EC 2014/68/EU. An in-house testing laboratory with hardness testing, metallography, tensile, impact, crack and microhardness testing issues 3.1 inspection certificates. The company, founded in 1939 in Remscheid-Lennep, is today run by the third generation of the Schmidthaus family.
- Site
- Breckerfeld
- Processes
- Hardening under protective gas (multipurpose chamber furnace), Hardening under protective gas (continuous furnace), Tempering under protective gas, Normalizing under protective gas, Quenching under protective gas up to 1150 °C, Carbide decomposition annealing under protective gas, Soft annealing under protective gas, Ferritization under protective gas
- Materials
- metallic materials, Steel, unalloyed steels, castings, Heat treatment under protective gas, Heat treatment without protective gas, Steel (unalloyed and alloyed), Castings
- Certificates
- DIN EN ISO 9001:2015, DIN EN ISO 14001:2015, DIN EN ISO 50001:2018, IATF 16949:2016, ABS Approval (Heat Treatment Facility and Process Approval), DNV GL Approval, BV Mode II Approval, AD 2000 Data Sheet W0, EC 2014/68/EU, ABS approval (HT-T2452755), DNV GL / BV Mode II, AD 2000 W0 / EC 2014/68/EU
- Founded
- 1939
- Industries
- Automotive, Marine/Shipbuilding, Pressure equipment/Plant engineering, Automotive (IATF 16949), Marine/Shipbuilding (ABS approval), Pressure equipment/Plant engineering (AD 2000 W0, EC 2014/68/EU)
- 01
Order acceptance and consultation on materials and processes
- 02
Heat treatment (with/without protective gas) in chamber, pusher and
- 03
Quenching in oil, polymer or water
- 04
Sandblasting/descaling on centrifugal shot-blasting machines
- 05
Testing in the in-house laboratory (hardness, metallography, tensile, impact,
- 06
Issuance of 3.1 inspection certificate and shipping
Materials & Heat Treatment Processes
Heat treatment under protective gas
Hardening, tempering, normalizing and more in multipurpose chamber furnaces and a protective-gas-operated roller-hearth continuous furnace for distortion reduction.
Heat treatment without protective gas
Treatments in chamber furnaces, belt/continuous furnaces and pusher furnaces with various quenching media.
Steel (unalloyed and alloyed)
Main material for hardening, tempering and annealing processes with an optimized combination of strength and toughness.
Castings
Semi- and fully automatic testing of large castings alongside small turned parts in the in-house laboratory.
Quenching in oil, polymer or water
Various quenching media for specific requirements on microstructure and component properties up to 1150 °C.
Locations
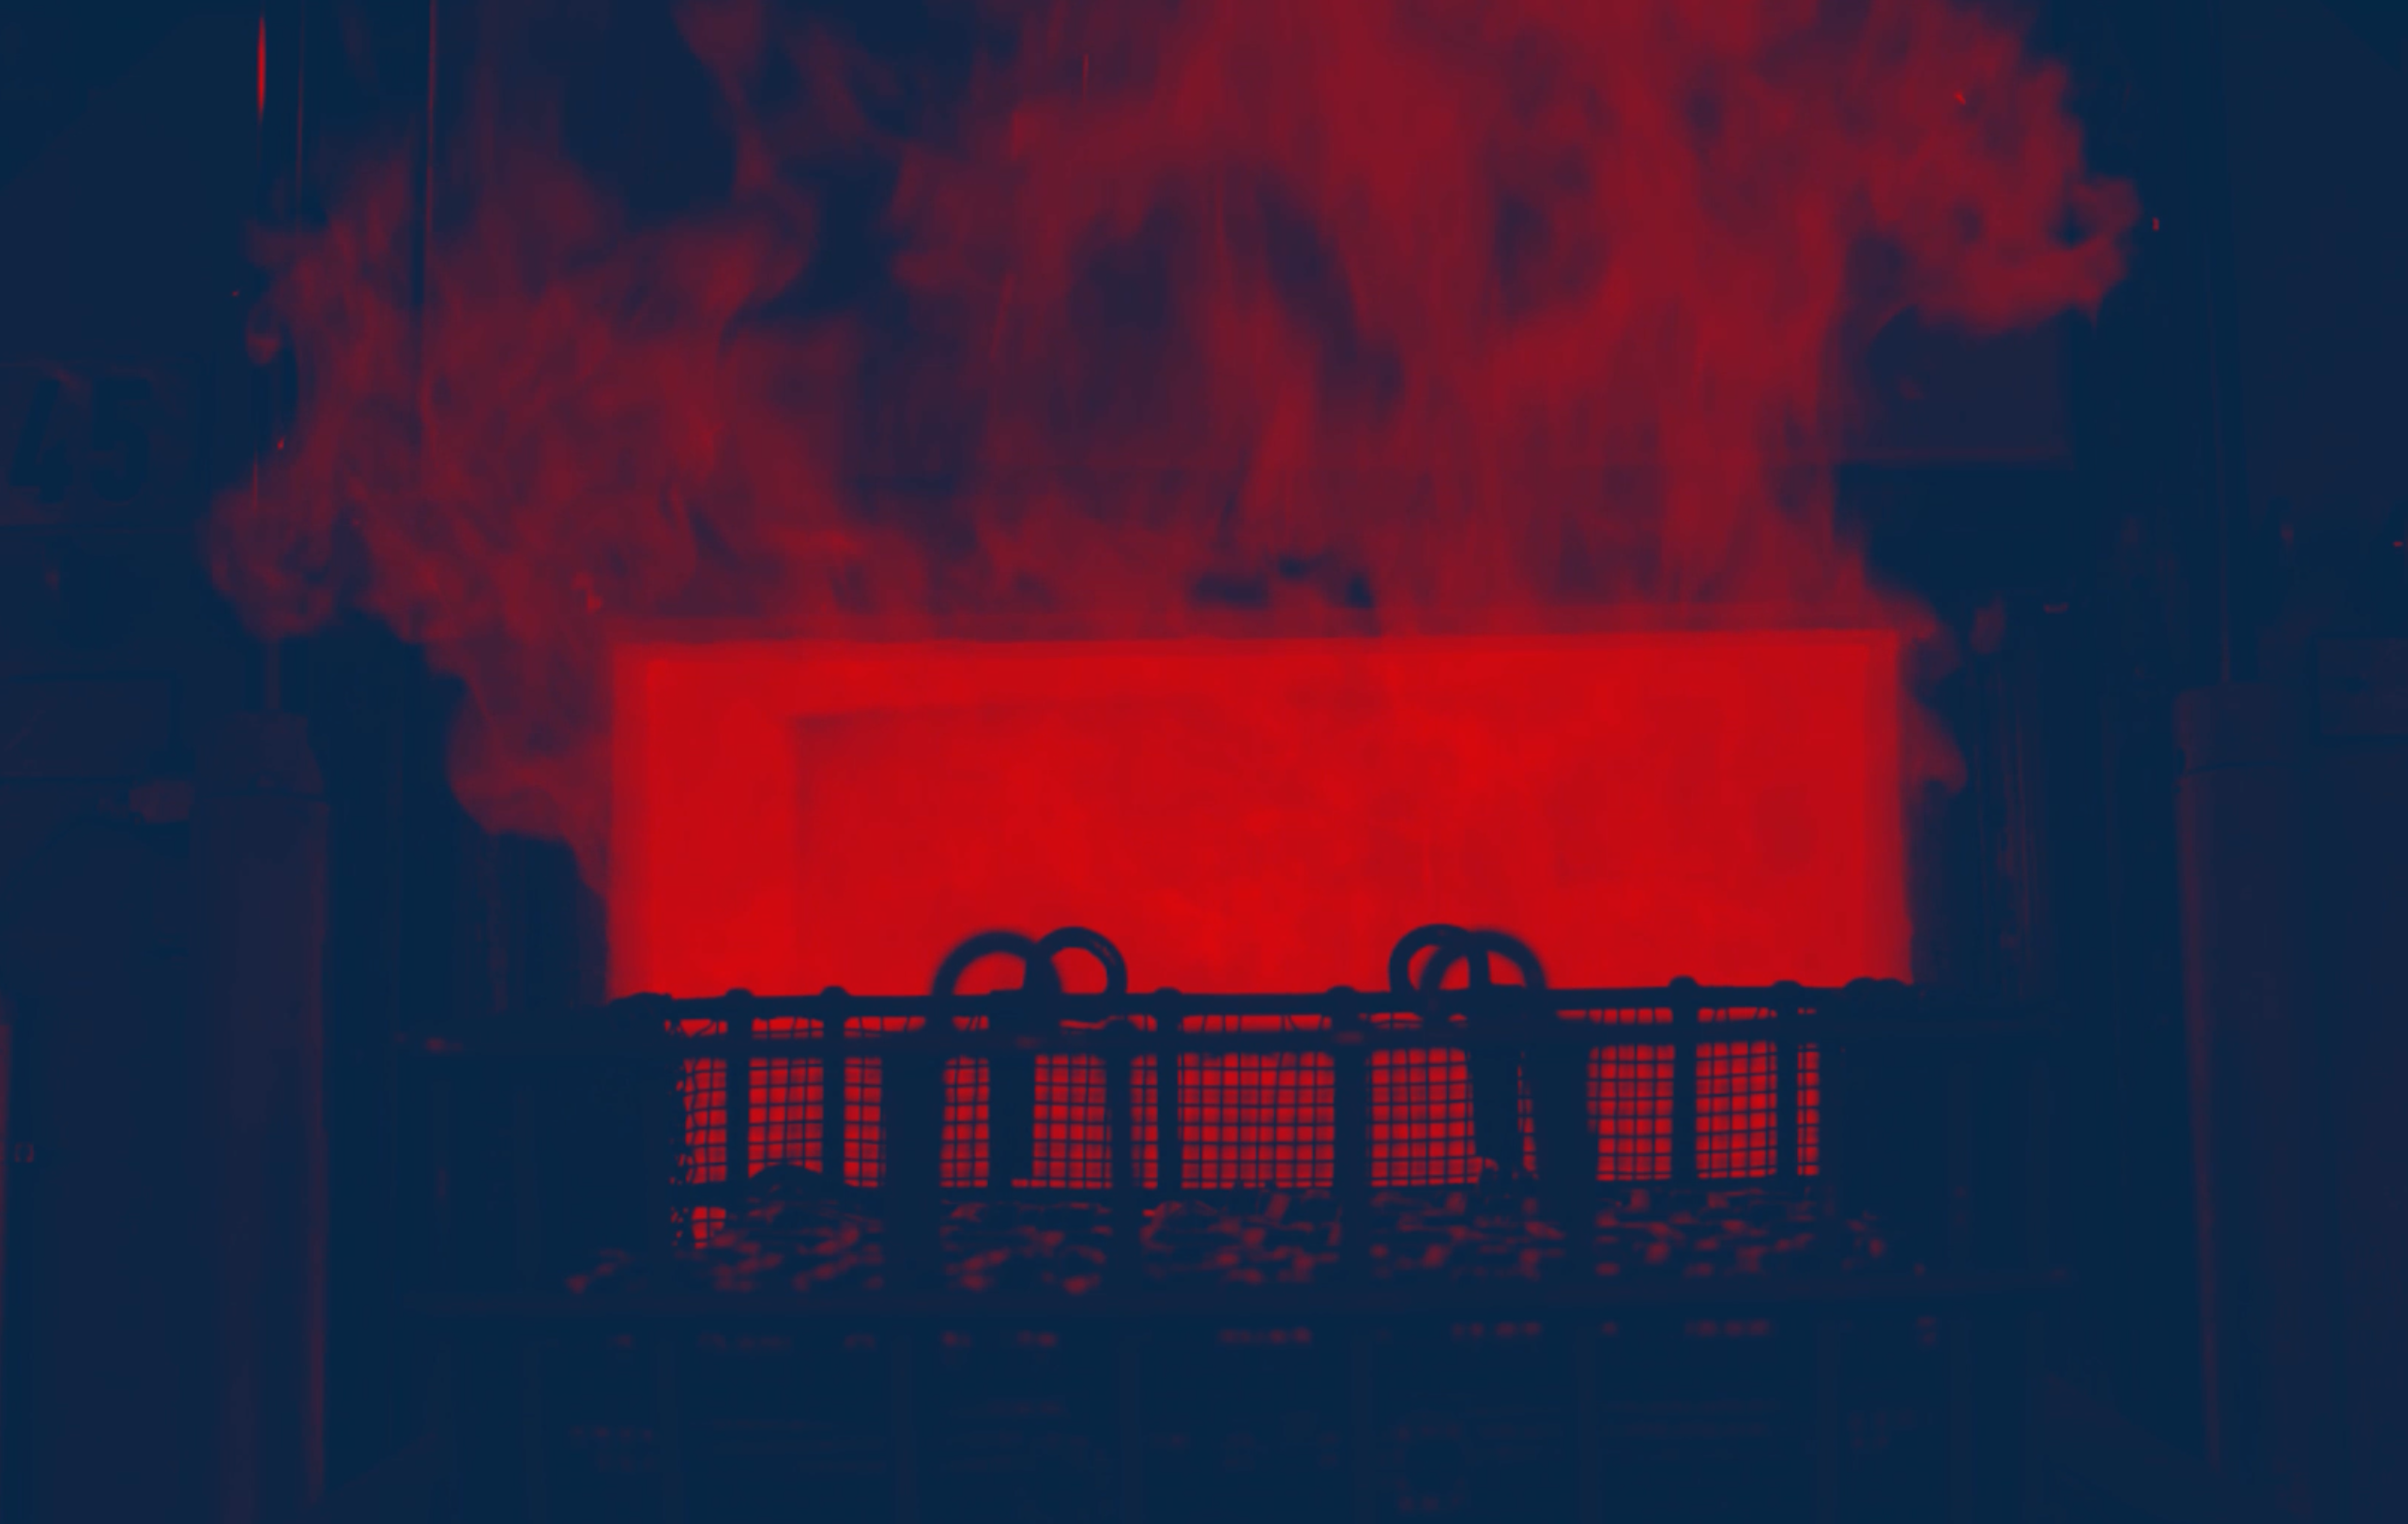
Breckerfeld
DEHeadquarters, Plant I and Plant II with training center (heat treatment and testing laboratory)
- Part weight / size
- Chamber furnaces up to 5,000 kg (furnace size 1050×3500 mm)
- Lot size
- Series batches and small batch weights
- Materials
- Steel, castings, metallic materials
- Multipurpose chamber furnaces (1050×3500 mm)
- Roller-hearth continuous furnaces for annealing and tempering (2 fully automatic systems, 2010)
- Protective-gas-operated roller-hearth continuous furnace (2002)
- Pusher furnaces
- 2 centrifugal shot-blasting machines
- Light-load hardness testing machine
- Pendulum impact tester PW 30
- Tensile testing machine up to 40 t
Treated Components
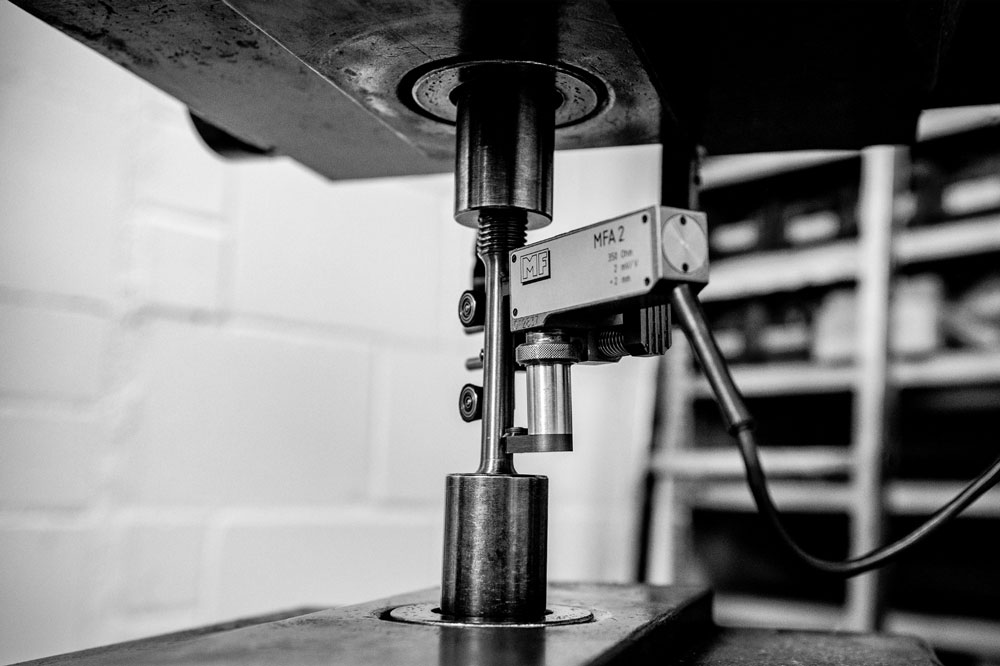
Inside the production
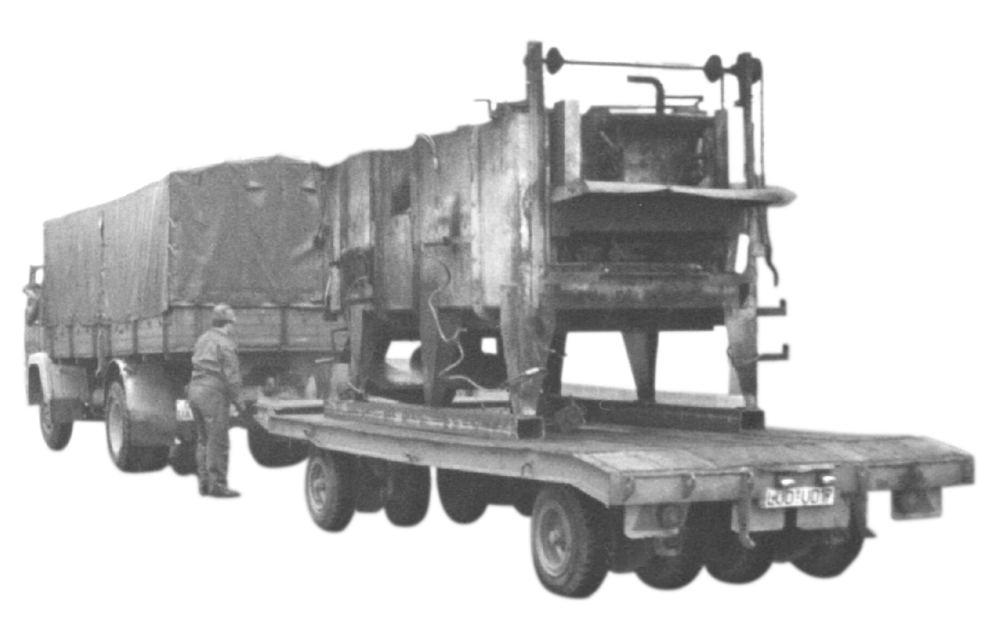
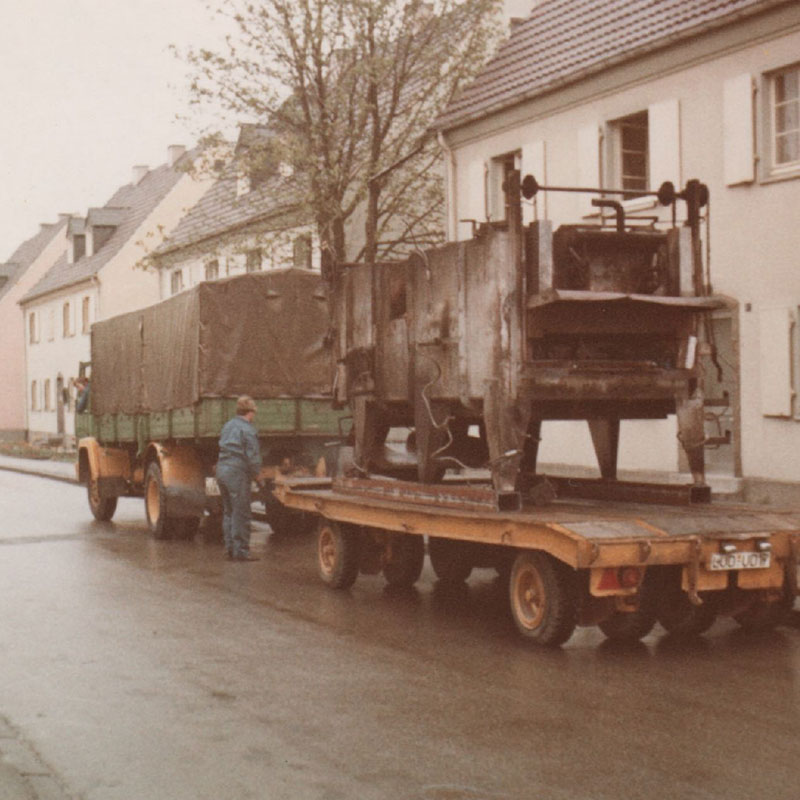
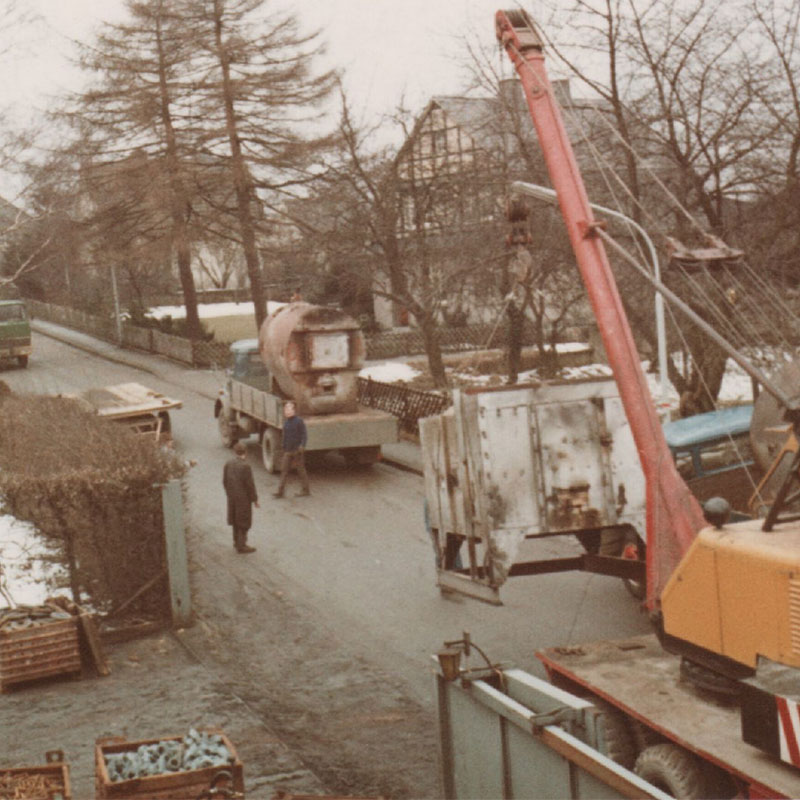
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Hardening under protective gas (multipurpose chamber furnace)Heat treatment | – | 3500 mm (furnace size 1050×3500) × 1050 mm | 5000 kg | – | Steel, metallic materials |
| Hardening under protective gas (continuous furnace)Heat treatment | – | – | 20 kg | – | Steel |
| Tempering under protective gasHeat treatment | – | – | 5000 kg (chamber furnace) / 20 kg | – | Steel |
| Normalizing under protective gasHeat treatment | – | 3500 mm (furnace size 1050×3500) × 1050 mm | 5000 kg (chamber furnace) / 20 kg | – | unalloyed steels, Steel |
| Quenching under protective gas up to 1150 °CHeat treatment | – | 1850 mm (furnace size 1050×1850) × 1050 mm | 3000 kg | – | Steel |
| Carbide decomposition annealing under protective gasHeat treatment | – | 3500 mm (furnace size 1050×3500) × 1050 mm | 5000 kg | – | Steel |
| Soft annealing under protective gasHeat treatment | – | 3500 mm (furnace size 1050×3500) × 1050 mm | 5000 kg | – | Steel |
| Ferritization under protective gasHeat treatment | – | 3500 mm (furnace size 1050×3500) × 1050 mm | 5000 kg | – | Steel |
| Isothermal annealing (FP) under protective gasHeat treatment | – | 3500 mm (furnace size 1050×3500) × 1050 mm | 5000 kg (chamber furnace) / 20 kg | – | Steel |
| Stress-relief annealing under protective gasHeat treatment | – | 3500 mm (furnace size 1050×3500) × 1050 mm | 5000 kg | – | Steel |
| Annealing (tempering) under protective gasHeat treatment | – | 3500 mm (furnace size 1050×3500) × 1050 mm | 5000 kg | – | Steel |
| Hardening without protective gas (chamber furnace)Heat treatment | – | 3500 mm (furnace size 1050×3500) × 1050 mm | 5000 kg | – | Steel |
| Tempering without protective gasHeat treatment | – | – | 5000 kg | – | Steel |
| Normalizing without protective gasHeat treatment | – | 3500 mm (furnace size 1050×3500) × 1050 mm | 5000 kg | – | Steel |
| Quenching without protective gas up to 1159 °CHeat treatment | – | 1850 mm (furnace size 1050×1850) × 1050 mm | 3000 kg | – | Steel |
| Carbide decomposition annealing without protective gasHeat treatment | – | 3500 mm (furnace size 1050×3500) × 1050 mm | 5000 kg | – | Steel |
| Soft annealing without protective gasHeat treatment | – | 3500 mm (furnace size 1050×3500) × 1050 mm | 5000 kg | – | Steel |
| Ferritization without protective gasHeat treatment | – | 3500 mm (furnace size 1050×3500) × 1050 mm | 5000 kg | – | Steel |
| Isothermal annealing without protective gasHeat treatment | – | 3500 mm (furnace size 1050×3500) × 1050 mm | 5000 kg (chamber furnace) / 20 kg | – | Steel |
| Stress-relief annealing without protective gasHeat treatment | – | 3500 mm (furnace size 1050×3500) × 1050 mm | 5000 kg | – | Steel |
| Annealing (tempering) without protective gasHeat treatment | – | 3500 mm (furnace size 1050×3500) × 1050 mm | 5000 kg | – | Steel |
| Sandblasting / descaling (centrifugal shot-blasting machines)Surface | – | – | – | – | metallic materials |
| Quenching in oil, polymer or waterHeat treatment | – | – | – | – | Steel |
| Hardness testing / case hardening depth (light-load hardness testing machine)Testing | – | – | – | – | Steel, castings |
| Metallography (micrograph images)Testing | – | – | – | – | metallic materials |
| Tensile test (tensile testing machine up to 40 tonnes)Testing | – | – | – | – | metallic materials |
| Impact test (pendulum impact tester PW 30)Testing | – | – | – | – | metallic materials |
| Crack and microhardness testingTesting | – | – | – | – | metallic materials |
11 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| Multipurpose chamber furnace | – | – | Furnace size 1050×3500 mm, up to 5000 kg piece weight | – | Breckerfeld |
| Continuous furnace (roller hearth) | – | – | up to 20 kg piece weight | 2002 | Breckerfeld |
| Roller-hearth system for annealing and tempering | – | – | – | 2002 | Breckerfeld |
| Protective-gas-operated roller-hearth continuous furnace | – | – | – | 2002 | Breckerfeld |
| Continuous furnace for annealing and tempering | – | – | – | 2004 | Breckerfeld |
| Fully automatic continuous furnaces for annealing and tempering | – | 2 | up to 20 kg piece weight | 2010 | Breckerfeld |
| Pusher furnace | – | – | – | – | Breckerfeld |
| Centrifugal shot-blasting machine | – | 2 | – | – | Breckerfeld |
| Light-load hardness testing machine (automatic) | – | 1 | – | – | Breckerfeld |
| Pendulum impact tester | PW 30 | 1 | – | – | Breckerfeld |
| Tensile testing machine | – | 1 | up to 40 tonnes | – | Breckerfeld |
Additional services
Quality & Certification
An in-house laboratory covers all common testing methods: automatic light-load hardness testing machine for case hardening depth, metallography with electronically archived micrograph images, tensile testing machine up to 40 tonnes as well as pendulum impact tester PW 30 for impact tests. At the end of testing, a 3.1 inspection certificate is issued.
| Evidence | Breckerfeld |
|---|---|
| DIN EN ISO 9001:2015 | |
| IATF 16949:2016 | |
| DIN EN ISO 14001:2015 | |
| DIN EN ISO 50001:2018 | |
| ABS approval (HT-T2452755) | |
| DNV GL / BV Mode II | |
| AD 2000 W0 / EC 2014/68/EU |
Company History
- 1939
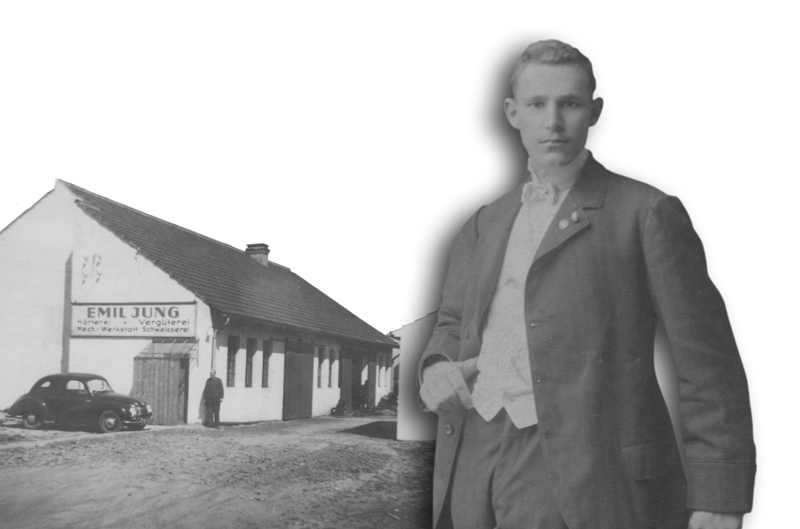
Founding of Härterei C & H Turck by Emil Jung and the brothers Carl and Heinrich Turck in Remscheid-Lennep (15 March).
- 1943
Separation from the Turck brothers; Emil Jung continues to run the hardening and tempering shop in Remscheid-Lennep and additionally produces in Halver.
- 1947
Expansion of the plant in Halver.
- 1952
Consolidation of the two plants on a new site in Halver.
- 1964
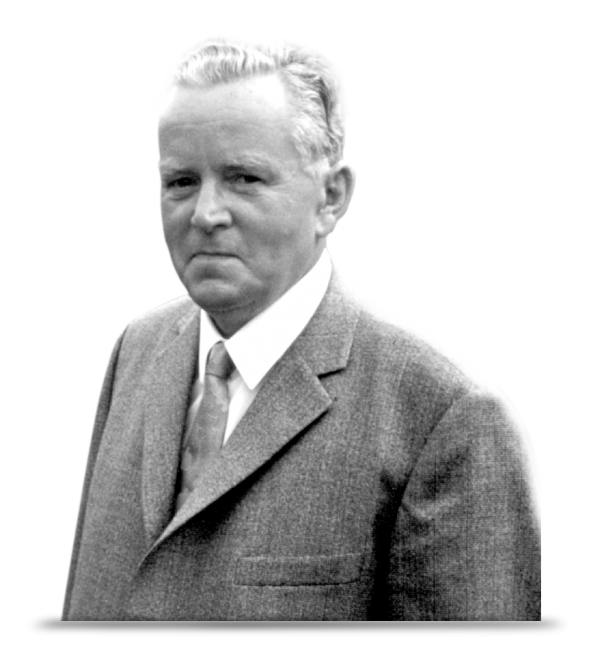
Emil Schmidthaus (son-in-law of Emil Jung) takes over plant management on 1 April.
- 1971
Relocation of the site to Breckerfeld; Jürgen Schmidthaus becomes a partner.
- 1976
Heat treatment in multipurpose chamber furnaces under protective gas.
- 1989
Jürgen Schmidthaus takes over the management after the death of Emil Schmidthaus.
- 2002
Introduction of ISO TS 16949 quality management system; commissioning of a roller-hearth system and a protective-gas-operated roller-hearth continuous furnace.
- 2004
Additional continuous furnace for annealing and tempering; modernization of the chamber furnaces and continuous furnaces.
- 2007
Construction of Plant II with integrated training center.
- 2010
Commissioning of two fully automatic continuous furnaces for annealing and tempering.
- 2014
75th company anniversary; introduction of the DIN EN ISO 50001 energy management system.
- 2016
Introduction of the DIN EN ISO 14001 environmental management system.
- 2017
Jürgen Schmidthaus steps down as managing director and becomes chairman of the advisory board.
- 2018
Wolf Maximilian and Felix-Leonard Schmidthaus become co-partners.
- 2021
Wolf Maximilian Schmidthaus receives sole power of attorney (procura).
- 2023
Wolf Maximilian Schmidthaus becomes managing director; Felix-Leonard Schmidthaus receives sole power of attorney (procura).