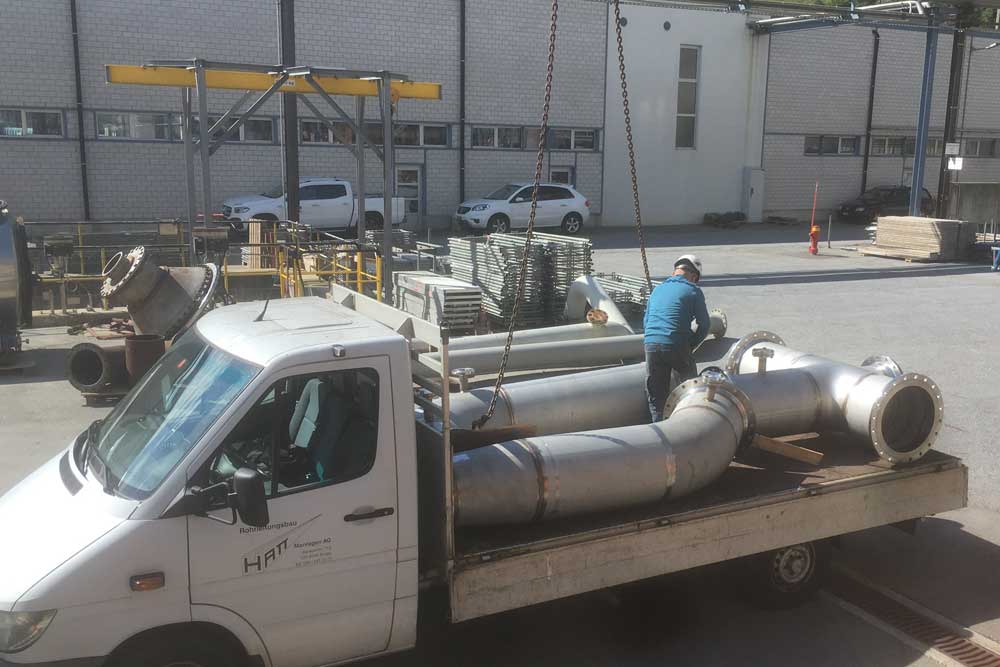
Plant construction, piping construction, welding technology and annealing service for energy and industrial companies
Hatt Montagen AG
5200 Brugg AG, SwitzerlandNew on Amplifa
About Hatt Montagen AG
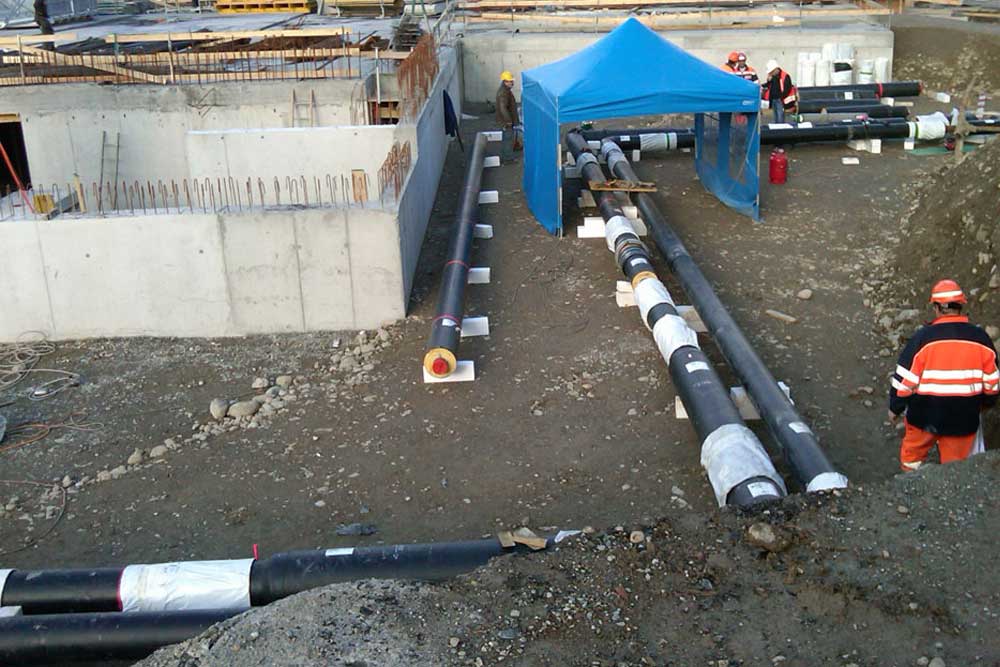
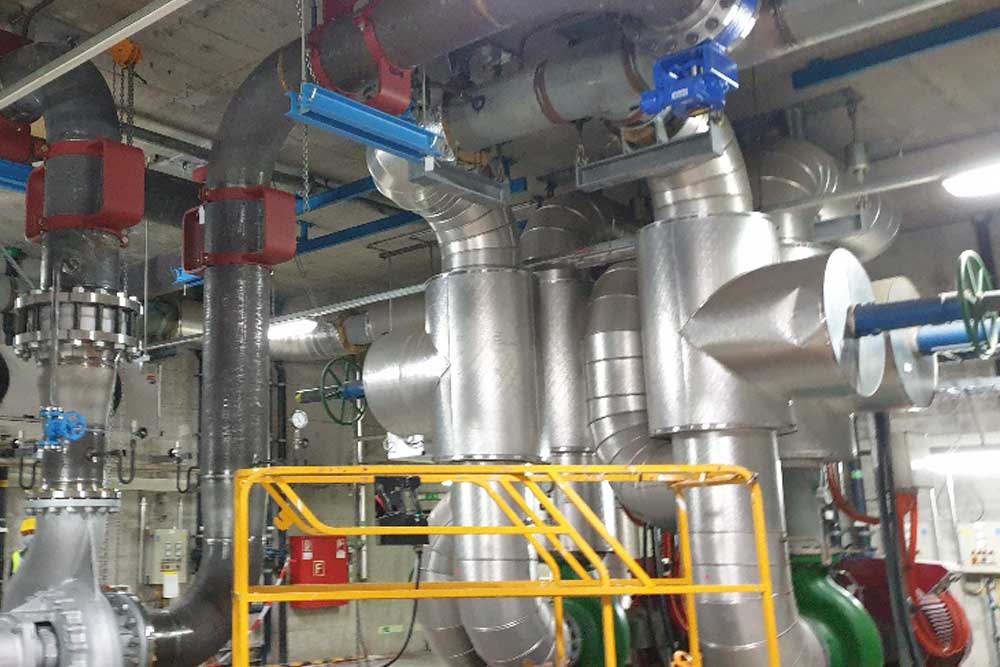
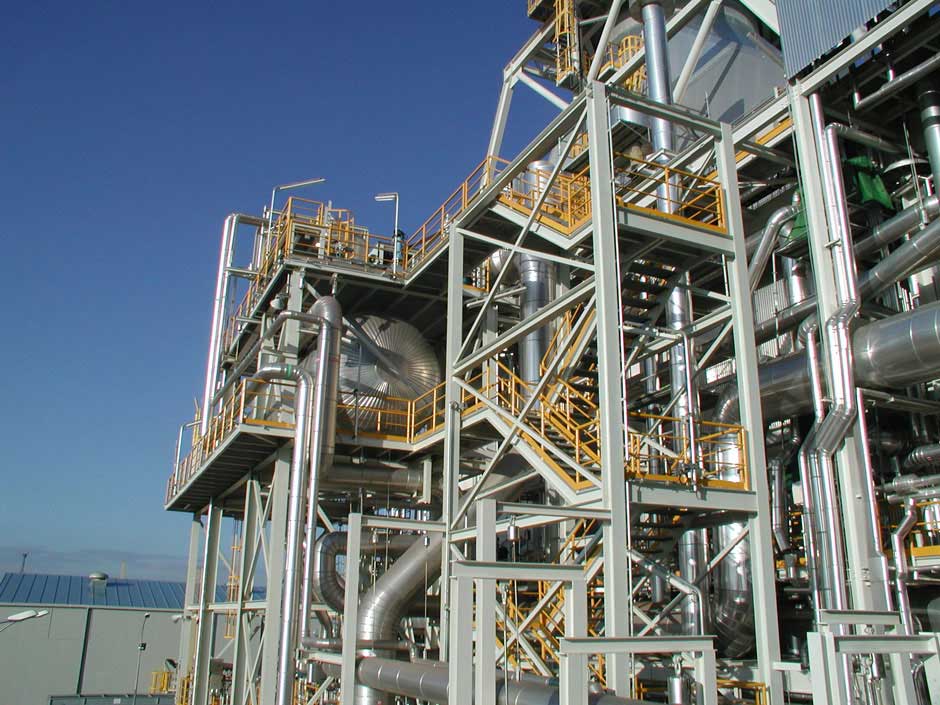
Hatt Montagen AG is a Swiss fabrication and installation company specialising in plant construction, piping construction and welding technology, headquartered in Brugg (AG). The portfolio includes prefabrication and in-house fabrication of pipework, assembly and installation including district heating pipeline construction with ancillary systems, weld overlay welding with buttering layers (e.g. NIBAS), on-site shaft machining as well as maintenance and overhaul work during shutdown periods. The company processes materials according to EN/ISO 15608, including material groups 1, 5.2 (10CrMo910), 6.4 (1.4903), 8.1 and 10.2, and, with its own annealing machine fleet, offers thermal pre-, during- and post-treatments in the workshop or at the customer's site. Non-destructive testing (VT, PT Level 2), CAD execution drawings with material take-offs and complete documentation including inspections with official authorities round off the offering. Customers come primarily from power generation (nuclear power plants, waste incineration plants, district heating), waste disposal, the food industry and the HVAC/plumbing sector; deliveries and welding assignments are carried out domestically and abroad, including packaging and freight forwarding worldwide.
- Site
- Brugg AG
- Processes
- Piping construction (prefabrication, in-house fabrication, assembly), TIG welding (141), MMA welding (111), TIG/MMA (141/111), MAG welding (135), TIG-v (141-v), Annealing service (thermal pre-, during- and post-treatment, annealing records and annealing, On-site shaft machining (pre-machining, weld overlay cladding, turning)
- Materials
- 10CrMo910, 1.4903, NIBAS filler material, Material group 10.2 (EN/ISO 15608), Unalloyed steels, Austenitic stainless steels, Material group 10.2, TIG welding
- Certificates
- ISO 9001:2015 (quality management), ISO 14001:2015 (environmental management), ISO 45001:2018 (occupational health and safety), ISO 3834-2 (quality requirements for fusion welding), EXC2 according to EN 1090-2 (steel load-bearing structures), SVTI approval Directive 201 (transfer of identification marks, workshop and, SVTI approval Directive 501 (manufacture/repair of permit-required, AD 2000-HP 0 / EN 13445-4 / EN 13480-4 / EN 12952-5 / EN ISO 3834-3, PED module, BAG permit for handling ionising radiation, ISO 9001:2015, ISO 14001:2015, ISO 45001:2018, ISO 3834-2, EN 1090 (EXC2), IATF 16949, EN 9100, ISO 13485
- Founded
- 1990
- Industries
- Power generation (nuclear power, waste incineration, district heating), Waste disposal and recycling, HVAC and plumbing, Food industry, Hospitals, Water supply and wastewater
- 01
Measurement in the existing plant
- 02
Engineering and CAD execution drawings with material take-offs
- 03
Material procurement
- 04
Prefabrication / in-house fabrication (welding technology TIG, MMA, MAG, TIG-v)
- 05
Thermal pre- and post-treatment (annealing service)
- 06
Non-destructive testing (VT/PT Level 2)
- 07
Inspections with official authorities
- 08
Packaging and freight forwarding / on-site assembly
Materials and processes
10CrMo910
Creep-resistant steel for power plant components; among other applications, weld overlay welded with NIBAS buttering layers.
1.4903
Ferritic-martensitic stainless steel for pipework in power plant construction.
Unalloyed steels
Standard structural steels for piping and steel construction according to EN/ISO 15608.
Austenitic stainless steels
Stainless materials for piping construction and food/plumbing technology.
Material group 10.2
Microstructure-stable materials for high-temperature applications according to welding approval.
NIBAS filler material
Nickel-based weld overlay as a buttering layer on 1.4903 and 10CrMo910.
TIG welding
Manual process for material groups 1 to 10.2 according to EN/ISO 15614-1 / ASME XI.
MMA (stick electrode) welding
Manual shielded metal arc welding for steels and stainless steels.
MAG welding
Partially mechanised process for steel pipework.
TIG-v welding
Process for root/orbital seams in piping construction.
Annealing service
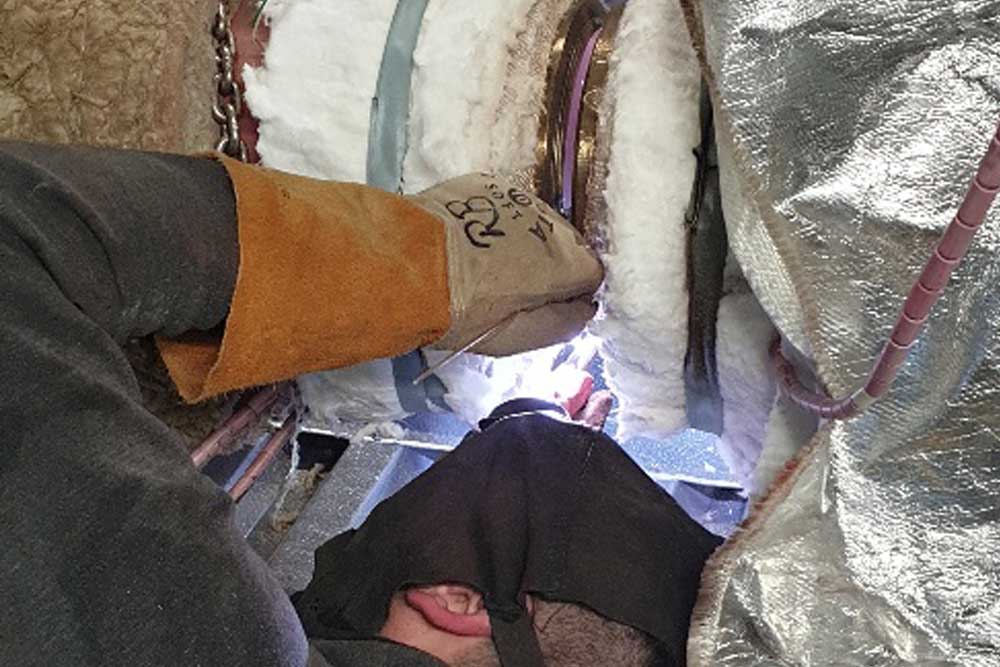
Thermal pre-, during- and post-treatment in the workshop or on site including annealing records.
Non-destructive testing
Visual testing and dye penetrant testing Level 2 (SGZP-certified) on site or in the workshop.
Locations
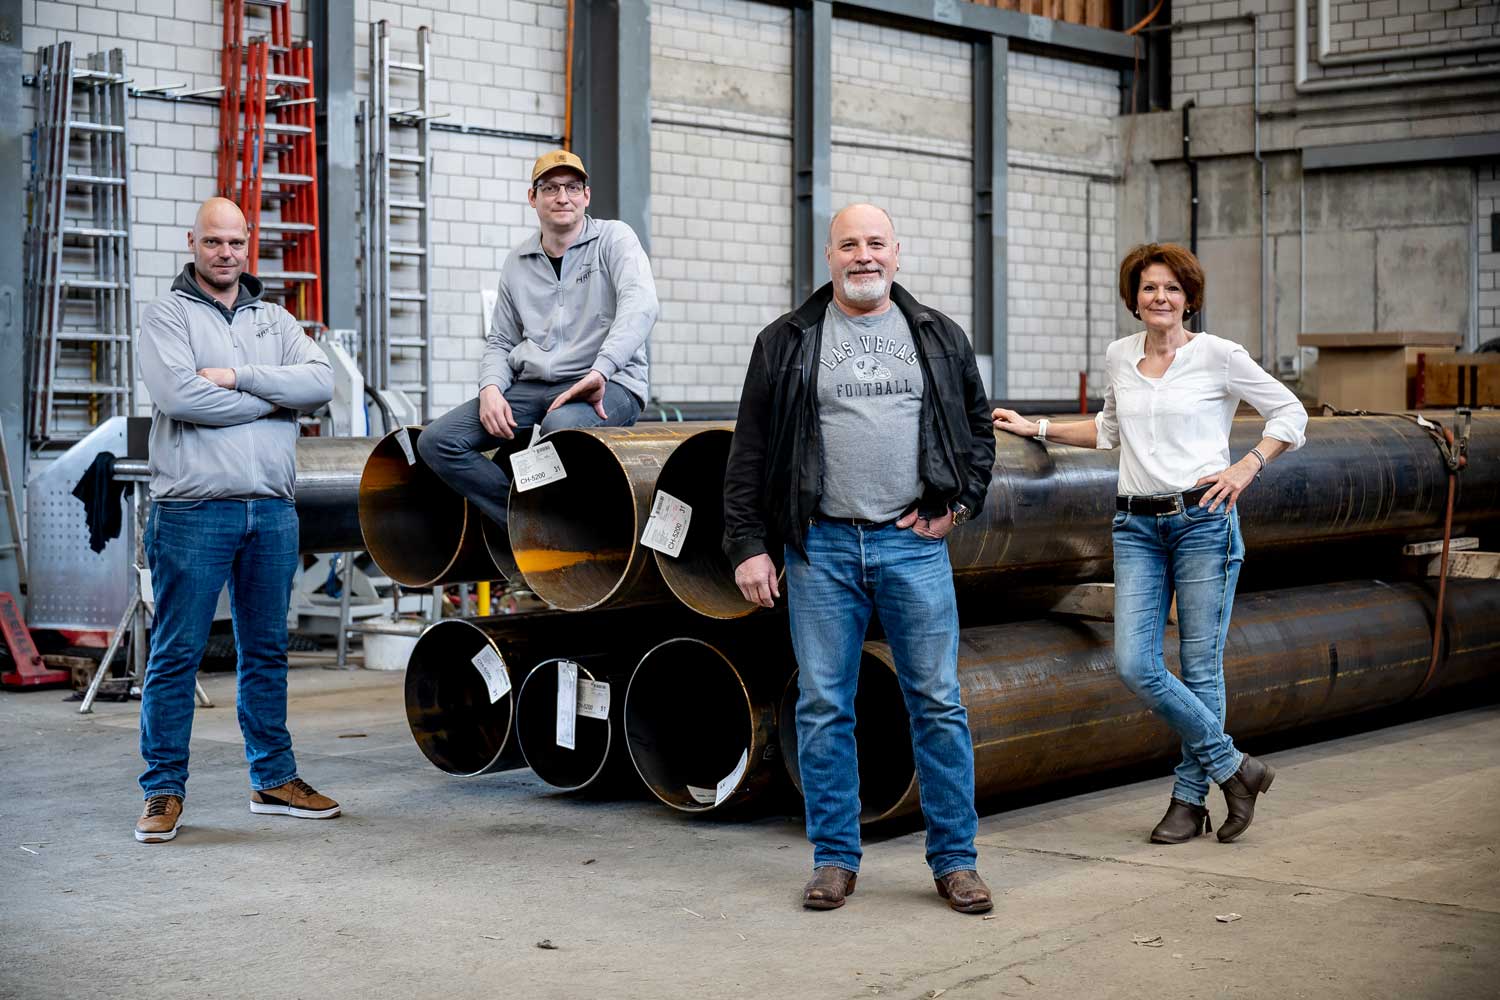
Brugg
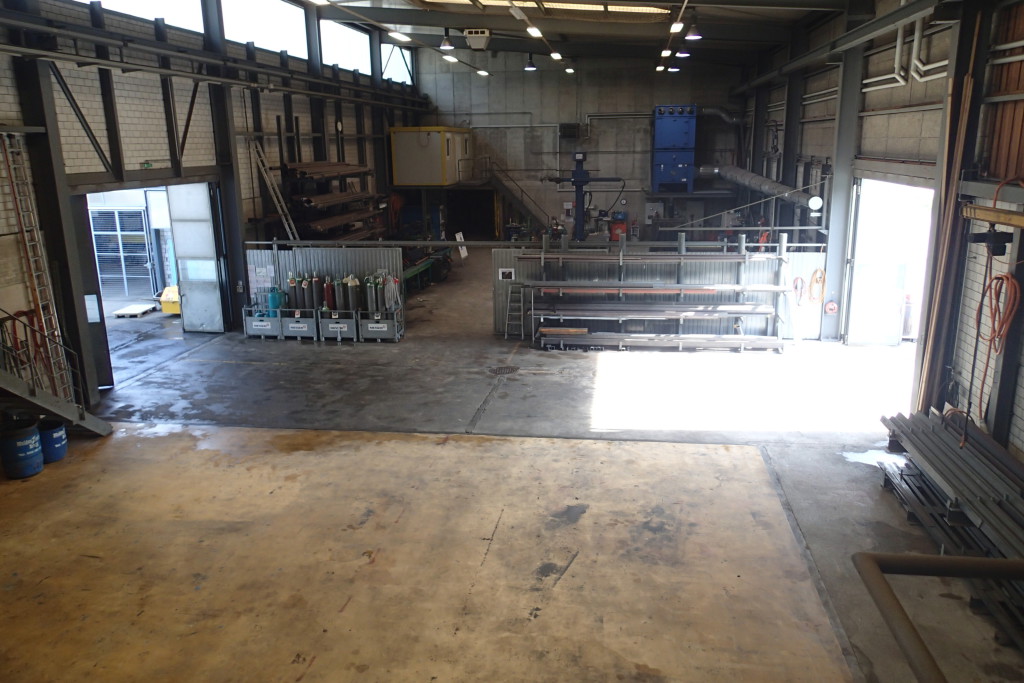
CHHeadquarters with plant, fabrication hall (approx. 1099 m²), procurement/sales and production
- Materials
- Steels, stainless steels (EN/ISO 15608 groups 1, 5.2, 6.4, 8.1, 10.2)
- Annealing machine fleet for thermal treatments
Components and services
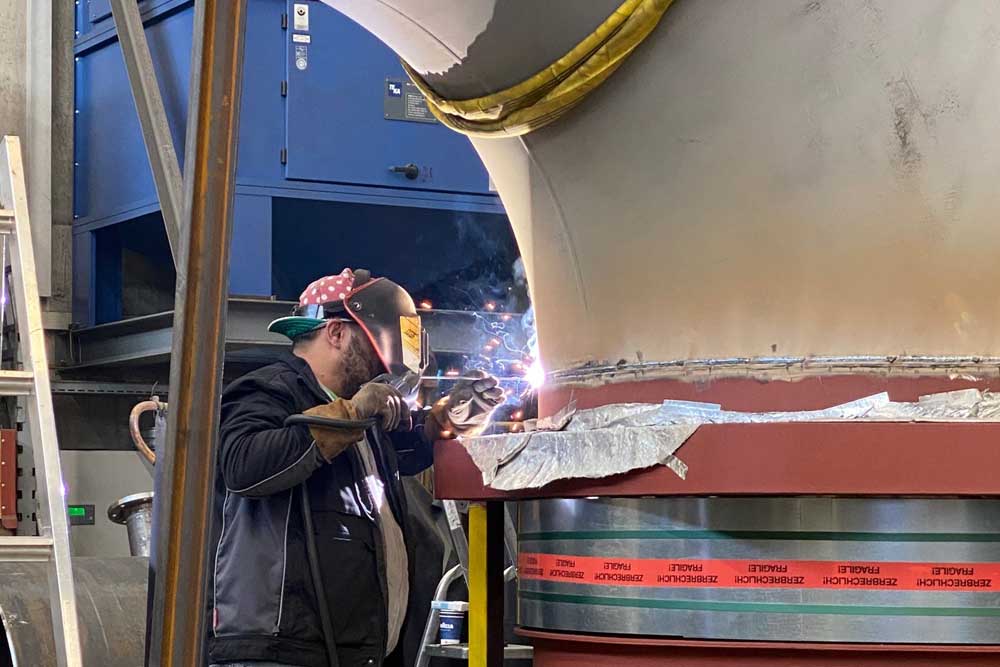
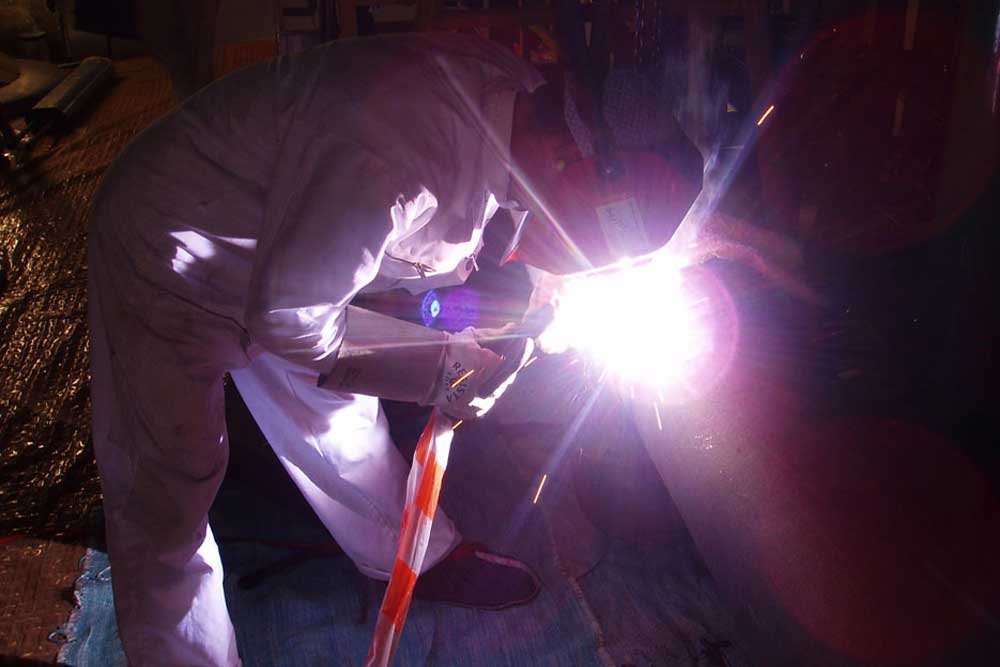
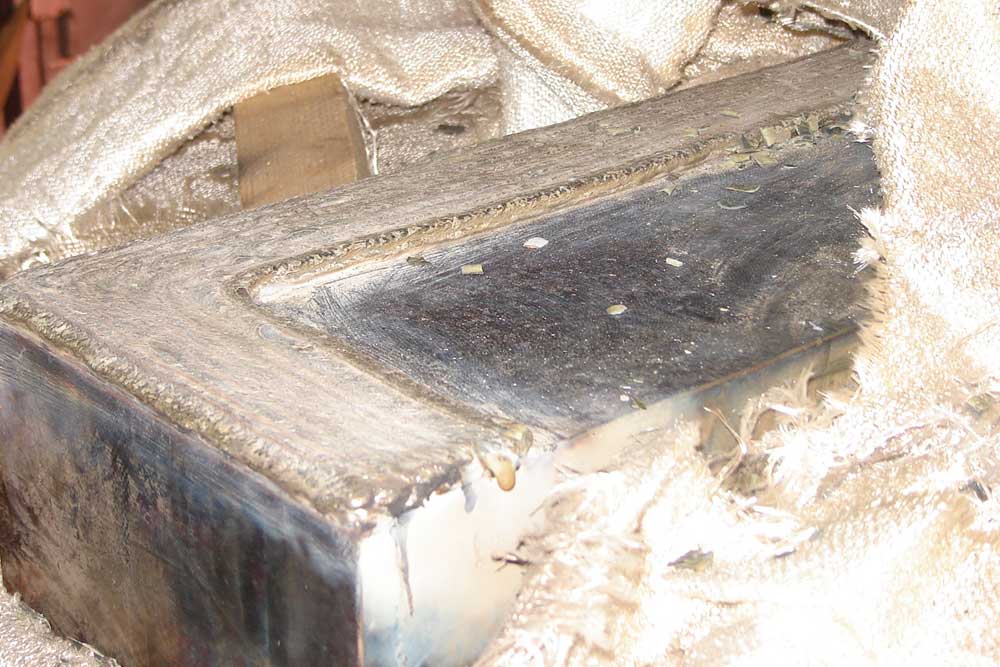
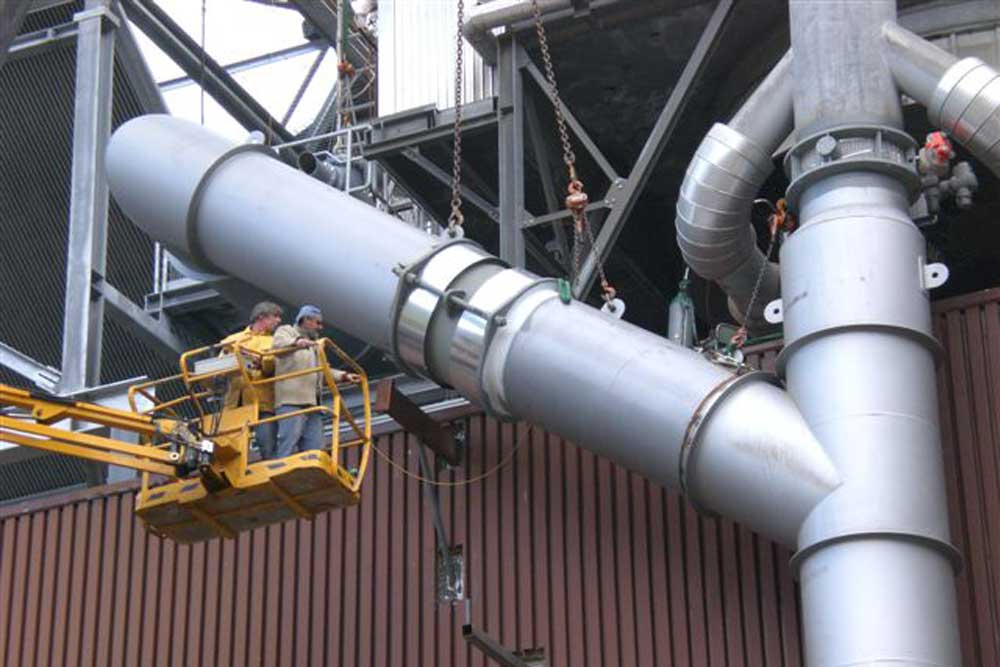
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Piping construction (prefabrication, in-house fabrication, assembly)Joining | – | – | – | – | – |
| TIG welding (141)Joining | – | – | – | – | Material groups 1, 1.1, 1.2, 5.2, 6.4, 8.1, 10.2 (EN/ISO |
| MMA welding (111)Joining | – | – | – | – | Material groups 1, 5.2, 6.4, 8.1, 10.2 (EN/ISO 15608) |
| TIG/MMA (141/111)Joining | – | – | – | – | Material groups 1, 5.2, 6.4, 8.1 (EN/ISO 15608) |
| MAG welding (135)Joining | – | – | – | – | Material groups 1, 5.2, 6.4, 8.1 (EN/ISO 15608) |
| TIG-v (141-v)Joining | – | – | – | – | Material groups 1, 5.2, 6.4, 8.1 (EN/ISO 15608) |
| Annealing service (thermal pre-, during- and post-treatment, annealing records and annealingHeat treatment | – | – | – | – | – |
| On-site shaft machining (pre-machining, weld overlay cladding, turning)Machining | g6 (Ø240mm) · N7 | – | – | – | – |
| Weld overlay welding (e.g. NIBAS buttering layer on material group 6.4, 1.4903; material group 5.2,Joining | – | – | – | – | 1.4903, 10CrMo910, NIBAS filler material |
| Plant construction / power plant construction (new installations and overhauls of wasteAssembly | – | – | – | – | – |
| Non-destructive testing VT – visual testing Level 2Testing | – | – | – | – | – |
| Non-destructive testing PT – dye penetrant testing Level 2Testing | – | – | – | – | all non-porous materials; mainly not |
| Service and maintenance (maintenance and overhaul work, welding assignments domestic/abroad,Assembly | – | – | – | – | – |
| District heating pipeline construction (general execution, assembly and laying of district heatingAssembly | – | – | – | – | – |
| Preparation of welding and annealing instructions, CAD execution drawings with material take-offsEngineering | – | – | – | – | – |
1 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| Annealing machine | – | – | – | – | Brugg (workshop) and on site |
Additional services
Quality and certificates
The company is certified according to ISO 9001:2015, ISO 3834-2 (fusion welding) as well as ISO 14001 and ISO 45001; testing is carried out by SGZP-certified testers (VT, PT Level 2) and a BAG permit for handling ionising radiation is held.
| Evidence | Brugg |
|---|---|
| ISO 9001:2015 | |
| ISO 14001:2015 | |
| ISO 45001:2018 | |
| ISO 3834-2 | |
| EN 1090 (EXC2) | |
| IATF 16949 | |
| EN 9100 | |
| ISO 13485 |
Company history
- 1990
Founded as a sole proprietorship by Rolf Hatt
- 2004
Conversion into a public limited company
- 2020
Acquisition by Manuel Blatter and Jan Wicki as succession solution
- 2024
Company founder Rolf Hatt unexpectedly passed away on 24.12.2024; the business is continued by the owners in his spirit