Electroplated surface finishing of steel parts: zinc plating, zinc nickel, zinc iron, phosphating, electropolishing and tempering.
Herbert Reinmuth GmbH
63927 Bürgstadt (Erfstraße 22) · 97076 Würzburg (Sandäcker 7)New on Amplifa
The Company
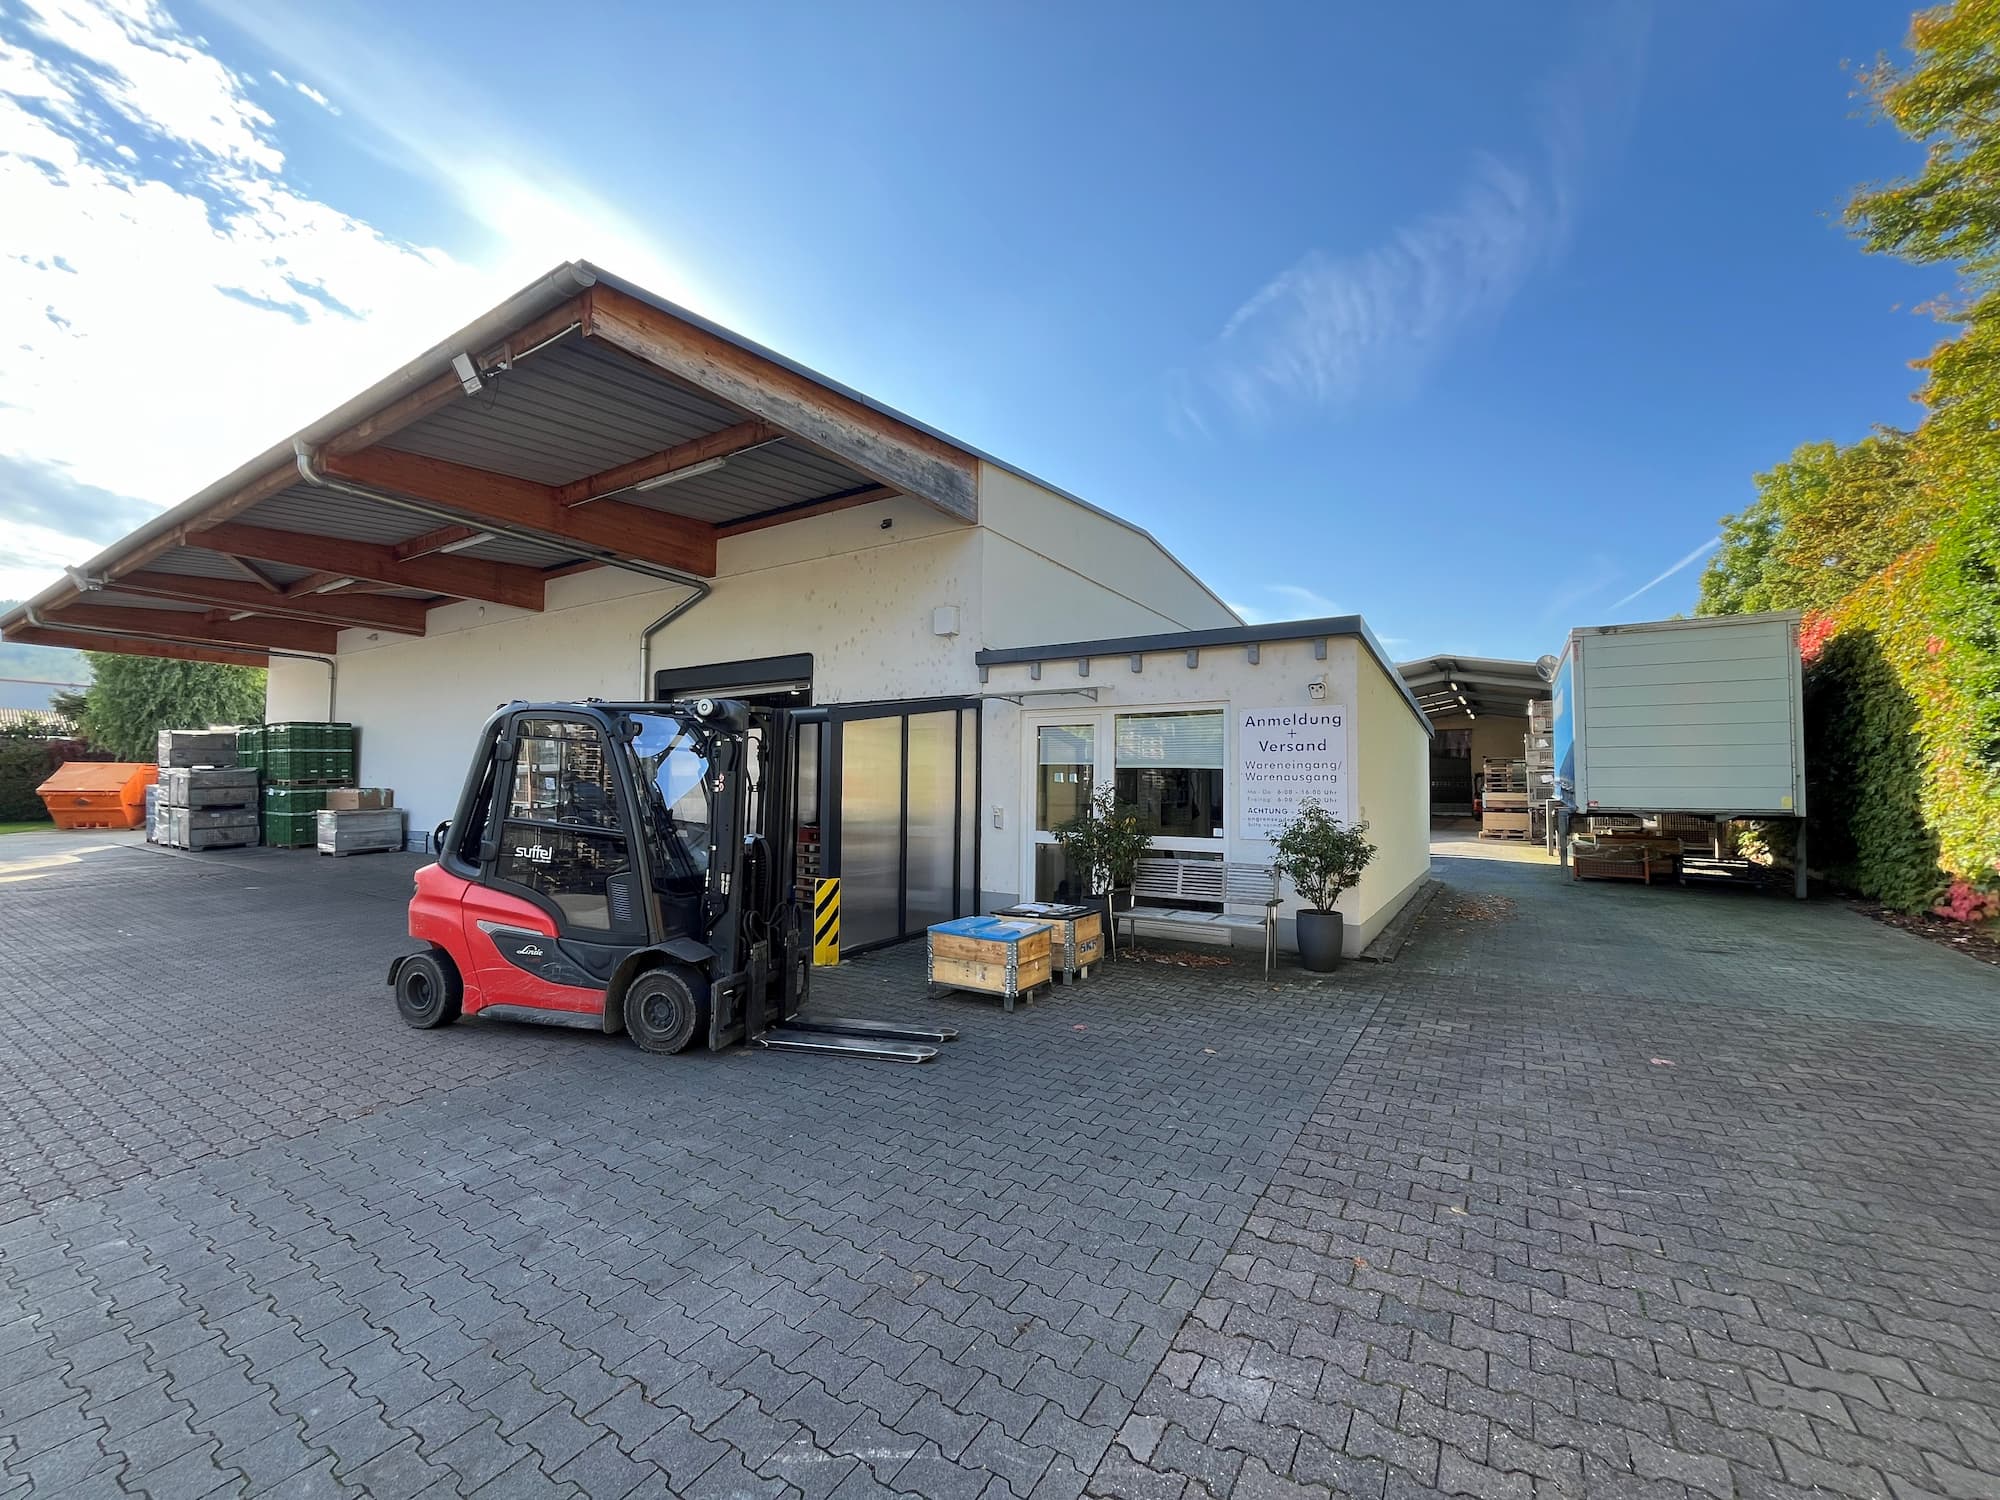
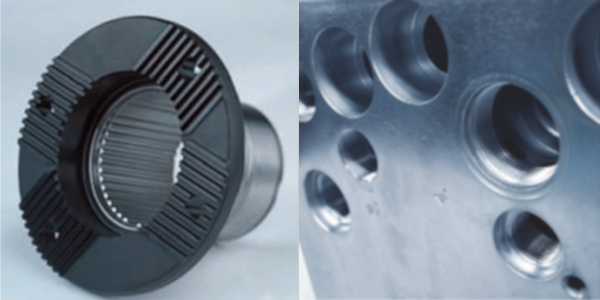
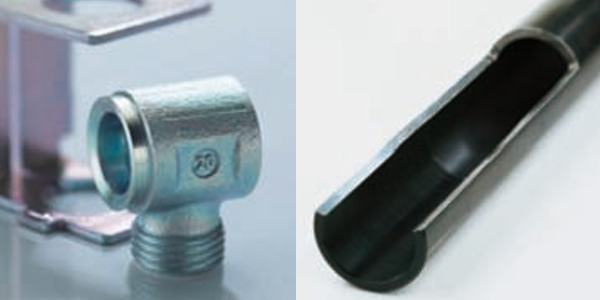
The Herbert Reinmuth GmbH is a company for electroplated surface finishing founded in 1972 and based in Bürgstadt am Main. At its headquarters, steel components are zinc-plated in rack and barrel processes (acid zinc) as well as coated with zinc nickel, zinc iron and zinc phosphate; further processes include electropolishing, tempering up to 300 °C and partial coating with custom masking fixtures. Special solutions include internal zinc plating of tubes and structural parts as well as cost-effective rack coating of hollow and drawing parts, as used in automotive engineering. Machinable dimensions are up to 3000 x 1000 x 400 mm at a maximum part weight of 300 kg. Together with its sister company HR Metallveredelung GmbH in Würzburg, the company belongs to the Reinmuth Galvanik Group and, since its acquisition by the KFB Bauer GmbH, to the KFB Surfaces Group with 11 companies at 8 sites in Germany, Austria and the Czech Republic. Corrosion protection and surfaces are approved for a wide range of industries, especially automotive engineering.
- Site
- Bürgstadt
- Processes
- Electroplated zinc plating (acid zinc), Electroplated zinc plating (acid zinc), barrel line, Zinc Nickel Coating, Zinc Iron Coating, Zinc Phosphate (Phosphating), Electropolishing, Partial coating to tight tolerances (masking fixtures), Internal zinc plating of tubes and structural parts
- Materials
- Steel, Electroplated zinc plating (acid zinc), Zinc Nickel Coating, Zinc Iron Coating, Zinc Phosphate (Phosphating), Electropolishing, Tempering up to 300 °C
- Certificates
- DIN EN ISO 9001, DIN EN ISO 14001
- Founded
- 1972
- Employees
- 60
- Industries
- Surface finishing, Electroplating, Coating, Automotive engineering, Corrosion protection
- 01
Consulting in the planning phase
- 02
Cleaning/pre-treatment
- 03
Electroplated coating (rack/barrel)
- 04
Passivation and post-treatment/sealing
- 05
Tempering (optional)
- 06
Testing in own laboratory (salt spray chamber, ICP, X-ray fluorescence)
- 07
Initial sample inspection report and delivery
Surfaces & Processes
Electroplated zinc plating (acid zinc)
Classic corrosion protection for steel on a rack line (up to 3000x1000x400 mm, 300 kg) and barrel line (up to 130 kg), passivation blue/transparent, post-treatment with sealing, friction additive or temporary preservation.
Zinc Nickel Coating
High-quality corrosion protection for steel with passivation in blue, transparent or black as well as sealing or temporary preservation.
Zinc Iron Coating
Process for steel components with passivation in blue, transparent or black and sealing with or without friction additive.
Zinc Phosphate (Phosphating)
Phosphating of steel parts on the rack followed by preservation.
Electropolishing
Electrochemical smoothing and finishing of metal surfaces.
Tempering up to 300 °C
Heat treatment of workpieces up to 2000 mm part length and 250 kg weight for hydrogen relief annealing/preservation.
Sites
Bürgstadt
DEHeadquarters, electroplating and coating site
- Part weight / size
- up to 3000 x 1000 x 400 mm, max. 300 kg (barrel: 130 kg)
- Lot size
- Series production; prototypes and sample processing by arrangement
- Materials
- Steel
- Rack line for zinc plating
- Barrel line for zinc plating
- Tempering oven (up to 300 °C, 2000 mm)
- Salt spray chamber
- Laboratory: ICP, titration, photometry, X-ray fluorescence
Würzburg
DESister site (HR Metallveredelung GmbH), electroplating
- Materials
- Steel
Components
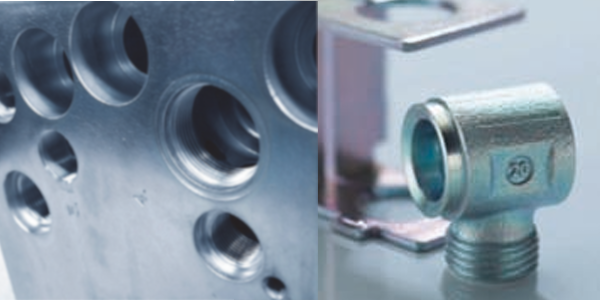
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Electroplated zinc plating (acid zinc)Surface | – | 3000 mm × 1000 mm × 400 mm | 300 kg | – | Steel |
| Electroplated zinc plating (acid zinc), barrel lineSurface | – | – | 130 kg | – | Steel |
| Zinc Nickel CoatingSurface | – | 3000 mm × 1000 mm × 400 mm | 300 kg | – | Steel |
| Zinc Iron CoatingSurface | – | 3000 mm × 1000 mm × 400 mm | 300 kg | – | Steel |
| Zinc Phosphate (Phosphating)Surface | – | 3000 mm × 1000 mm × 400 mm | 300 kg | – | Steel |
| ElectropolishingSurface | – | – | – | – | – |
| Partial coating to tight tolerances (masking fixtures)Surface | tight tolerances | – | – | – | – |
| Internal zinc plating of tubes and structural partsSurface | – | – | – | – | – |
| Coating of hollow and drawing parts (rack)Surface | – | – | – | – | – |
| Temporary preservation (post-treatment)Surface | – | – | – | – | – |
| Tempering up to max. 300°CHeat treatment | – | 2000 mm | 250 kg | – | – |
| Salt spray test according to DIN EN ISO 9227 (corrosion testing)Testing | – | – | – | – | – |
| Metal analysis by means of Inductively Coupled Plasma (ICP)Testing | – | – | – | – | – |
| Titration for chemical analysesTesting | – | – | – | – | – |
| PhotometryTesting | – | – | – | – | – |
| X-ray fluorescence analysisTesting | – | – | – | – | – |
| Consulting/optimization in the planning phase of components (engineering)Engineering | – | – | – | – | – |
4 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| Rack line (zinc plating) | – | – | 3000x1000x400 mm | – | Bürgstadt |
| Barrel line (zinc plating) | – | – | – | – | Bürgstadt |
| Tempering oven | – | – | 2000 mm | – | Bürgstadt |
| Salt spray chamber | – | – | – | – | Bürgstadt |
Additional services
Quality & Environment
Quality is assured through comprehensive testing procedures in all production areas: in the company's own laboratory, the salt spray test is carried out according to DIN EN ISO 9227 in a salt spray chamber, along with metal analyses using ICP, titration, photometry and X-ray fluorescence. The end of the process chain is marked by an initial sample inspection report.
| Evidence | Bürgstadt |
|---|---|
| DIN EN ISO 9001 | |
| DIN EN ISO 14001 |
History
- 1972
Foundation of the Herbert Reinmuth GmbH.
Acquisition of the Reinmuth Galvanik Group (Herbert Reinmuth GmbH and HR Metallveredelung GmbH) by the KFB Bauer GmbH; the company is today part of the KFB Surfaces Group with 11 companies at 8 sites in Germany, Austria and the Czech Republic.