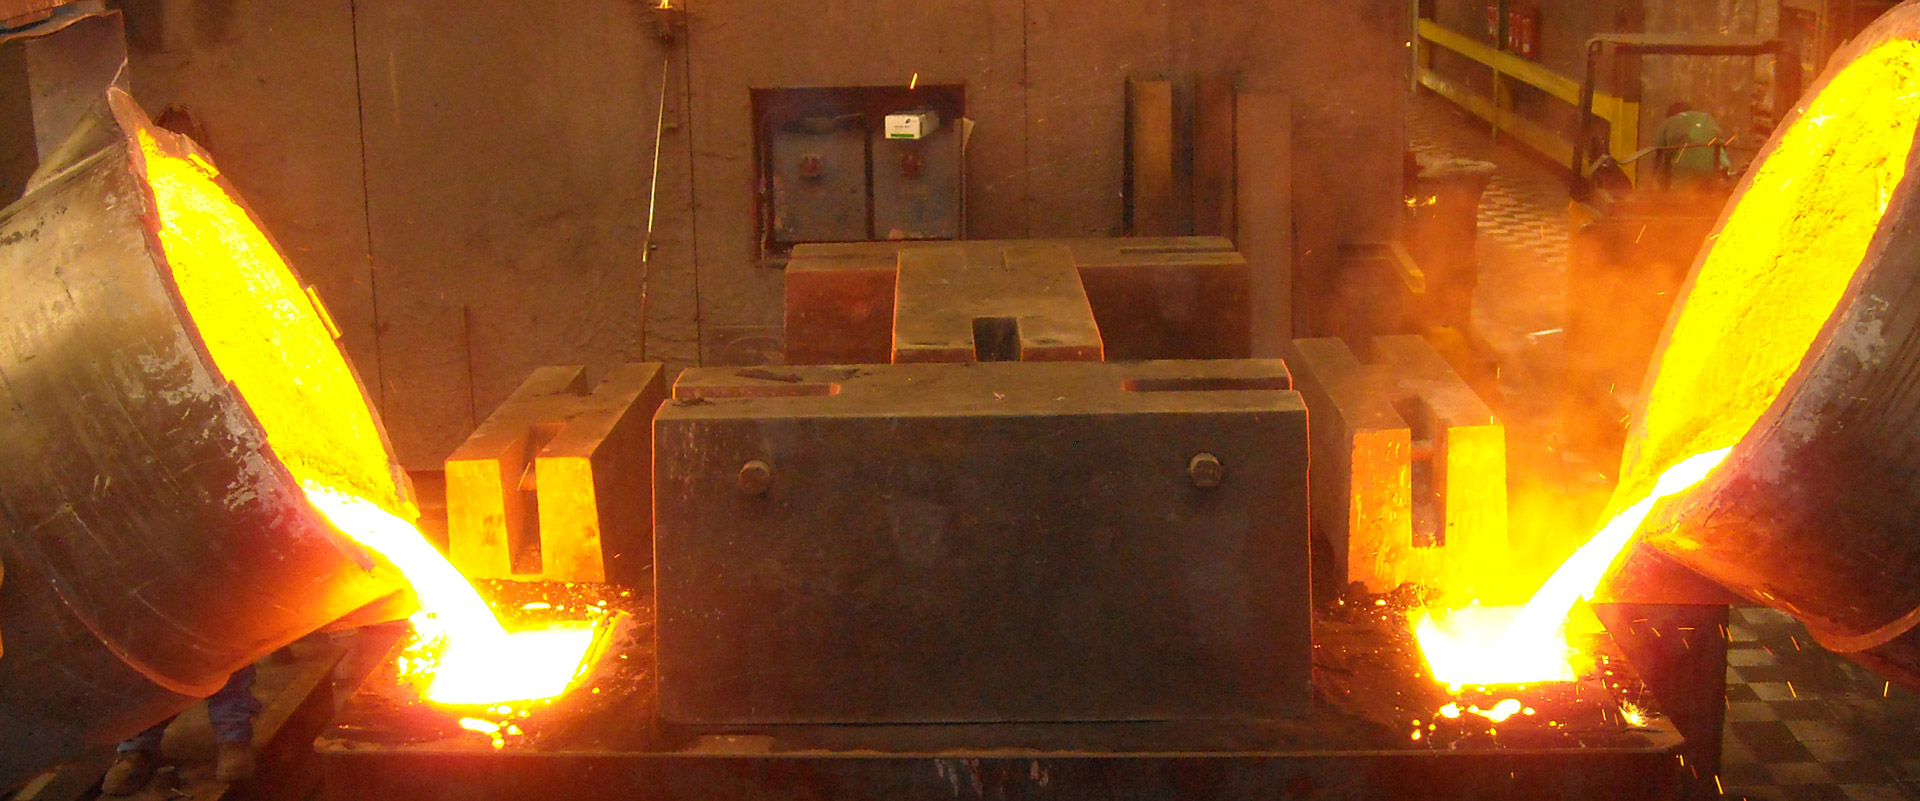
Hand-moulded engineering iron castings in EN-GJL and EN-GJS from one-off pieces to small series of 1,000 units
Karl Casper GmbH & Co. KG
Remchingen-Nöttingen (Headquarters / Foundry)New on Amplifa
About Karl Casper Guss
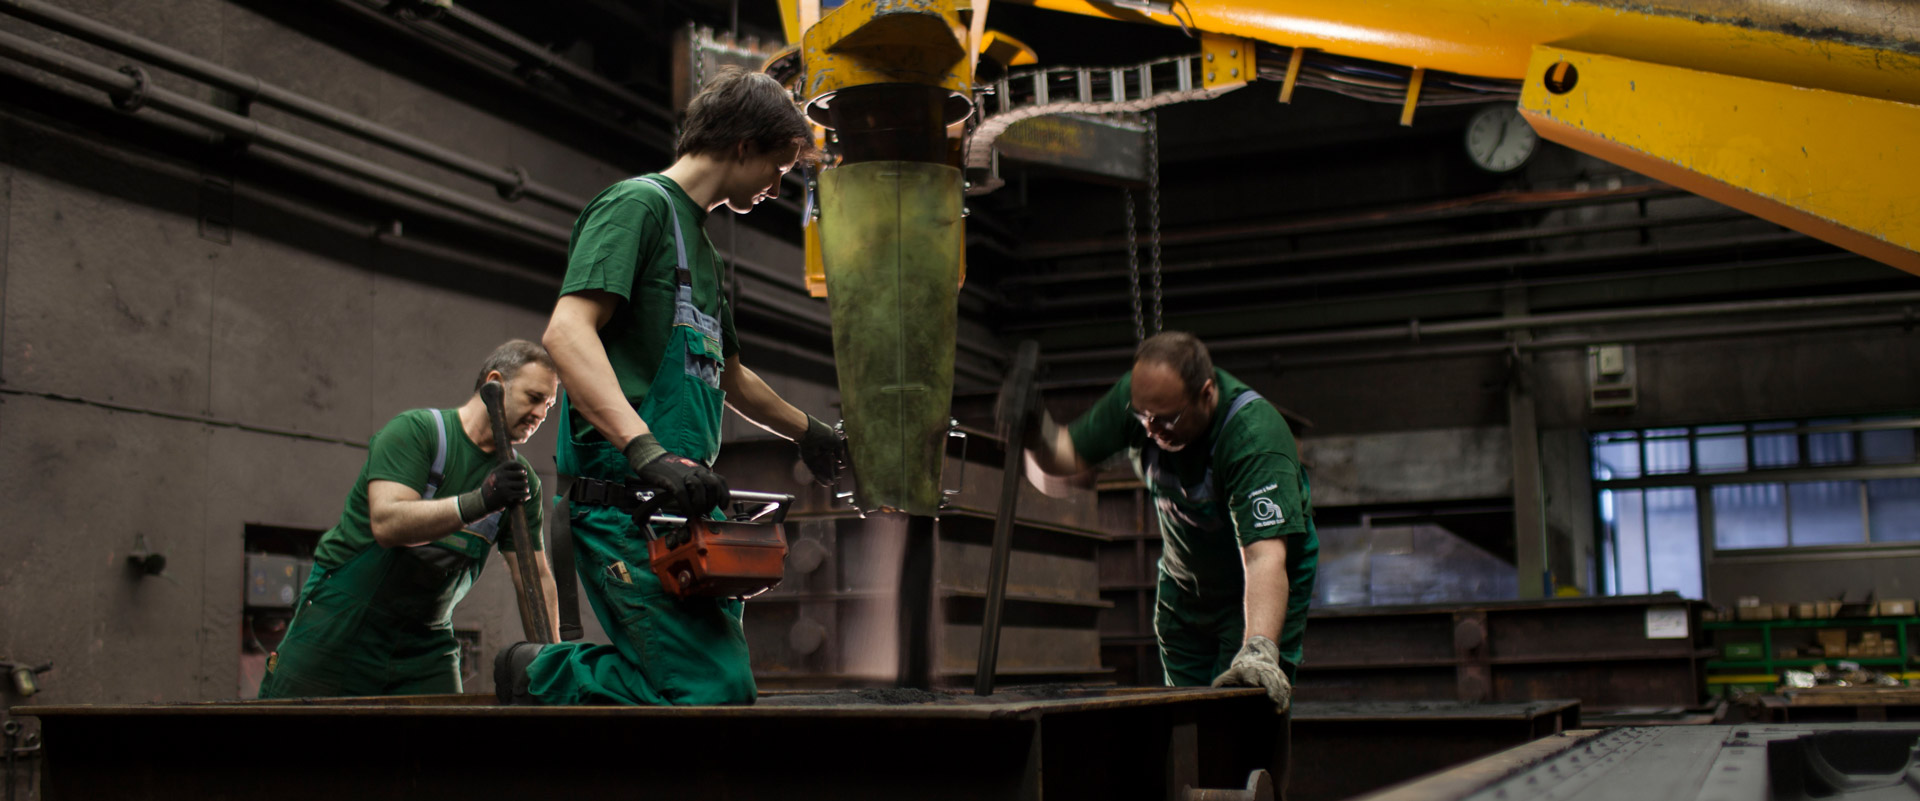
Karl Casper GmbH & Co. KG is a founder-managed foundry in its fifth generation, established in 1877 in Pforzheim and headquartered in Remchingen-Nöttingen (Baden-Württemberg). The company manufactures dimensionally accurate engineering iron castings on a contract basis using the hand-moulded sand casting process in grey cast iron with lamellar graphite (EN-GJL) and spheroidal graphite cast iron (EN-GJS), including the solid-solution-strengthened ferritic grades EN-GJS-450-18 to EN-GJS-500-14. Depending on the material, the castings weigh between 50 kg or 100 kg and 4 tonnes; quantities range from one-off pieces and prototypes made from polystyrene patterns to small series of 1,000 units made from wooden and plastic patterns. The value chain includes design and materials consulting, in-house pattern making from laminated wood, metal, synthetic resin or polystyrene foam, casting simulation with MAGMASOFT, heat treatment, fettling, priming, painting, machining through to ready-to-install delivery, as well as testing and assembly. Customers come from general mechanical engineering as well as tool, special machinery, shipbuilding and rail vehicle construction and injection moulding machine manufacturing. Around 90–100 employees work on the 26,000 m² site with 9,000 m² of built-up area. Art casting has been realised since 2018 in cooperation with external partner foundries.
- Site
- Remchingen-Nöttingen
- Processes
- Hand-moulded sand casting process (engineering iron casting), Grey cast iron (cast iron with lamellar graphite), Ductile iron casting (spheroidal graphite cast iron), Art casting (in cooperation with external partner foundries), Lost-wax casting (art casting, via partner foundries), Pattern making (wood and plastic patterns, polystyrene patterns), Machining of castings (as-cast or machined and ready-to-install), Fettling and post-processing (deburring at fettling stations)
- Materials
- Cast iron with lamellar graphite, Spheroidal graphite cast iron, Solid-solution-strengthened ferritic spheroidal graphite cast iron, Aluminium, Bronze, Iron (art casting), Grey cast iron with lamellar graphite (grey iron), Spheroidal graphite cast iron (ductile iron)
- Certificates
- DIN EN ISO 14001:2015, DIN EN ISO 9001:2015, DIN EN ISO 50001:2018, ISO 9001, ISO 14001, ISO 50001
- Founded
- 1877
- Employees
- around 90–100
- Industries
- General mechanical engineering, Machine tool construction, Special machinery construction, Injection moulding machine manufacturing, Shipbuilding, Rail vehicle construction
- 01
Design and materials consulting
- 02
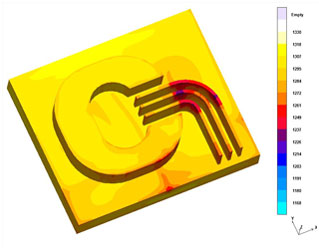
Casting simulation (MAGMASOFT)
- 03
Pattern making (wood, metal, synthetic resin, polystyrene foam)
- 04
Hand-moulded sand casting (EN-GJL, EN-GJS)
- 05
Heat treatment (hardening, annealing)
- 06
Fettling and post-processing
- 07
Priming and painting
- 08
Machining and ready-to-install delivery
- 09
Testing (mechanical and non-destructive)
- 10
Assembly and just-in-time delivery
Materials and Processes
Grey cast iron with lamellar graphite (grey iron)
Wear-resistant material insensitive to wall thickness variations, with high damping capacity and good machinability; castings from 50 kg to 4 t.
Spheroidal graphite cast iron (ductile iron)
Steel-like mechanical properties; properties can be modified by hardening and annealing; castings from 100 kg to 4 t.
Solid-solution-strengthened ferritic spheroidal graphite cast iron
Ferritic ductile iron for highly stressed castings with high toughness.
Solid-solution-strengthened ferritic spheroidal graphite cast iron
Ferritic ductile iron with increased strength for demanding mechanical engineering components.
Aluminium casting (art casting via partner foundries)
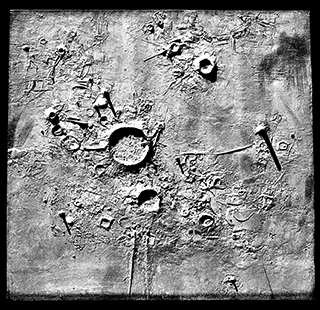
Used for art casting since 1961, e.g. façade panels of the Reuchlinhaus in Pforzheim.
Bronze casting (art casting via partner foundries)
Material for artworks produced by sand casting or lost-wax casting.
Location
Remchingen-Nöttingen
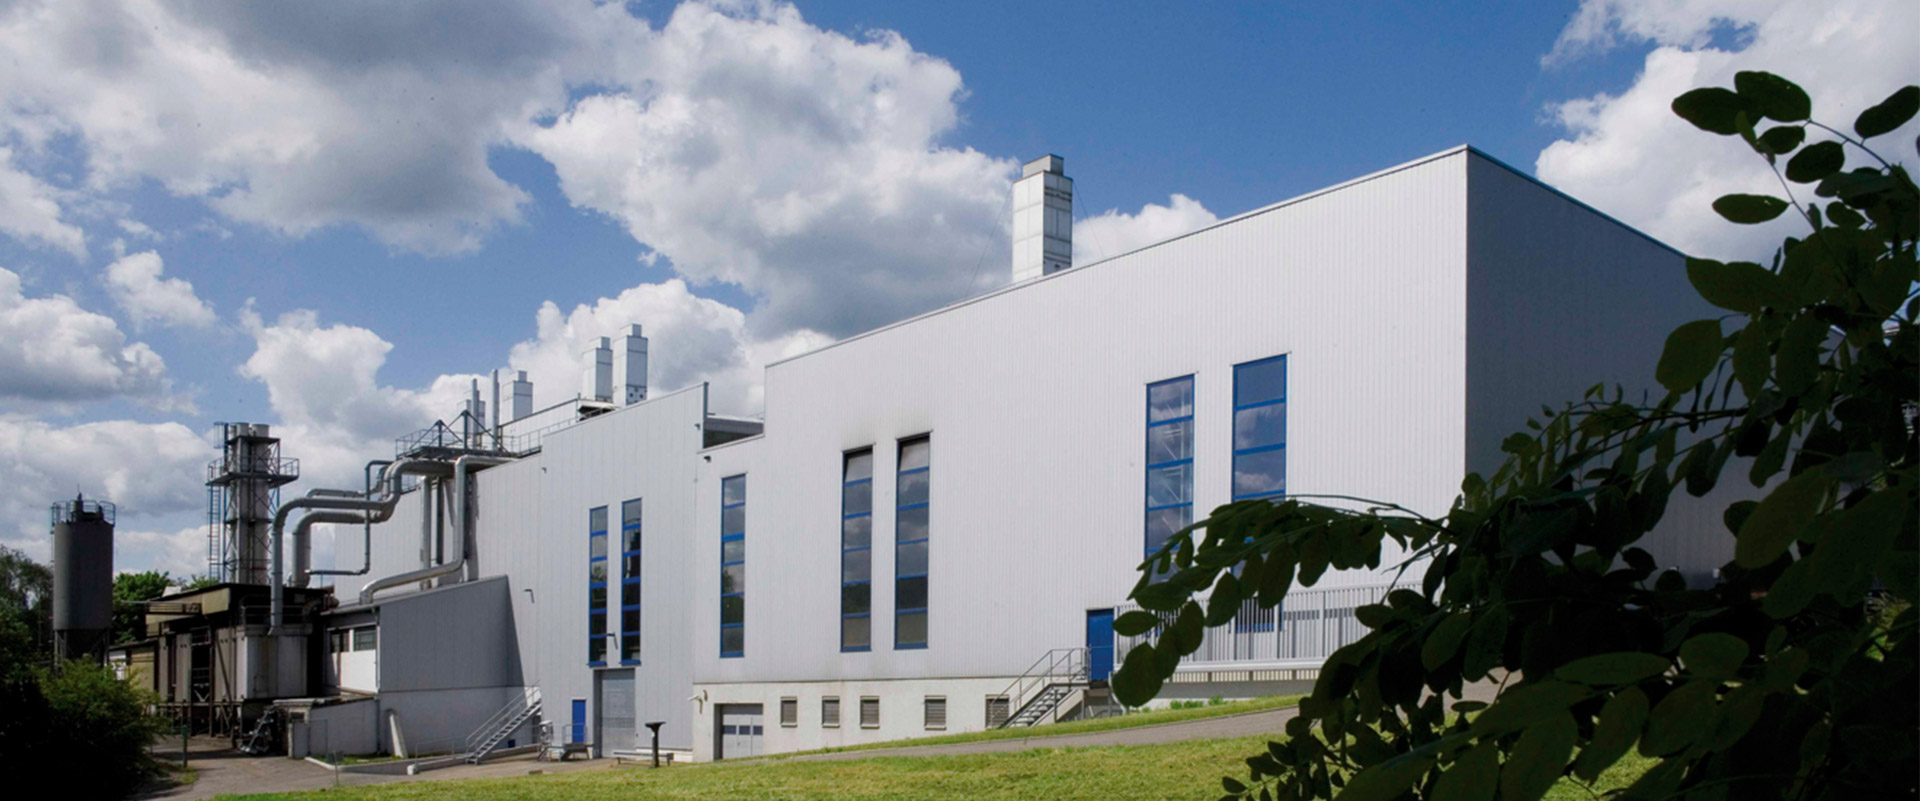
DEHeadquarters and foundry with hand moulding shop, pattern making, fettling shop, painting system and testing
- Part weight / size
- Castings 50/100 kg to 4 t (up to 9.5 t for
- Lot size
- One-off piece / prototype to 1,000 units
- Materials
- EN-GJL, EN-GJS (EN-GJS-450-18 to EN-GJS-500-14)
- 2 medium-frequency induction furnaces of 1.5 t each (from 1997)
- Electric furnace with doubled capacity (2018)
- Hand moulding shop (new building 2006)
- Fettling stations
- Painting system
- Gas-powered combined heat and power unit
Components
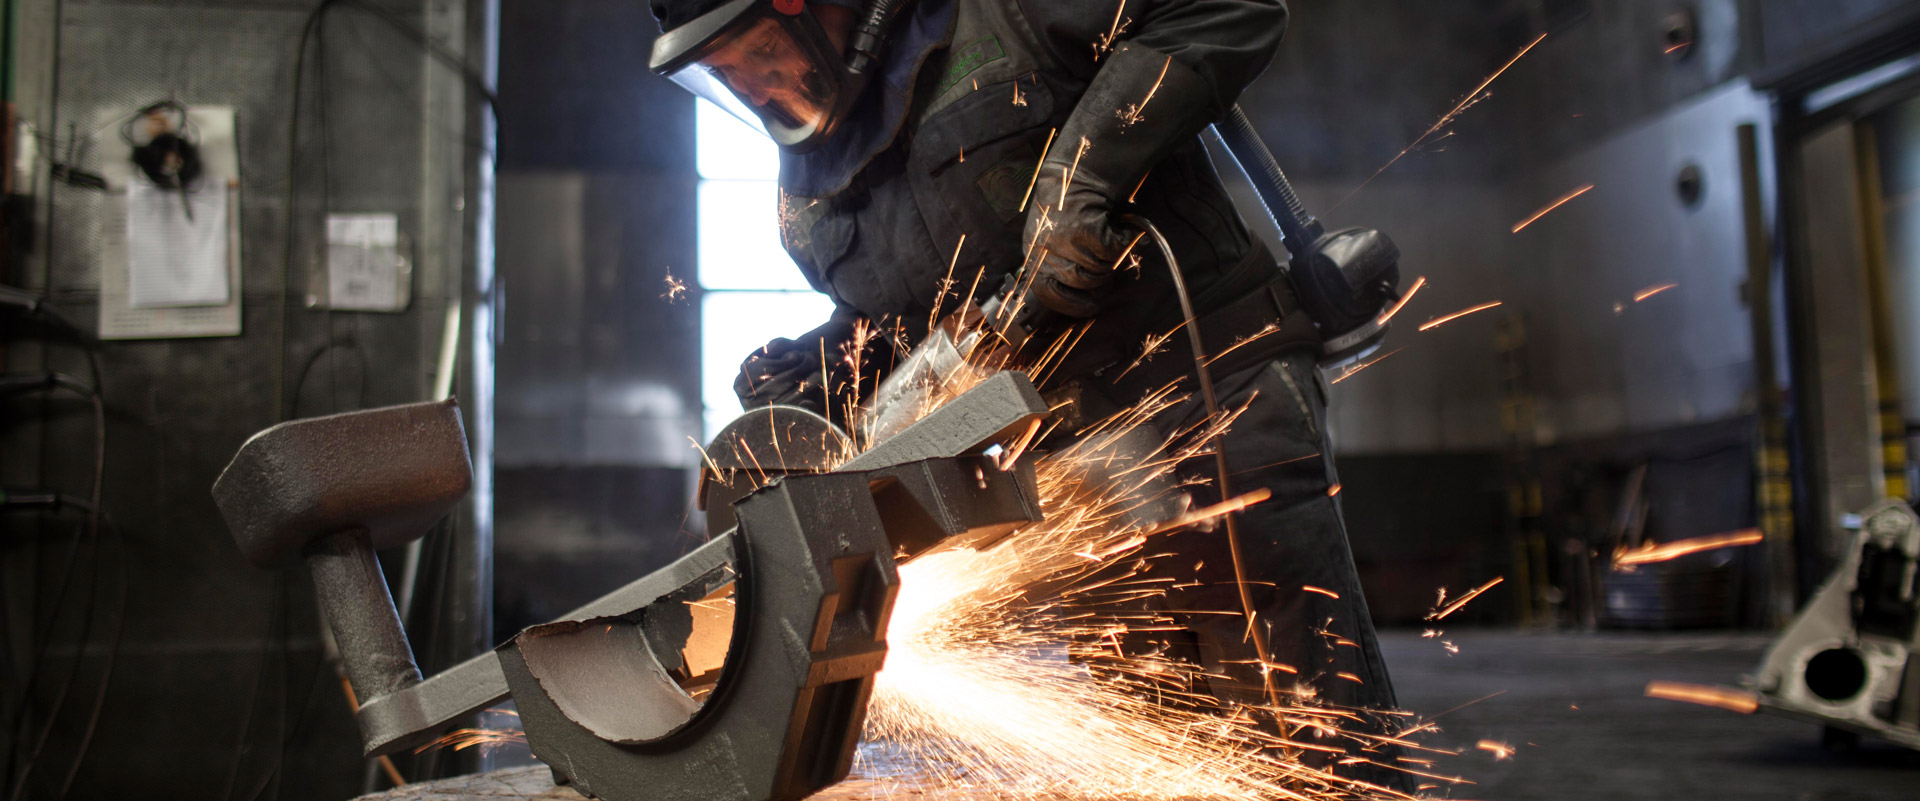
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Hand-moulded sand casting process (engineering iron casting)Casting | – | – | 100 kg – 9.5 tonnes | 1 (one-off piece) – 1,000 pieces | EN-GJL, EN-GJS |
| Grey cast iron (cast iron with lamellar graphite)Casting | – | – | 50 kg – 4 t | – | EN-GJL, GG |
| Ductile iron casting (spheroidal graphite cast iron)Casting | – | – | 100 kg – 4 t | – | EN-GJS, GGG, EN-GJS-450-18, EN-GJS-500-14 |
| Art casting (in cooperation with external partner foundries)Casting | – | 21 m (height of largest works to date) × 7 m diameter × 21 m | – | – | Iron, Aluminium, Bronze |
| Lost-wax casting (art casting, via partner foundries)Casting | – | – | – | – | Iron, Aluminium, Bronze, Ceramic, Fireclay |
| Pattern making (wood and plastic patterns, polystyrene patterns)Engineering | – | – | – | – | Laminated wood, Metal, Synthetic resins, Polystyrene foam |
| Machining of castings (as-cast or machined and ready-to-install)Machining | – | – | – | – | EN-GJL, EN-GJS |
| Fettling and post-processing (deburring at fettling stations)Surface | – | – | – | – | EN-GJL, EN-GJS |
| Annealing (heat treatment on customer request)Heat treatment | – | – | – | – | EN-GJL, EN-GJS |
| Hardening (heat treatment, property modification for ductile iron)Heat treatment | – | – | – | – | EN-GJS |
| Priming and painting (own painting system)Surface | – | – | – | – | EN-GJL, EN-GJS |
| Testing: tensile testing, notched bar impact bending testing, microstructure examinations, hardnessTesting | – | – | – | – | EN-GJL, EN-GJS |
| Assembly (including structural work, fountain installation, water engineering)Assembly | – | – | – | – | – |
| Design consulting and materials consultingEngineering | – | – | – | – | – |
| Casting simulation and residual stress calculation (MAGMASOFT/Magma)Engineering | – | – | – | – | – |
| Furan sand regenerationCasting | – | – | – | – | – |
7 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| Medium-frequency induction furnaces | – | 2 | 1.5 tonnes each | 1997 | Remchingen |
| Electric furnace (E-furnace) | – | – | – | – | Remchingen |
| Cupola furnace | – | – | – | – | Remchingen |
| Painting system | – | 1 | – | 2000 | Remchingen |
| Fettling stations (casting fettling shop) | – | – | – | – | Remchingen |
| Hand moulding shop (hall for hand-moulded casting) | – | – | – | 2006 | Remchingen |
| Gas-powered combined heat and power unit | – | 1 | – | – | Remchingen |
Additional services
Reference customers
Quality
Quality assurance includes tensile testing, notched bar impact bending testing, hardness testing, microstructure examinations, ultrasonic and dye penetrant testing. All quality-relevant data is documented via the cast-in piece number; customers can follow production in real time via the extranet portal.
| Evidence | Remchingen-Nöttingen |
|---|---|
| ISO 9001 | |
| ISO 14001 | |
| ISO 50001 |
History
- 1877
Founded in Pforzheim
- 1953
Karl Casper begins building the “white foundry” at the present-day Remchingen site
- 1961
First art casting: façade panels in aluminium casting for the Reuchlinhaus Pforzheim
- 1976
Philosophy “The white foundry in the countryside” under Till Casper; construction of foundry halls, a cupola furnace melting plant and furan sand regeneration
- 1992
Rudolf Eberle Prize (Innovation Prize of Baden-Württemberg) for furan sand regeneration
- 1997
Commissioning of two 1.5-tonne medium-frequency induction furnaces for spheroidal graphite cast iron
- 2002
125 years of Casper Guss
- 2006
Felix Casper joins the company; new building for the hand moulding shop
- 2007
Felix Casper becomes managing director; Malte Lüking takes over as technical director
- 2010
Launch of Casper 4.0 (Industry 4.0 / smart factory)
- 2012
Introduction of the MAGMASOFT simulation software; roofing of the charge preparation area
- 2014
“The transparent foundry”: customers observe production in real time via the extranet
- 2016
New building for the box hall and logistics centre; award “100 Places for Industry 4.0 in Baden-Württemberg”
- 2018
Shut-down of the cupola furnace and doubling of the electric furnace capacity; departure of Till Casper from the management; focus on industrial iron casting, discontinuation of in-house art casting production
- 2022
Renovation of the filling station for medium-sized castings
- 2023
Conversion of the filling hall for large castings