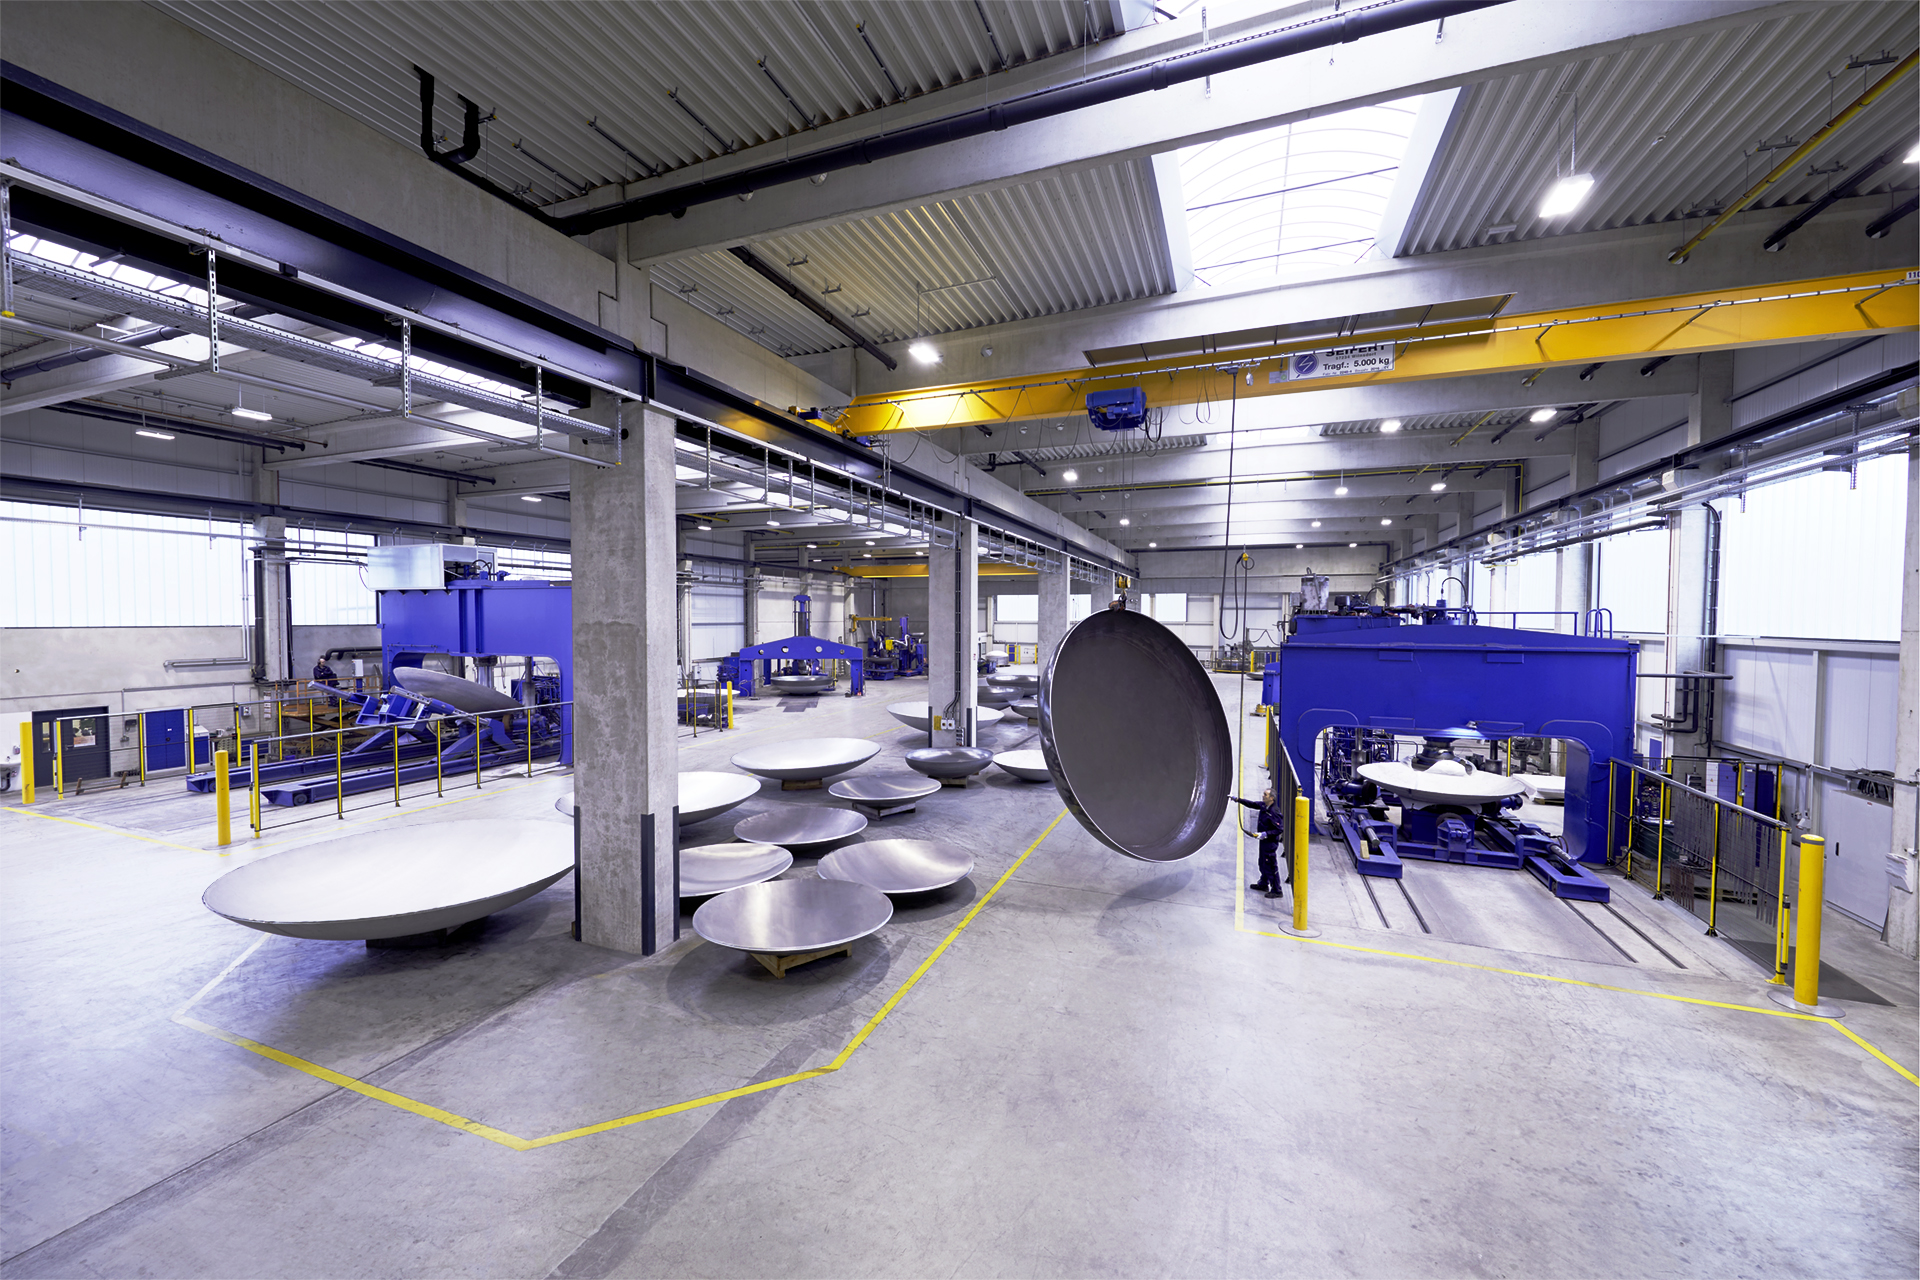
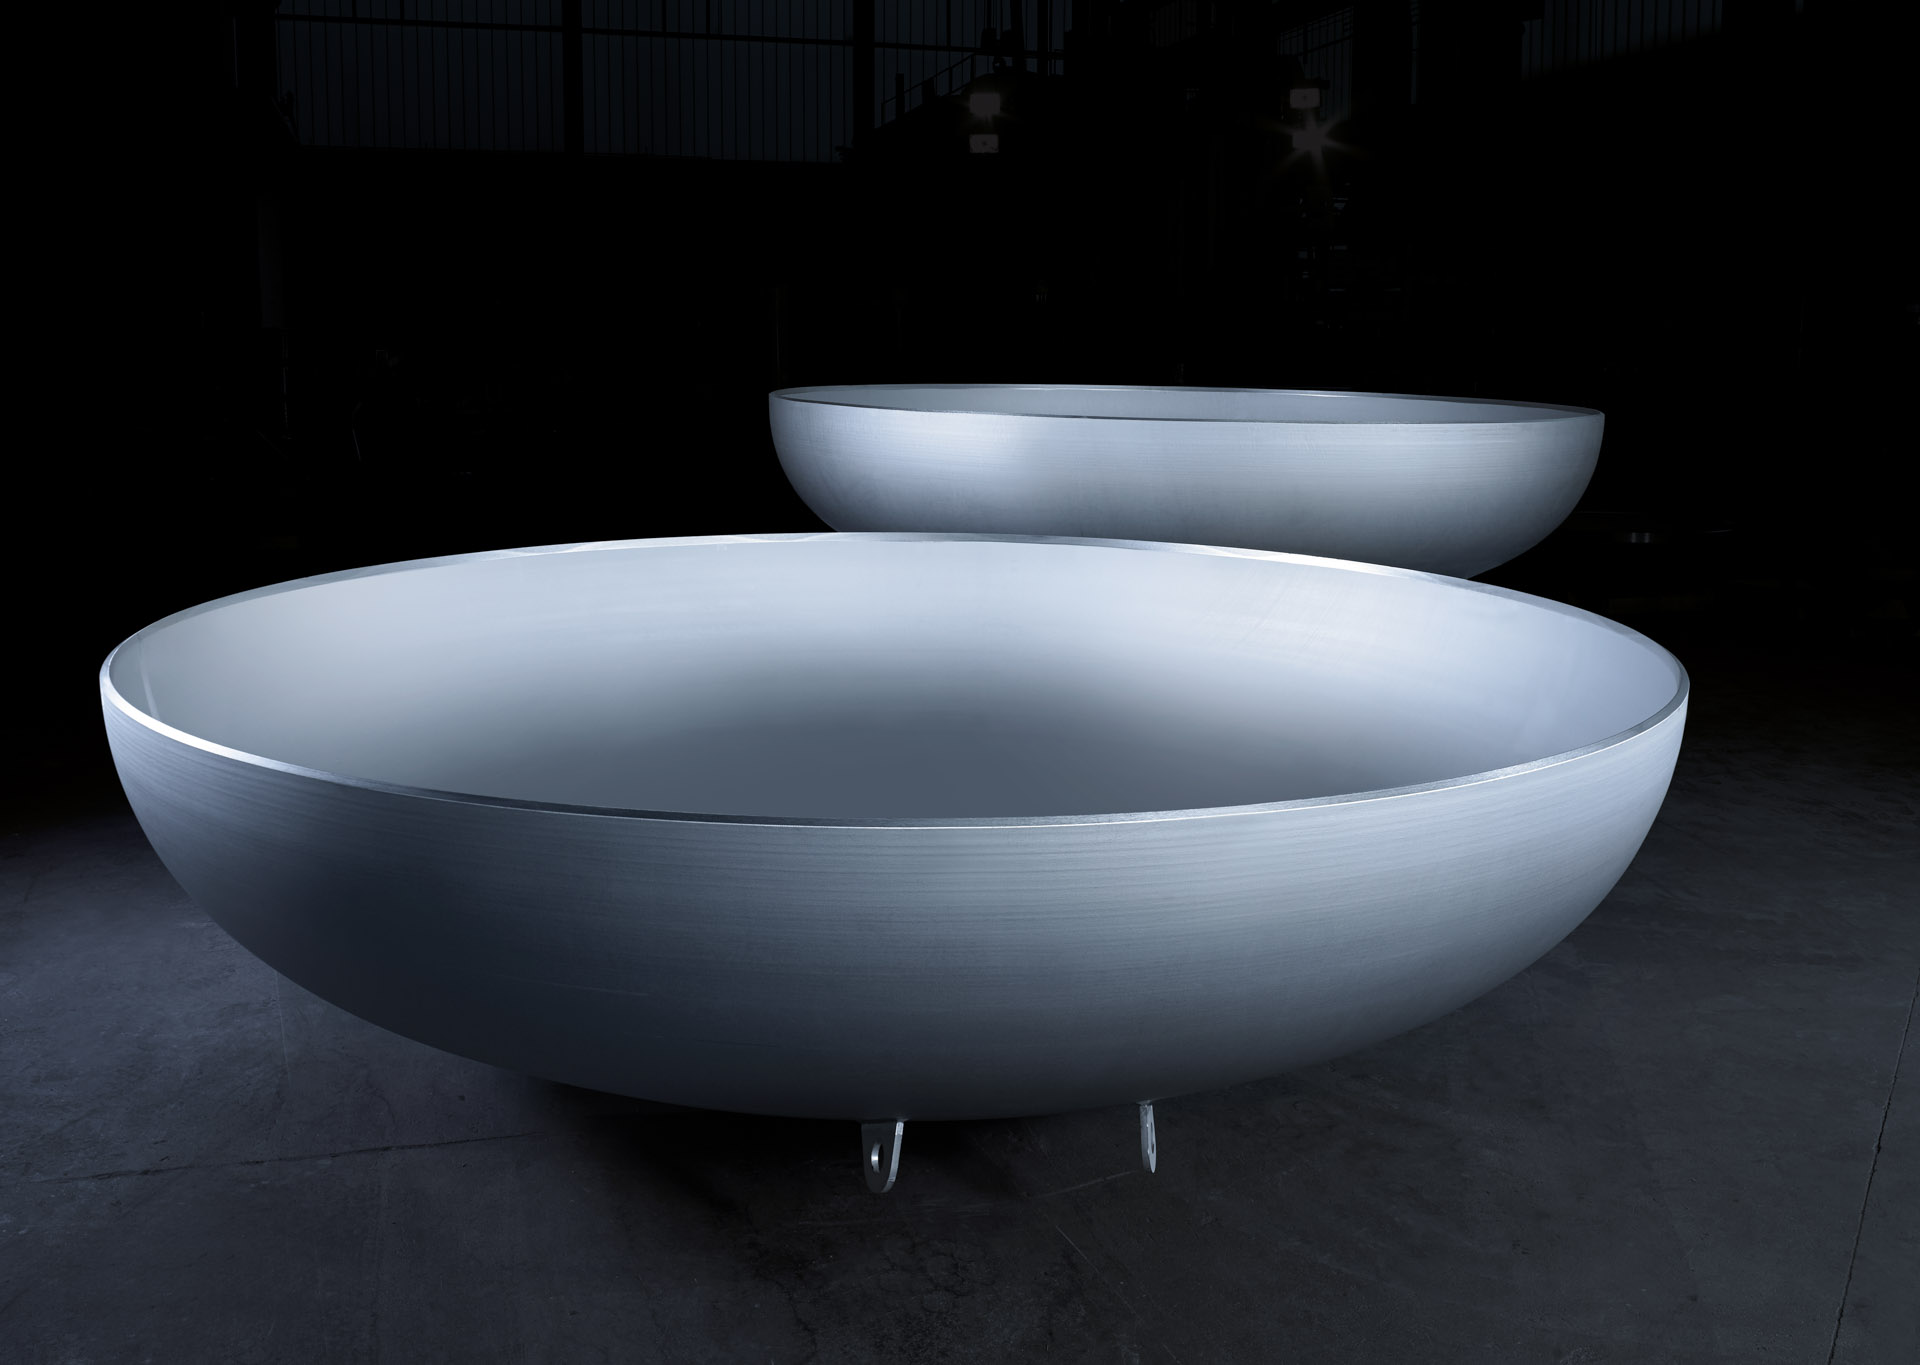
Manufacturer of vessel heads, cones and special pressed parts up to 13.500 mm diameter for vessel, apparatus and plant engineering.
KÖNIG + CO. GmbH
57250 Netphen · 35708 HaigerNew on Amplifa
Experience. Quality. Future.
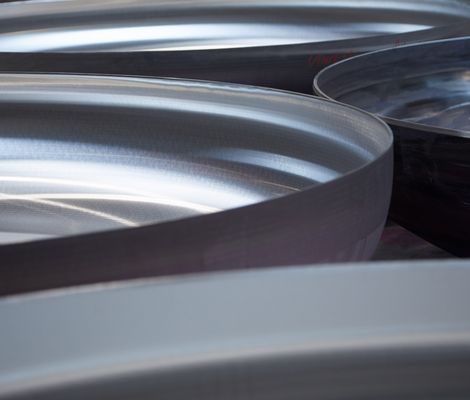
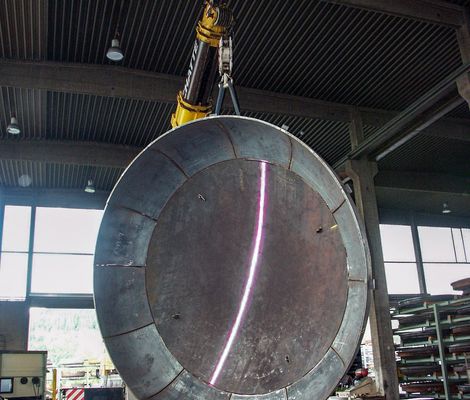
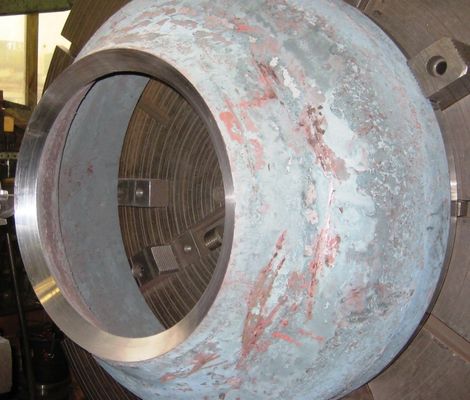
KÖNIG + CO. GmbH is a company founded in 1930 in Netphen with more than 240 employees, specialising in the forming of vessel heads, cones, special pressed parts, storage heads and welded constructions. The manufacturing range includes cold and hot pressing (deep drawing of heads from 21,3 to 2.100 mm diameter with wall thicknesses of 2 to 200 mm) as well as spinning and flanging of one-piece heads up to 8.200 mm diameter, 120 mm wall thickness and 30 tonnes unit weight. In addition, heat treatment (normalizing, tempering, PWHT, solution and soft annealing), various welding processes, 3D flame cutting, edge working and surface treatment such as sandblasting, pickling and grinding are offered. Materials processed include boiler plate, fine-grain and CrMo steels, stainless steels, duplex and superduplex materials, nickel alloys, titanium, zirconium, tantalum, aluminium, brass and copper. Customers come from the chemical and pharmaceutical industries, energy and power plant engineering, oil and gas, LNG/cryogenics, the beverage and food industry as well as storage and transport. The main plant is located in Netphen (approx. 65.000 m²), with a branch plant in Haiger (22.000 m², exclusively white-line production of stainless materials).
- Site
- Netphen
- Processes
- Cold and hot pressing (deep drawing of heads), Spinning and flanging (cold and hot), Heat treatment – normalizing (850-980°C), Heat treatment – tempering (650-750°C), Stress-relief annealing / PWHT (595-720°C), Solution annealing (1000-1180°C), Soft annealing, Welding – plasma-TIG welding
- Materials
- Boiler plate, Fine-grain structural steel, CrMo steel, Stainless steel, Duplex, Superduplex, Aluminium, Brass
- Certificates
- DIN EN ISO 9001:2015, DIN EN ISO 50001:2018, ASME PRT Certification Div.1, ASME PRT Certification Div.2, AD-2000 Merkblatt HP 0, AD-2000 Merkblatt W 0, PED 2014/68/EU Anhg. I 3.1 + DIN EN ISO 3834-2, PED 2014/68/EU Anhg. I 4.3, DNV Zulassung (Pressed Parts, DNV-CP-0350), NORSOK M-650 (mehrere Werkstoffe), BV Mode II Scheme, LRS Schweißverbindungen Druckbehälter Class 2.1, DIN EN ISO 9001, DIN EN ISO 50001, ASME PRT (Div. 1 and Div. 2), AD-2000 HP 0 / W 0, PED 2014/68/EU + ISO 3834-2, DNV-CP-0350 (Pressed Parts), NORSOK M-650, Lloyd's Register / Bureau Veritas
- Founded
- 1930
- Employees
- 240+
- Industries
- Chemical and pharmaceutical plants, Energy and power plant engineering (including the nuclear sector), Oil and gas industry, Liquefied natural gas (LNG) and cryogenic plants, Beverage and food industry, Storage and transport
- 01
Material selection and cutting (3D flame cutting)
- 02
Cold/hot pressing or spinning and flanging
- 03
Heat treatment
- 04
Welding / edge working
- 05
Surface treatment
- 06
Testing in the materials testing laboratory
- 07
Documentation and dispatch
Forming of Special Materials
Boiler plate and fine-grain structural steel (e.g. P235GH, P355N)
Standard materials for pressure vessel heads in cold- and hot-formed condition.
CrMo steel
For high-temperature-resistant applications in energy and power plant engineering.
Austenitic stainless steels (among others 1.4301, 1.4307, 1.4404, 1.4571)
For chemical, pharmaceutical and food-grade applications.
Duplex 1.4462 (S31803/S32205)
High strength and corrosion resistance, among others with NORSOK M-650 approval.
Superduplex S32750 and S31254
For aggressive media in oil and gas as well as chemical plants.
Nickel steel X8Ni9 (9 % Ni)
For cryogenic LNG applications with high impact toughness at low temperatures.
Super austenitic N08926
Seawater- and acid-resistant material with NORSOK approval.
Nickel alloys
For corrosion- and heat-exposed vessels in plant engineering.
Titanium, zirconium, tantalum
Special materials for extreme chemical applications, also as clad material combinations.
Aluminium EN AW-5083
For cryogenic and lightweight vessel applications, DNV-approved.
Copper, CuNi30Mn1Fe, brass
For special applications, among others in apparatus engineering.
Non-magnetizable steel 1.3964
For applications with magnetic requirements, DNV-approved.
Our Locations
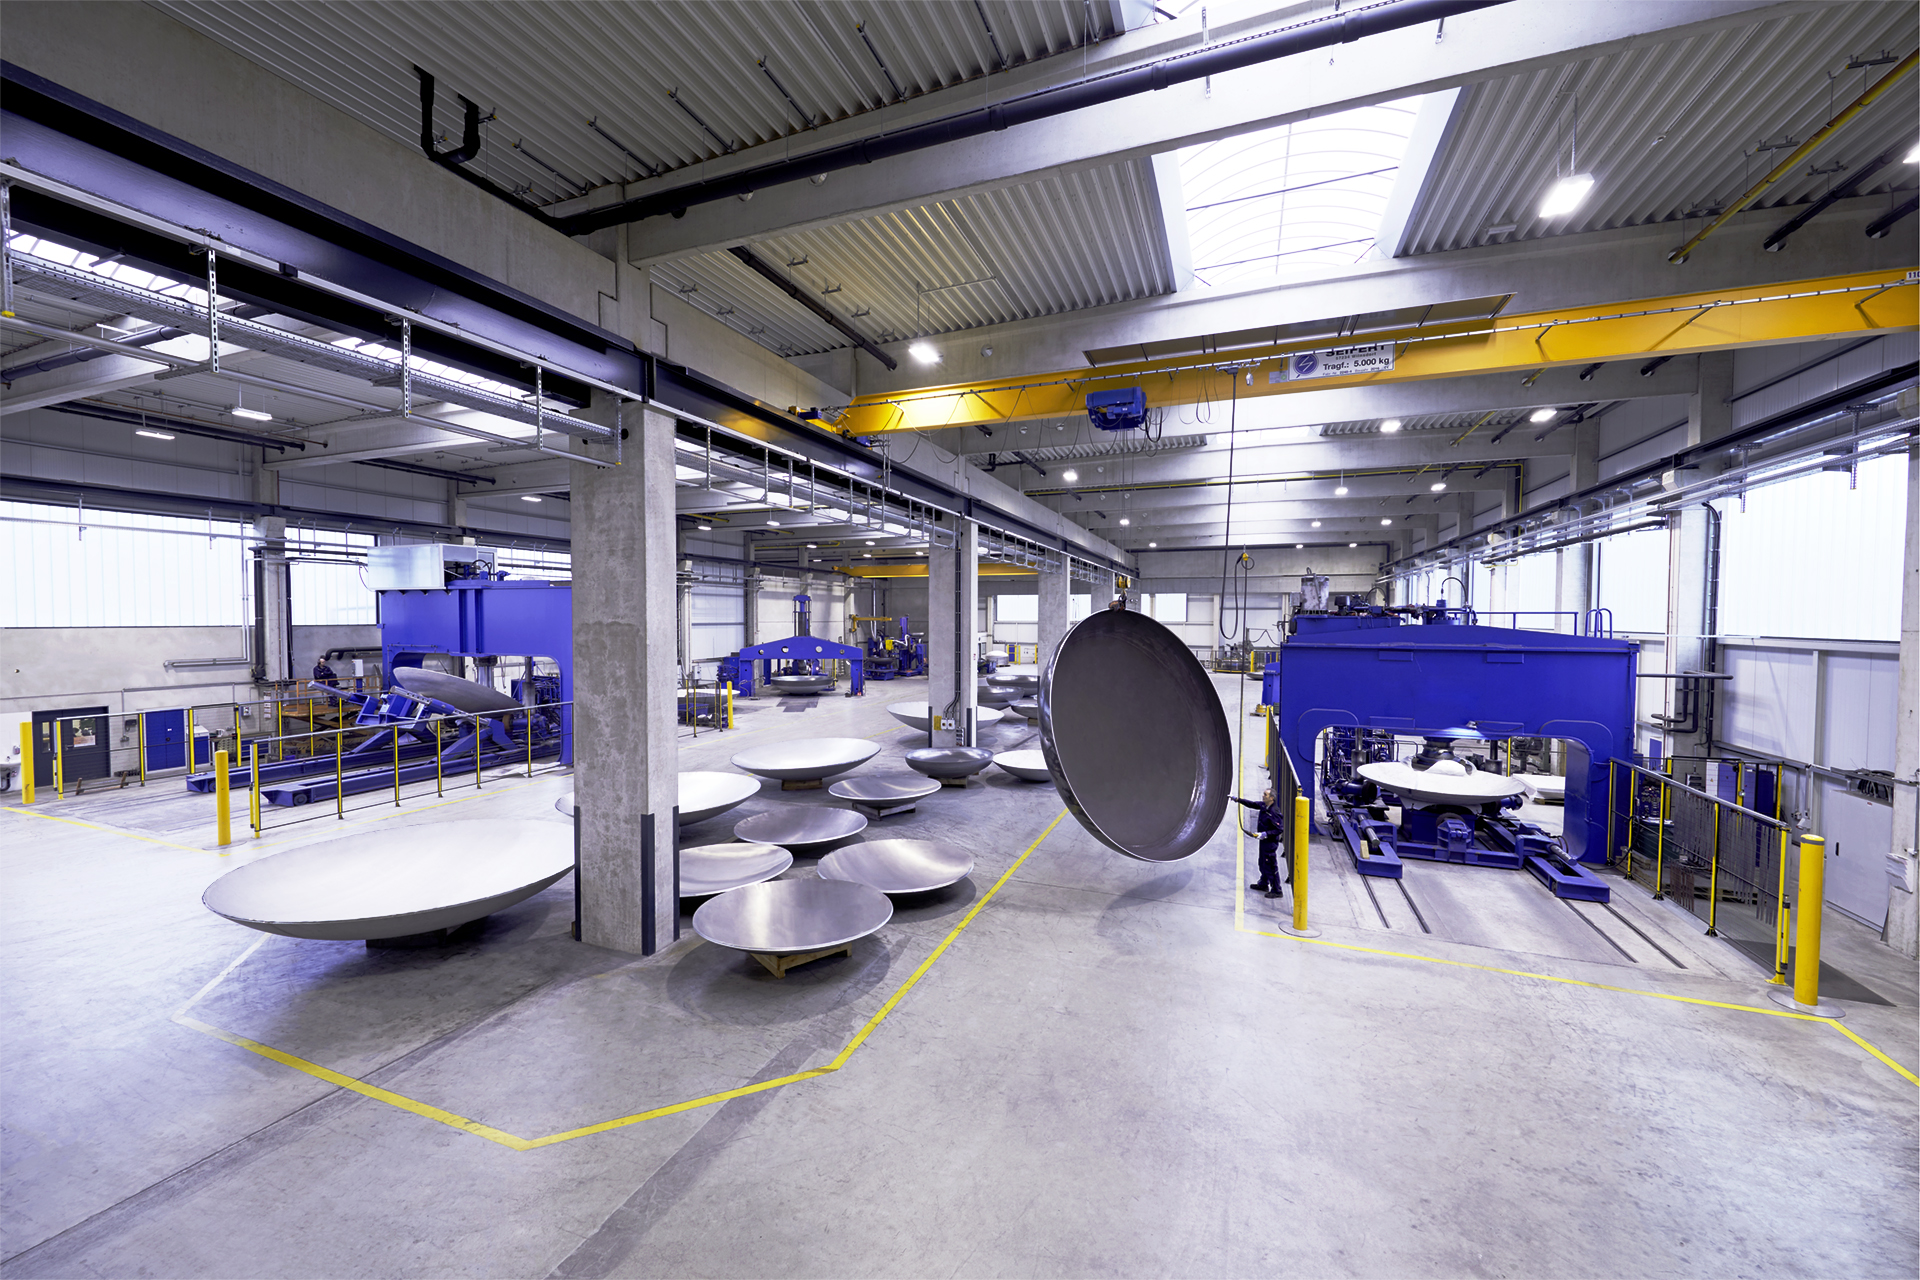
Netphen
DEMain plant (head plant), approx. 200 employees
- Part weight / size
- up to 30 t unit weight, one-piece heads up to 8.200 mm
- Lot size
- Single-item and small-series production
- Materials
- Boiler plate, fine-grain structural steel, CrMo steel, stainless steel, duplex, superduplex, nickel alloys, titanium,
- Hot spinning press
- Cold and hot flanging machine (heads up to 8.000 mm)
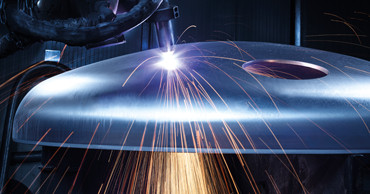
- 3D robot cutting system (plasma up to 85 mm, oxy-fuel up to 200 mm)
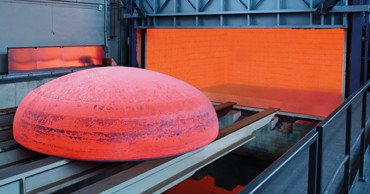
- Gas-fired high-performance chamber furnace 8.200 × 8.200 mm, max. 1200 °C
- 500.000-litre water quenching tank
- 40-t charging system
- Spindle presses
Haiger
DEBranch plant, exclusively white-line production of stainless materials (integration of the Hockenheim plant)
- Part weight / size
- Heads 1.500–6.500 mm diameter, thin-walled heads
- Lot size
- Single-item and small-series production
- Materials
- Exclusively stainless materials (stainless steel)
- Plasma/TIG gantry welding system
- Spinning/flanging processes
- Machine grinding (surface treatment)
- Gas-fired chamber furnace, max. 1100 °C
Products
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Cold and hot pressing (deep drawing of heads)Forming | – | 21,3 to 2.100 mm diameter | – | – | Boiler plate, Fine-grain structural steel, CrMo steel, Stainless steel, Duplex, Superduplex, Aluminium, Brass, Copper, Nickel alloys, Titanium, Zirconium, Tantalum |
| Spinning and flanging (cold and hot)Forming | – | up to 8.200 mm diameter | 30 tonnes unit weight | – | Boiler plate, Fine-grain structural steel, CrMo steel, Stainless steel, Duplex, Superduplex, Aluminium, Brass, Copper, Nickel alloys, Titanium, Zirconium, Tantalum |
| Heat treatment – normalizing (850-980°C)Heat treatment | – | – | 40 tonnes batch weight (charging system | – | Boiler plate, Fine-grain structural steel, CrMo steel, Stainless steel, Duplex, Superduplex, Nickel alloys, X8Ni9 |
| Heat treatment – tempering (650-750°C)Heat treatment | – | – | – | – | – |
| Stress-relief annealing / PWHT (595-720°C)Heat treatment | – | – | – | – | – |
| Solution annealing (1000-1180°C)Heat treatment | – | – | – | – | – |
| Soft annealingHeat treatment | – | – | – | – | – |
| Welding – plasma-TIG weldingJoining | – | – | – | – | Stainless steel, stainless materials |
| Welding – submerged arc welding (SAW)Joining | – | – | – | – | – |
| Welding – cladding welding (electroslag)Joining | – | – | – | – | clad material combinations |
| Welding – MIG / MAGJoining | – | – | – | – | – |
| Welding – electrodeJoining | – | – | – | – | – |
| Edge workingMachining | – | – | – | – | – |
| 3D flame cutting – plasma cuttingMachining | – | – | – | – | Steel, Stainless steel |
| 3D flame cutting – oxy-fuel cuttingMachining | – | – | – | – | Steel |
| Surface treatment – sandblastingSurface | – | – | – | – | – |
| Surface treatment – picklingSurface | – | – | – | – | – |
| Surface treatment – internal and external grinding (machine grinding)Surface | – | – | – | – | – |
| Manufacture of vessel heads, cones, special pressed parts, storage heads and welded constructionsForming | – | 21,3 mm to 13.500 mm diameter | – | Single-item production – Small series | Structural and stainless steels, Fine-grain structural steels, Duplex, Superduplex, Nickel alloys, Titanium, clad materials |
| Non-destructive testing: ultrasonic, X-ray, MT, PT, hardness testing on the component,Testing | – | – | – | – | – |
| Destructive testing: tensile test, impact bending test, bend testTesting | – | – | – | – | – |
8 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| Cold and hot flanging machine | In-house design (Gerhard König) | – | Heads up to 8.000 mm diameter | 2013 | Netphen |
| Hot spinning press | – | 1 | – | 2010 | Netphen |
| 3D robot cutting system (plasma/oxy-fuel) | – | 1 | Plasma up to 85 mm, oxy-fuel up to 200 mm sheet thickness | 2006 | Netphen |
| Chamber furnace (gas-fired, high-performance furnace) | – | – | 8.200 x 8.200 mm; max. temperature 1200°C (Netphen) / 1100°C (Haiger) | 2012 | Netphen |
| Water quenching tank / immersion tank | – | 1 | 500.000 litres | 2012 | Netphen |
| Charging system | – | 1 | 40 tonnes | – | Netphen |
| Plasma/TIG gantry welding system | – | – | – | – | Haiger |
| Spindle presses | – | – | – | 1933 | Netphen |
Additional services
Quality as a Consequence
All production and testing procedures are certified and approved for the respective industries. In our own materials testing laboratory, all common non-destructive testing methods (ultrasonic, X-ray, MT, PT, hardness testing, spectral analysis, ferrite content determination) as well as destructive tests (tensile, impact bending and bend tests) are carried out.
| Evidence | Netphen | Haiger |
|---|---|---|
| DIN EN ISO 9001 | ||
| DIN EN ISO 50001 | ||
| ASME PRT (Div. 1 and Div. 2) | ||
| AD-2000 HP 0 / W 0 | ||
| PED 2014/68/EU + ISO 3834-2 | ||
| DNV-CP-0350 (Pressed Parts) | ||
| NORSOK M-650 | ||
| Lloyd's Register / Bureau Veritas |
History
- 1930
Foundation of König + CO. GmbH by Adolf and Gustav König, Paul Nöh and Ernst Horn in Netphen; initially vessel manufacturing
- 1933
First spindle presses and flanging machines – focus on boiler heads
- 1961
Delivery programme extended to include heads, cones and hemispheres up to 3,2 m diameter
- 1963
Purchase of the Bödenpresswerk Hockenheim head pressing plant
- 1965
Expansion of painting / surface technology
- 1980–1990
New construction of halls 7, 8 and 9; expansion of the performance and product portfolio
- 1992
Quality management certified to ISO 9001
- 1995
Acquisition of the head pressing plant of the company Schmeck in Siegen
- 1999
Bernd and Jochen König take over the management
- 2006
Acquisition of a 3D robot cutting system
- 2010
World's first hot spinning press commissioned
- 2012
Replacement of the 8.200 × 8.200 mm chamber furnace including 500.000-litre water quenching tank
- 2013
Commissioning of a cold and hot flanging machine for heads up to 8.000 mm diameter
- 2017
New construction of the Haiger branch plant
- 2019
Expansion of production at the Haiger plant through integration of the Hockenheim plant
- 2025
Transfer of the company shares to the corporate group HBH Holdings Inc., Cincinnati, USA