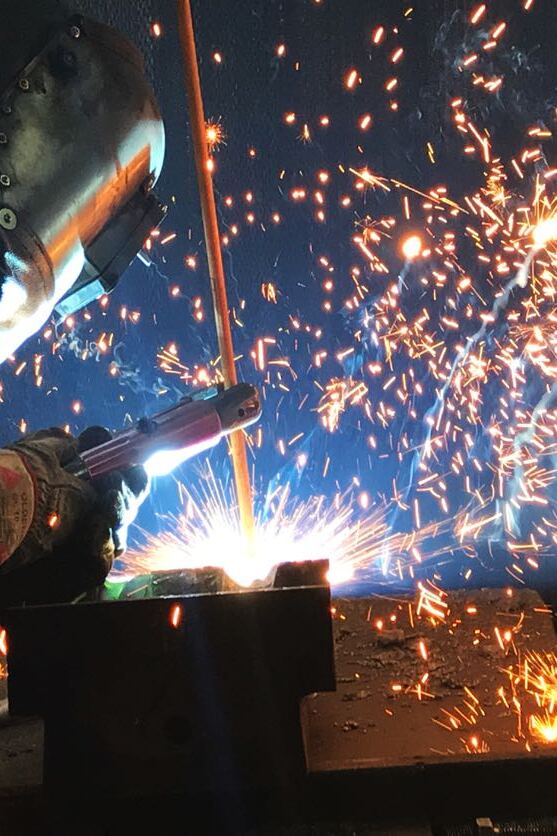
Welding-based repair of forging tools and heavy plant components up to 63 t
M+W Schweißtechnik GmbH
New on Amplifa
About M+W Schweißtechnik
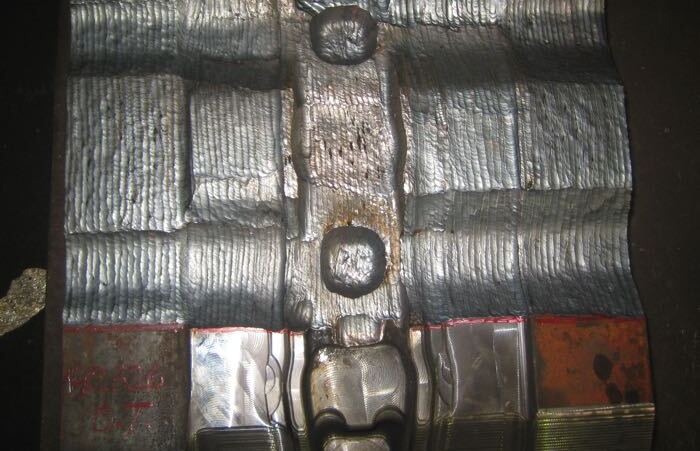
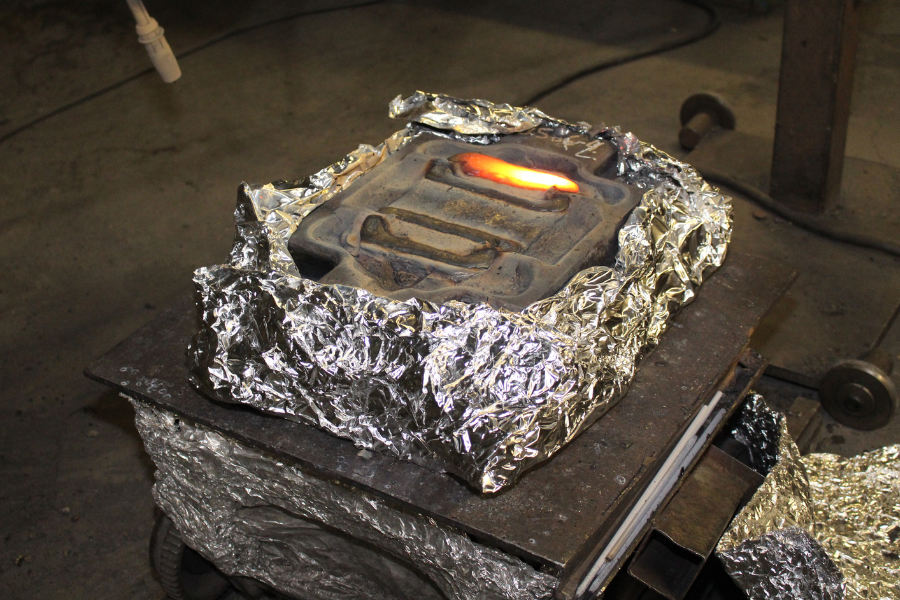
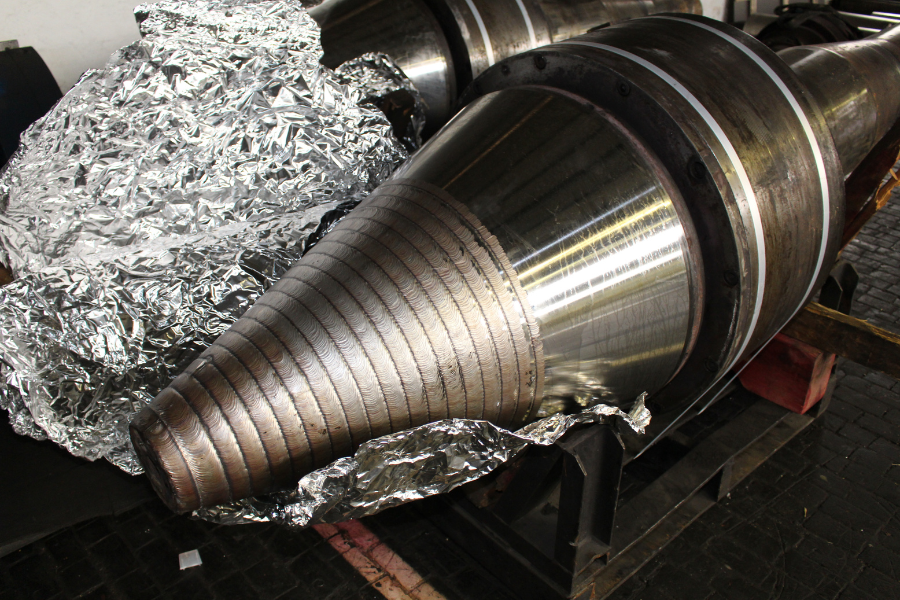
M+W Schweißtechnik GmbH specializes in the welding-based repair of heavy industrial components. Its team of 18 employees repairs worn forging tools by gouging out, build-up welding and filling the impressions, as well as plant components made of carbon steels and low- to high-alloy steels through cladding, overlay and joint welding. Processes used include SAW, MAG, MIG, TIG, open-arc and plasma powder welding, accompanied by preheating and stress-relief annealing in the company's own industrial furnaces. Strengths of up to 2,000 N/mm² are achieved on components weighing up to 63 tonnes each. Customers include forging shops, rolling mills, steel mills, plant manufacturers and heavy industry. If components cannot be transported, mobile on-site deployment is carried out with mobile heating equipment and welding units; project management including material procurement and machining is offered in conjunction with M+W Maschinen- und Werkzeugbau and M+W Intec repairs.
- Processes
- Repair of forging tools (gouging, build-up welding, filling of impressions), Repair of plant components by cladding, Overlay welding, Joint welding, SAW (submerged arc welding), MAG welding, MIG welding, TIG welding
- Materials
- Carbon steels, Low-alloy steels, High-alloy steels, Tool steels for forging tools
- Certificates
- ISO 9001
- Employees
- 18
- Industries
- Forging, Rolling mills, Steel mills, Plant manufacturers, Heavy industry
- 01
Damage assessment
- 02
Material selection and selection of the welding process
- 03
Preheating in industrial furnaces
- 04
Gouging / cladding / overlay or joint welding
- 05
Filling of impressions by welding
- 06
Stress-relief annealing
- 07
Ultrasonic and dye penetrant crack testing
- 08
Machining and reconditioning
Materials & Processes
Carbon steels
Repaired by cladding, overlay and joint welding.
Low-alloy steels
Used for plant components with an appropriately chosen filler material.
High-alloy steels
Repair of components for extreme loads in heavy industry.
Tool steels for forging tools
Repair of dies and impressions with strengths up to 2,000 N/mm².
Sites
Main site
DEWorkshop for welding technology, heat treatment and testing
- Part weight / size
- Components up to 63 t
- Materials
- Carbon steels, low- and high-alloy steels, tool steels
- Industrial furnaces for preheating and stress-relief annealing
- Ultrasonic testing equipment
Components
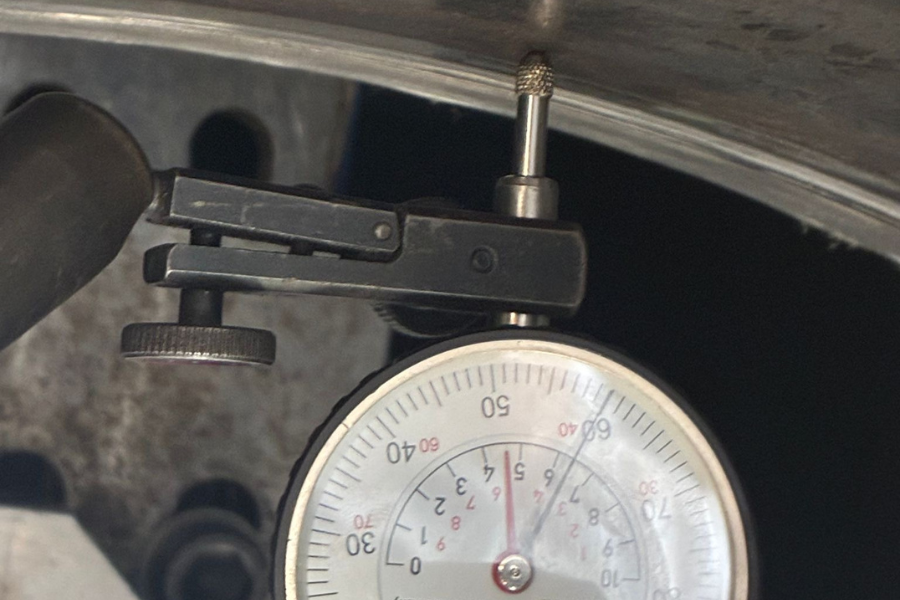
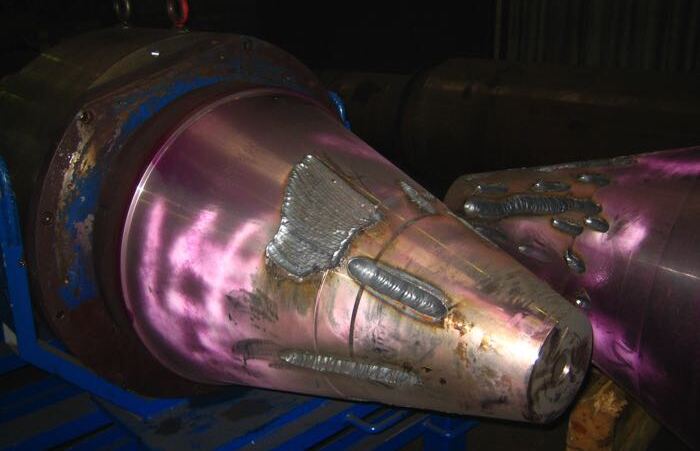
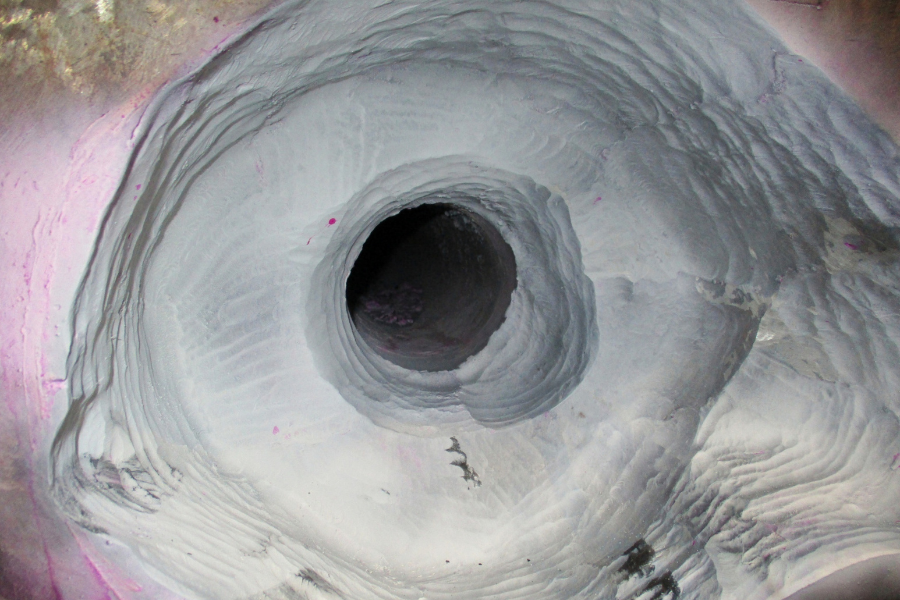
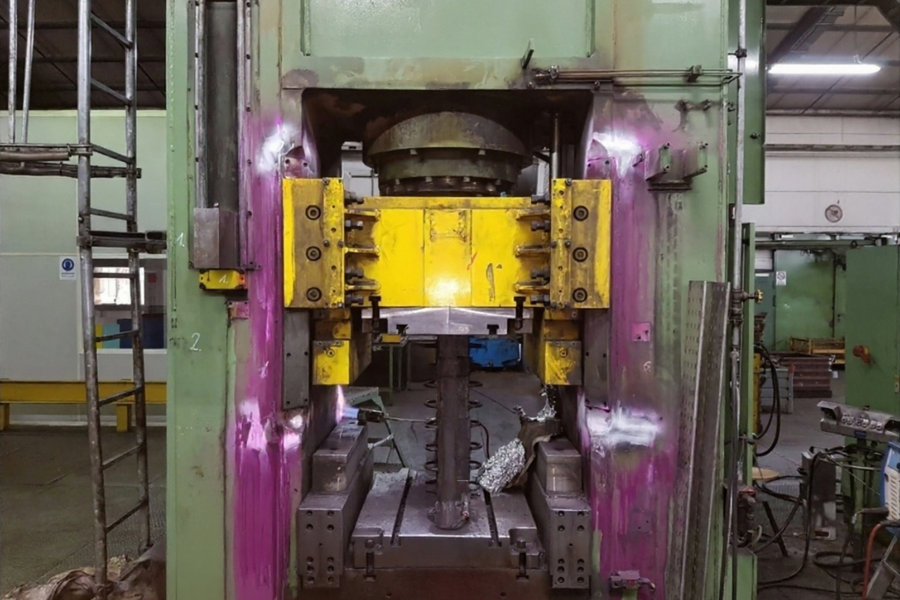
Inside the production
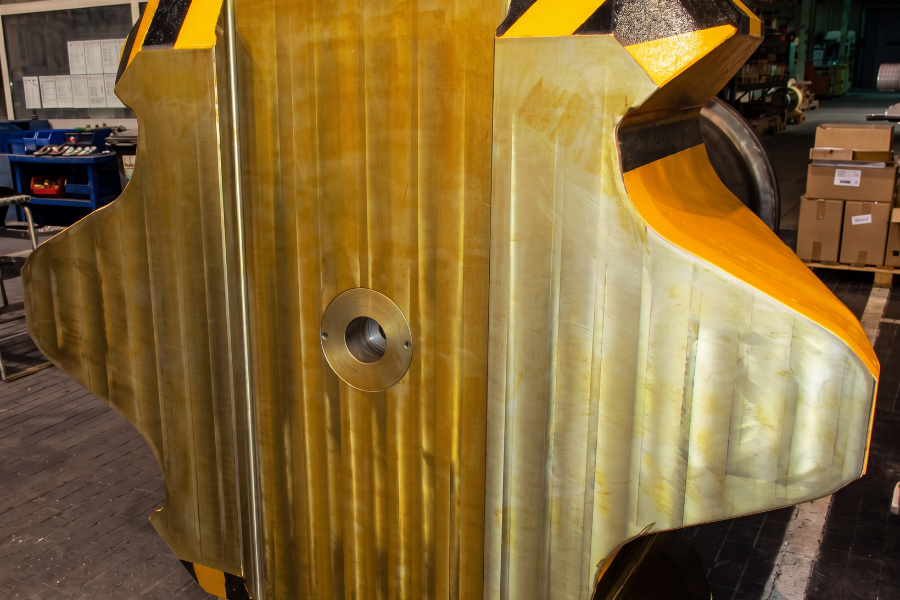
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Repair of forging tools (gouging, build-up welding, filling of impressions)Joining | – | – | – | – | Tool steels/forging tool steels |
| Repair of plant components by claddingJoining | – | – | 63 t | – | Carbon steels, low-alloy steels, high-alloy steels |
| Overlay weldingJoining | – | – | 63 t | – | Carbon steels, low-alloy steels, high-alloy steels |
| Joint weldingJoining | – | – | 63 t | – | Carbon steels, low-alloy steels, high-alloy steels |
| SAW (submerged arc welding)Joining | – | – | – | – | – |
| MAG weldingJoining | – | – | – | – | – |
| MIG weldingJoining | – | – | – | – | – |
| TIG weldingJoining | – | – | – | – | – |
| Open-arc weldingJoining | – | – | – | – | – |
| Plasma powder weldingJoining | – | – | – | – | – |
| Preheating and stress-relief annealing in industrial furnacesHeat treatment | – | – | – | – | – |
| Ultrasonic testingTesting | – | – | – | – | – |
| Dye penetrant crack testingTesting | – | – | – | – | – |
| Mobile on-site welding deployment with mobile heating equipment and welding unitsJoining | – | – | – | – | – |
3 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| Industrial furnaces (heat treatment) | – | – | – | – | – |
| Mobile heating equipment | – | – | – | – | on-site at the customer |
| Mobile welding units | – | – | – | – | on-site at the customer |
Additional services
Quality & Testing
Work is carried out in accordance with ISO 9001 with complete documentation of every work step. Ultrasonic and dye penetrant crack testing are performed in-house as standard.
| Evidence | Main site |
|---|---|
| ISO 9001 |