Sand casting of aluminium and copper alloys as one-offs, prototypes and small series up to 500 kg unit weight
Metallguss Brinschwitz GmbH
Rastatt (DE)New on Amplifa
About Metallguss Brinschwitz
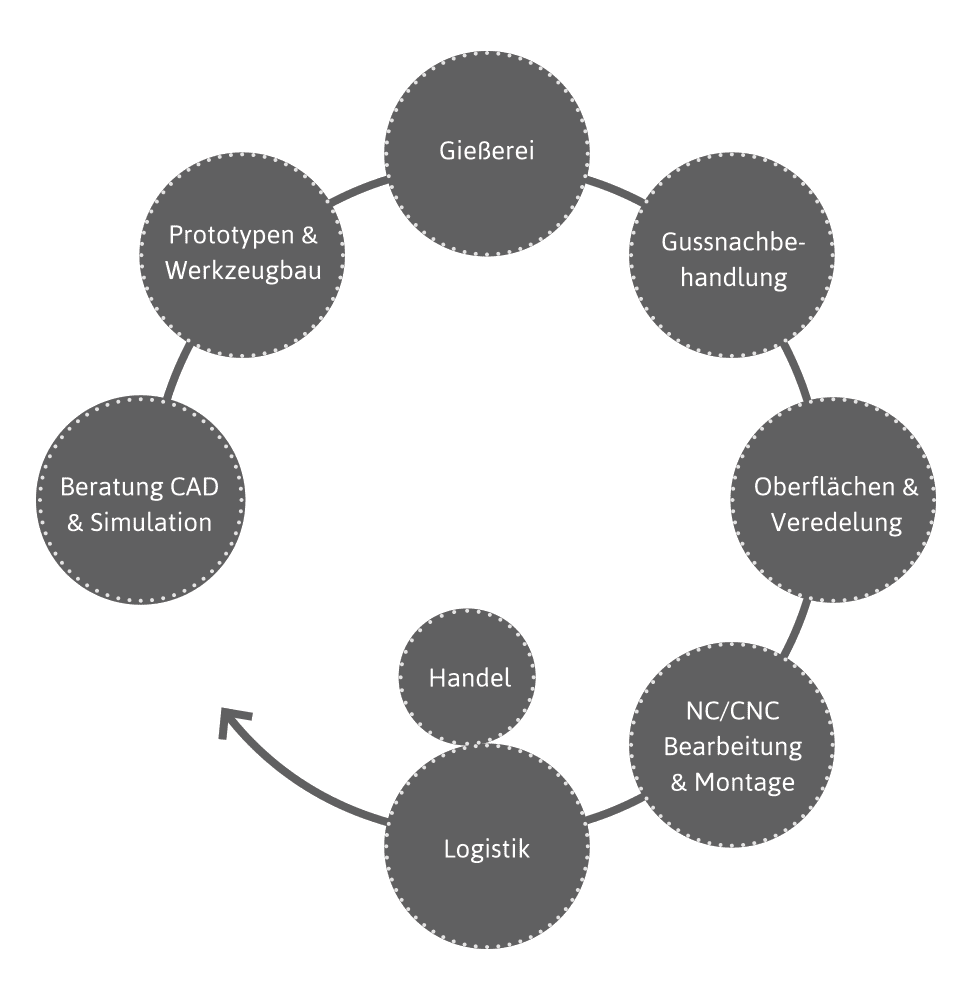
Metallguss Brinschwitz GmbH is a family-run foundry in Rastatt that has been producing castings in aluminium, pure copper and copper alloys such as red brass, bronze and special brass since 1920. The specialty is sand casting, performed using hand moulding and machine moulding as well as core block and cold-box moulding. With a melting operation up to 500 kg unit weight, castings with unit weights from approx. 25 grams to 250 kg (aluminium) or 200 kg (copper alloys) can be produced from more than 45 alloys. The range of services includes consulting, CAD and casting simulation, pattern and casting toolmaking, prototyping with printed sand moulds, post-casting treatment, assembly of ready-to-install castings and logistics. CNC machining and surface finishing are carried out via a partner network, as is the procurement of grey cast iron GG, spheroidal graphite cast iron GGG and steel castings GS. Customer industries include the electrical industry, mechanical engineering, valve and fittings manufacturing, pump manufacturing, shipbuilding, chemicals, the food industry and paper machinery. The team of around 30 mainly produces industrial one-offs, prototypes and small series.
- Site
- Rastatt
- Processes
- Sand casting (hand moulding), Sand casting (machine moulding, strip and turnover moulding machines), Core block and cold-box resin moulding for prototypes and special, individual parts, Core making (core making machines and manual core production in cold box and cold-box resin), Melting operation (heavy metals and aluminium), Prototyping with printed sand moulds, Prototypes from the original tool, CAD, simulation and casting system design
- Materials
- Red brass CuSn5Zn5Pb5-C (Rg5), Red brass CuSn7Zn4Pb7-C (Rg7), Red brass CuSn10Zn (Rg10), Bronze CuSn10-C (Gbz10), Bronze CuSn12-C (Gbz12), Bronze CuSn12Ni2-C (Gbz12Ni), Bronze CuSn11Pb2-C (Gbz12Pb), Aluminium bronze CuAl10Fe5Ni5-C (Ni-Al Bz)
- Certificates
- ISO 9001:2015
- Founded
- 1920
- Employees
- approx. 30
- Industries
- Electrical industry/Electronics, Mechanical engineering, Valve and fittings manufacturing, Pump manufacturing, Shipbuilding, Chemical/Petrochemical industry
- 01
Consulting on planning, material requirements and manufacturing processes
- 02
CAD, simulation and casting system design
- 03
Pattern making & casting toolmaking
- 04
Prototyping with printed sand moulds or from the original tool
- 05
Melting operation
- 06
Hand and machine moulding as well as core making (cold box/cold-box resin)
- 07
Casting and core removal
- 08
Post-casting treatment
- 09
Optical and tactile measurement, X-ray and leak testing
- 10
Surface finishing, CNC machining and assembly (with partners)
- 11
Logistics
Location
Rastatt
DEFoundry, production and administration
- Part weight / size
- Al up to 250 kg, Cu alloys up to 200 kg, melting operation
- Lot size
- One-offs to small series
- Materials
- Aluminium, pure copper, red brass, bronze, special brass
- Hand moulding with automatic sand preparation (max. flask size 3000 x 3000 mm)
- Strip and turnover moulding machines (max. 1200 x 800 mm)
- Core making machines, cold box/cold-box resin, up to max. 50 litres
- Induction furnace system (2021)
- Core breaker 605 / core removal system with F+K knock-out unit
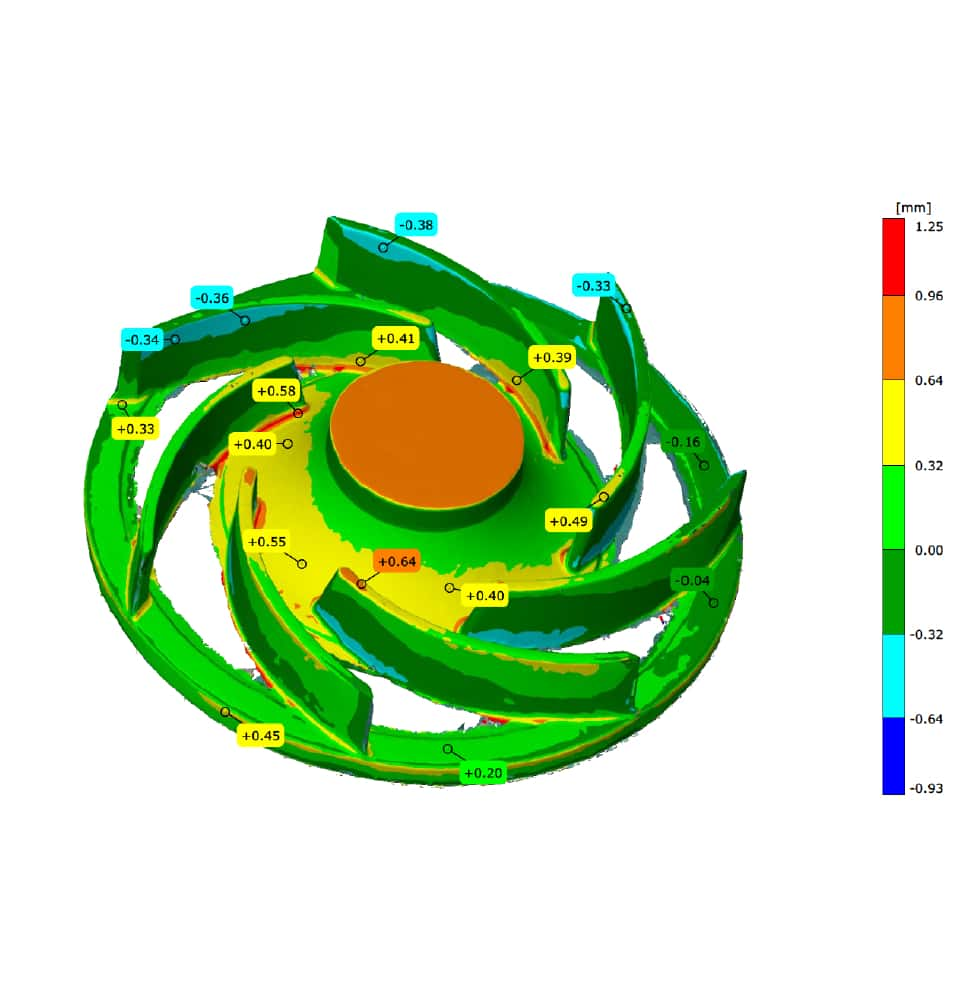
- FARO measuring arm with optical scanner head
- X-ray system
- Coordinate measuring machine
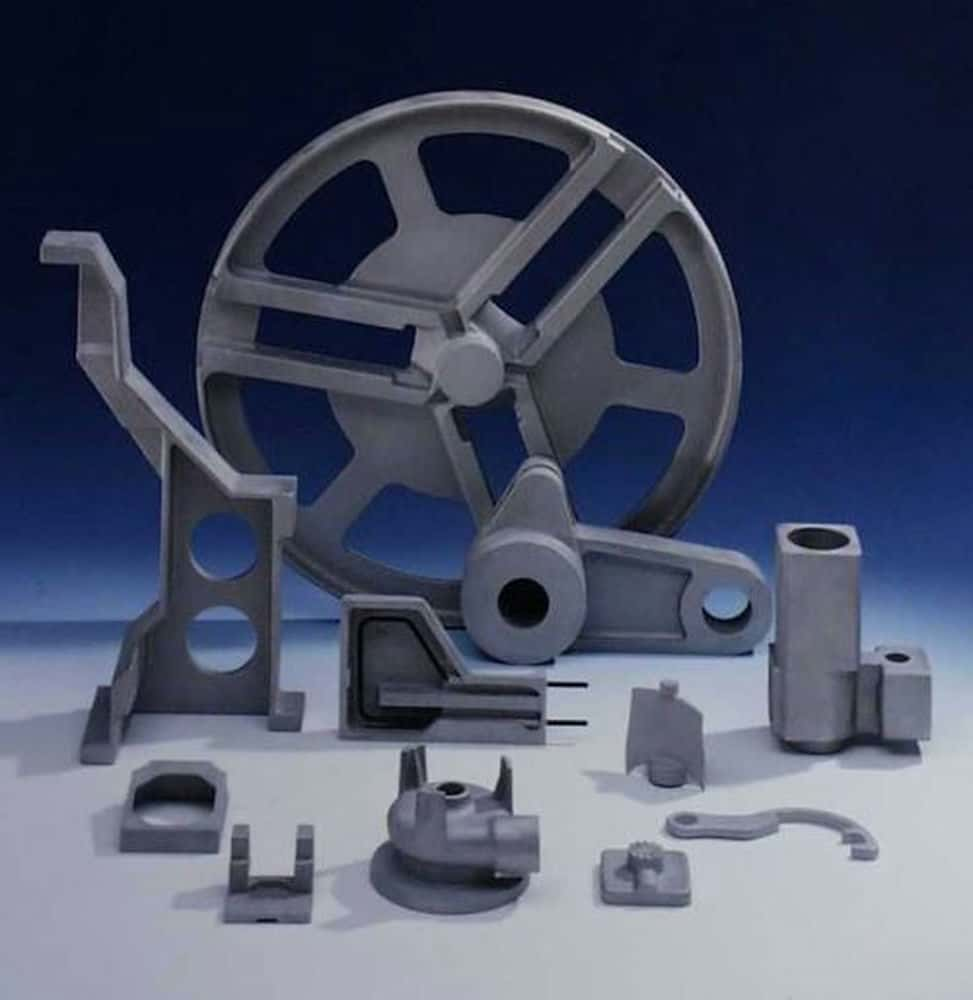
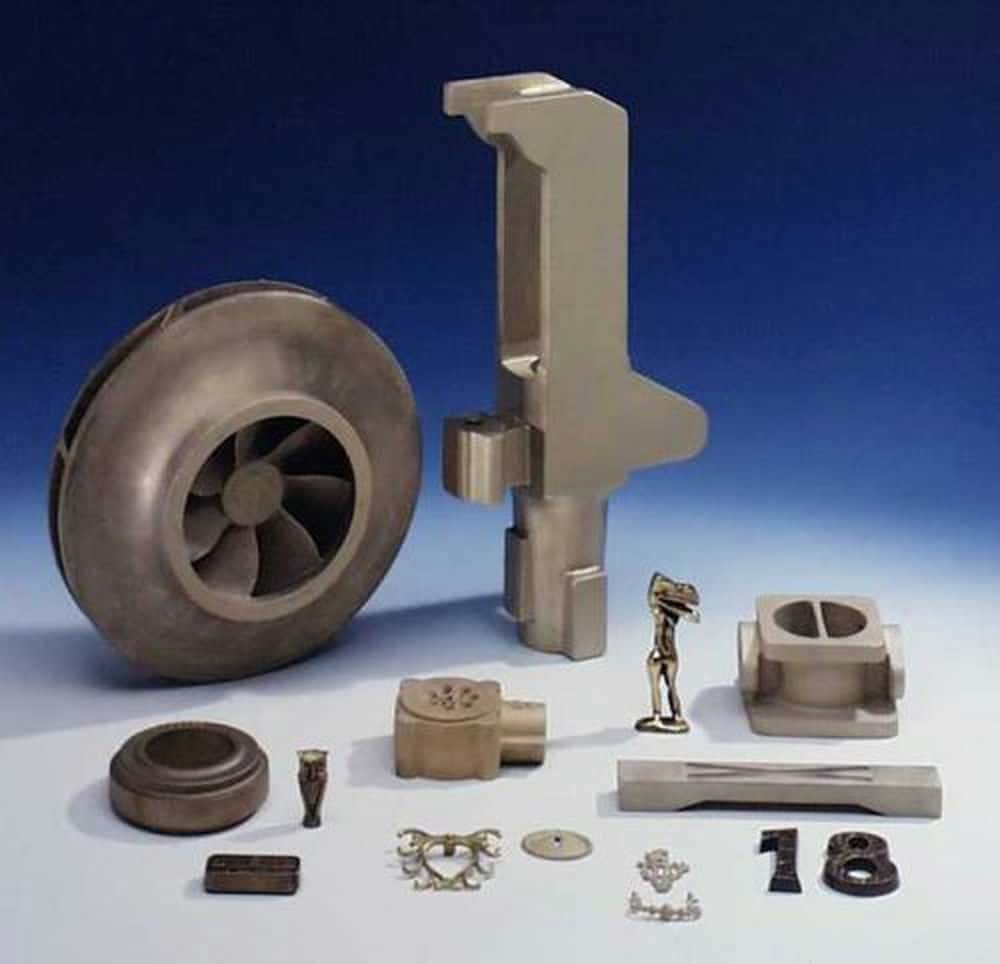
Components
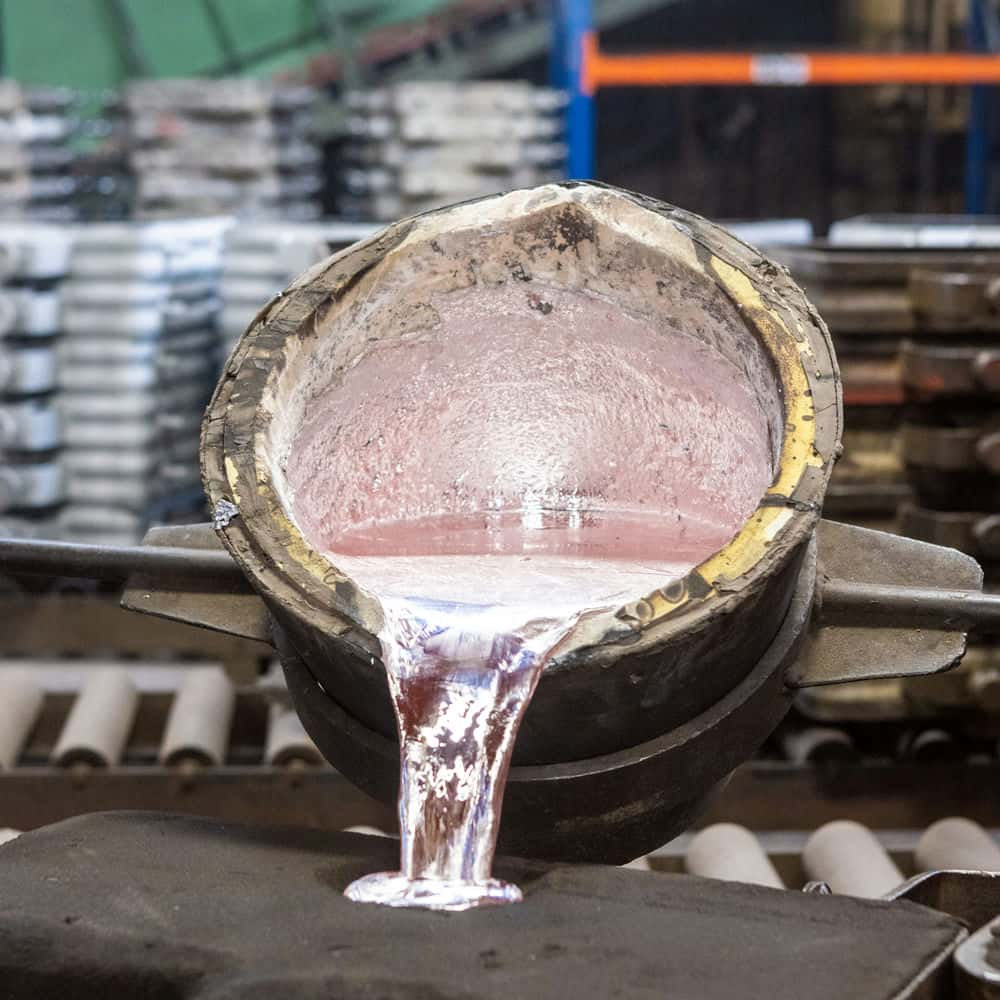
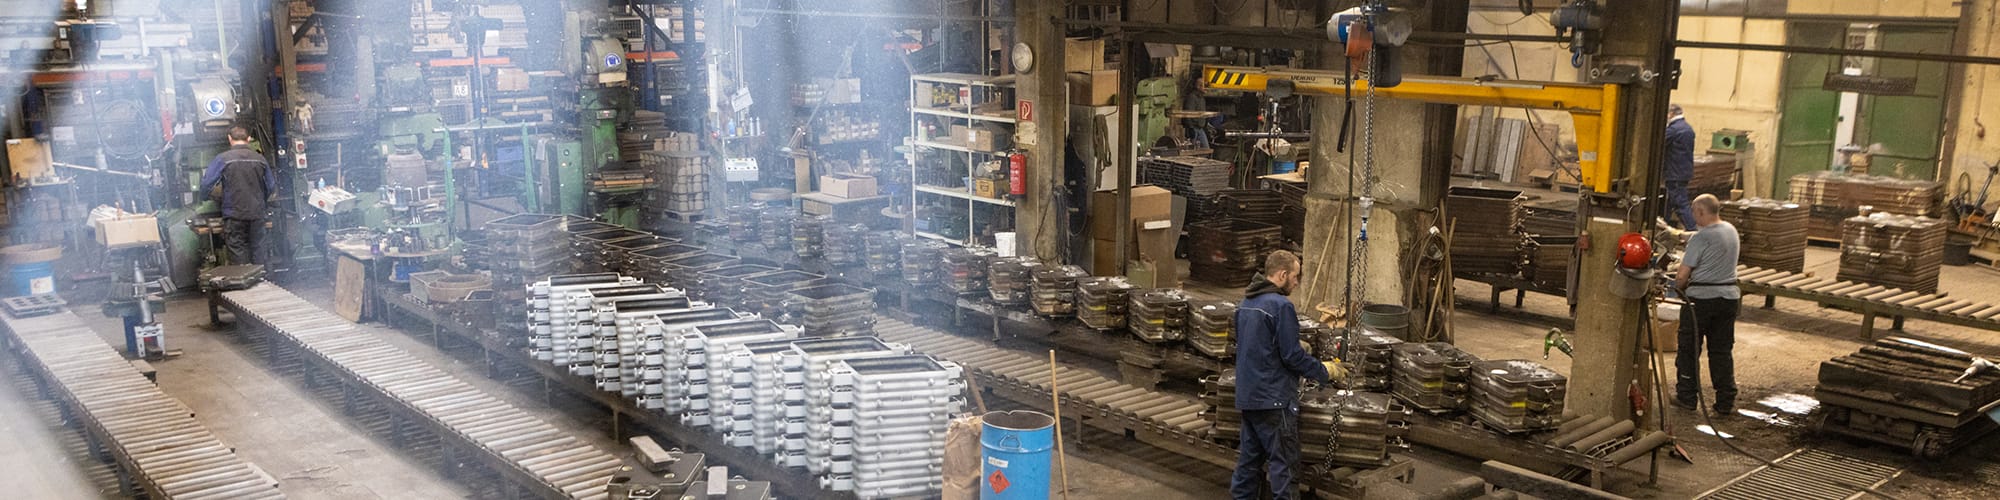
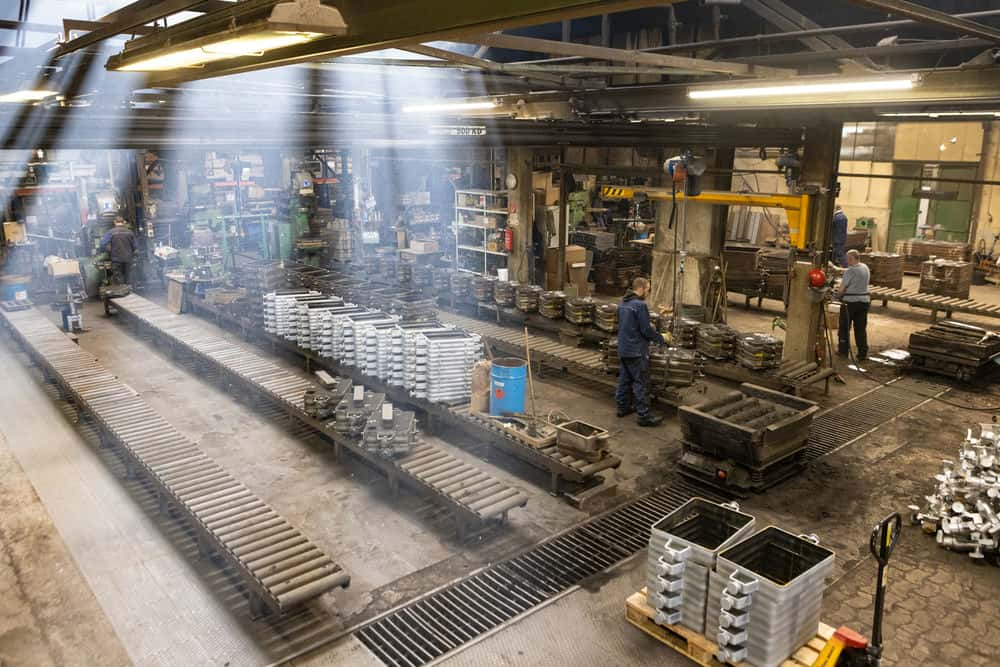
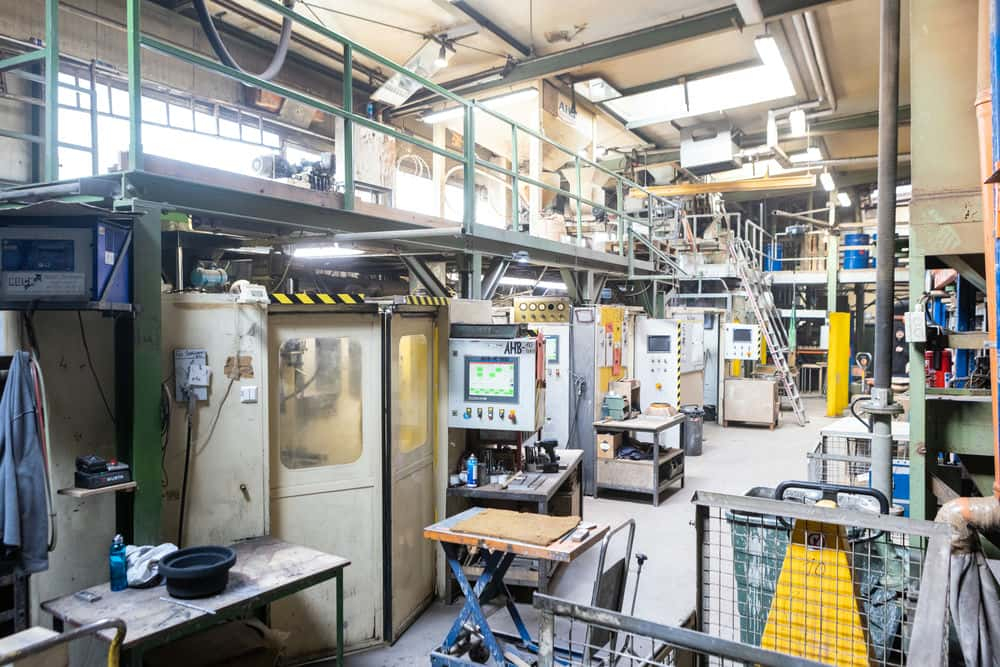
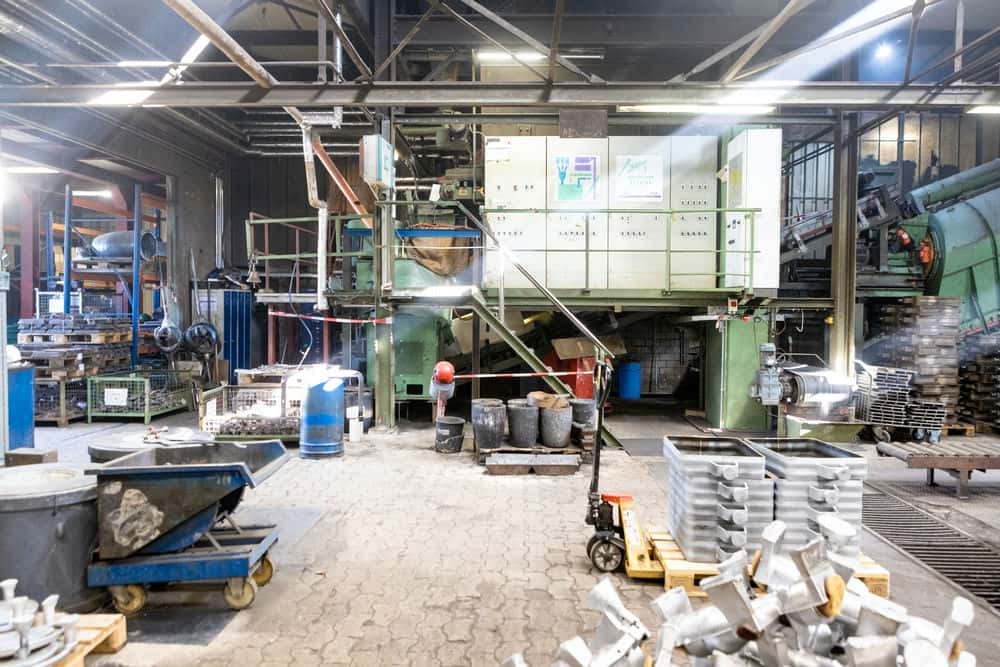
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Sand casting (hand moulding)Casting | – | 3000 mm × 3000 mm | approx. 25 grams – 250 kg | One-offs – Small series | Aluminium, Copper alloys, Pure copper |
| Sand casting (machine moulding, strip and turnover moulding machines)Casting | – | 1200 mm × 800 mm | 250 kg | – | Aluminium, Copper alloys |
| Core block and cold-box resin moulding for prototypes and special, individual partsCasting | – | – | – | – | Aluminium, Copper alloys |
| Core making (core making machines and manual core production in cold box and cold-box resin)Casting | – | – | – | – | – |
| Melting operation (heavy metals and aluminium)Casting | – | – | a few grams – 500 kg | – | Aluminium, Heavy metals, Copper alloys |
| Prototyping with printed sand mouldsAdditive | – | – | – | – | Aluminium, Copper alloys |
| Prototypes from the original toolCasting | – | – | – | – | Aluminium, Copper alloys |
| CAD, simulation and casting system designEngineering | – | – | – | – | – |
| CNC machining (via network/partners)Machining | – | – | – | – | – |
| Surface finishing and post-processing stagesSurface | – | – | – | – | – |
| Optical measurement (FARO measuring arm with optical scanner head)Testing | – | – | – | – | – |
| X-ray testing of castingsTesting | – | – | – | – | – |
| Pressure tightness testing (air under water or differential pressure), tactile measurement,Testing | – | – | – | – | – |
| Procurement of GG, GGG and GS via partnersCasting | – | – | – | – | GG, GGG, GS |
8 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| Hand moulding with automatic sand preparation | – | – | max. flask size 3000 x 3000 mm | – | Rastatt |
| Strip and turnover moulding machines | – | – | max. flask size 1200 x 800 mm | – | Rastatt |
| Core making machines (cold box and cold-box resin) | – | – | up to max. 50 litres | – | Rastatt |
| Induction furnace system | – | – | – | 2021 | Rastatt |
| FARO measuring arm with optical scanner head | FARO | – | – | – | Rastatt |
| X-ray system for casting inspection | – | – | – | – | Rastatt |
| Coordinate measuring machine (tactile measurement) | – | – | – | – | Rastatt |
| Core breaker 605 / core removal system for castings with F+K knock-out unit | F+K Core breaker 605 | – | – | – | Rastatt |
Additional services
Quality
Quality assurance includes optical measurement with a FARO measuring arm with optical scanner head, X-ray testing for internal casting defects, tactile measurement on a coordinate measuring machine, pressure tightness and helium pressure testing, spectral analysis, hardness and crack testing as well as microstructure verification. Upon customer request, certificates according to DIN EN 10204:2005-01 are issued.
| Evidence | Rastatt |
|---|---|
| ISO 9001:2015 |
History
- 1920
Company founded by Josef Hettel
- 1961
Continuous development of the foundry under Werner Hettel-Schlumberger; construction of the hand moulding hall
- 1974
Establishment of the machine moulding shop
- 1998
Handover and renaming of Hettel Metallguss GmbH to Metallguss Brinschwitz GmbH under CEO Frank Brinschwitz
- 2005
Expansion of the foundry and commissioning of the core making hall
- 2007
Expansion of the moulding sand preparation
- 2009
Addition of the North warehouse
- 2021
Succession and takeover by CEO Ralf Brinschwitz; modernisation of the foundry with new core making centres and a new induction furnace system