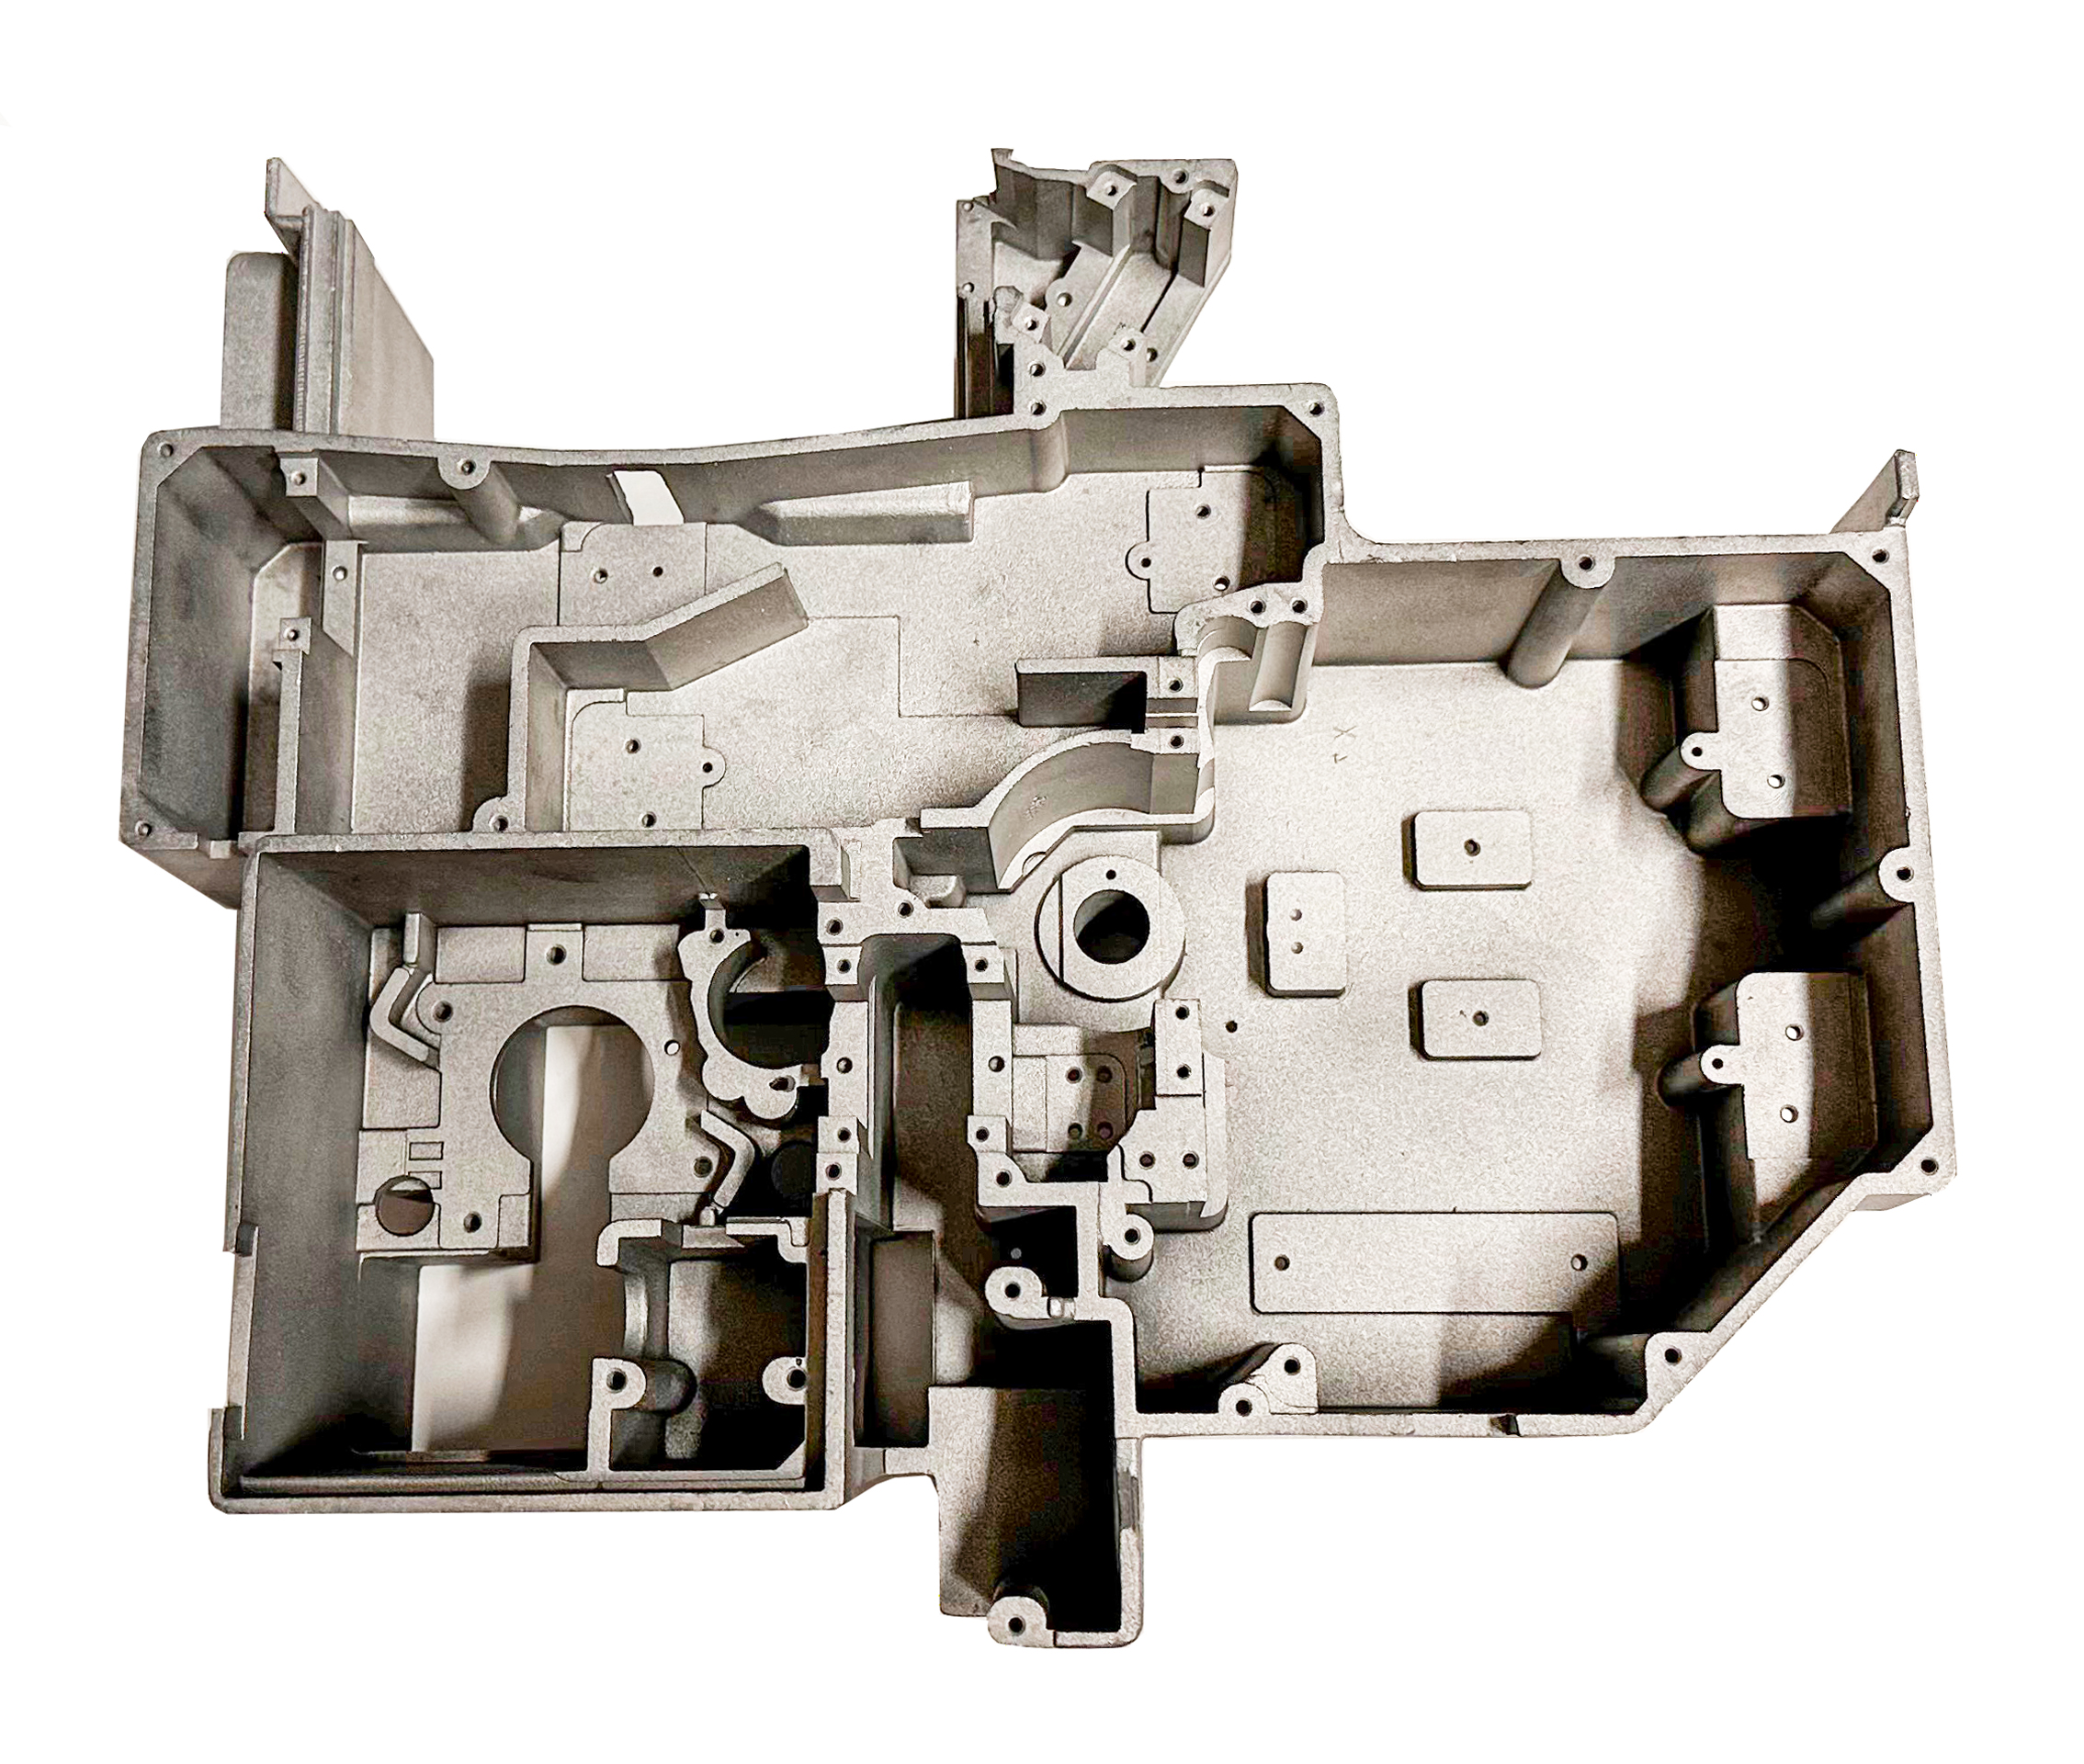
Permanent mould and sand casting in aluminium and copper-based alloys – from semi-finished products to ready-to-install CNC-machined components
Pöschel GmbH Metallguss
Solingen (Holbeinstraße 29) · Leichlingen (foundry hall H 08)New on Amplifa
The Core of the Matter
Pöschel GmbH Metallguss, founded in 1994 and now run by the second generation, is a specialist in the design, development and production of demanding castings in aluminium and copper-based alloys. At the Solingen site, permanent mould castings are produced on 800 m² of production floor space – machine-cast on gravity die casting machines or cast by hand, in each case with or without sand cores – as well as sand castings for complex geometries with bores and intersecting contours. Using steel and sand cores, thin-walled, pore- and shrinkage-free mouldings are also produced reproducibly. The service spectrum includes materials and design consulting, solidification simulation and finite element analysis, prototyping, heat treatment (T1, T5, T6, T7 per DIN EN 1706), ready-to-install CNC machining, and powder and KTL coating. Customers come from laboratory technology, medical technology, energy technology, mechanical engineering, electrical engineering and mining; lot sizes range from one-off parts to medium series of around 10,000 pieces. The quality management system is certified to DIN EN ISO 9001:2015.
- Site
- Solingen
- Processes
- Permanent mould casting (machine casting with/without sand core), Permanent mould casting (hand casting with/without sand core), Sand casting, CNC machining (machining, ready-to-install: thread tapping, turning of bearing seats, rivet pins, Tempering/heat treatment T1 per DIN EN 1706 (controlled cooling, naturally aged), Tempering/heat treatment T5 per DIN EN 1706 (artificially aged without overageing), Tempering/heat treatment T6 per DIN EN 1706 (solution annealing, fully artificially aged), Tempering/heat treatment T7 per DIN EN 1706 (solution annealing and over-ageing for maximum
- Materials
- AlSi12 (230), AlSi12, AlSi0,5Mg, AlSi8Cu3, Copper-based alloys, Brass (cast-in bushing), Permanent mould casting (machine and hand casting), Sand casting
- Certificates
- DIN EN ISO 9001:2015, ISO 9001
- Founded
- 1994
- Employees
- 10
- Industries
- Laboratory technology, Medical technology, Energy technology, Mechanical engineering, Electrical engineering, Mining
- 01
Feasibility analysis
- 02
Solidification simulation and finite element analysis
- 03
Design consulting / casting-optimised design
- 04
Prototyping / first samples
- 05
Permanent mould casting (machine or hand casting, with/without sand core) or
- 06
Heat treatment / tempering (T1–T7 per DIN EN 1706)
- 07
CNC machining up to ready-to-install
- 08
Powder or KTL coating
- 09
Packaging and delivery
Materials and Processes
AlSi12 (230)
Good castability and tightness for thin-walled, complex housings, e.g. in laboratory and medical technology.
AlSi0,5Mg
High-conductivity alloy for contact holders in energy technology, with targeted heat treatment to increase electrical conductivity.
AlSi8Cu3
Strength-oriented alloy for pressure-tight, shrinkage-free flange parts in mechanical engineering.
Copper-based alloys
For components with special requirements for conductivity and heat transfer.
Brass (cast-in bushing)
Cast-in bushings integrate bearing functions directly into the aluminium component.
Permanent mould casting (machine and hand casting)
With or without sand core, for pore- and shrinkage-free parts from one-offs to medium series.
Sand casting
For complex geometries and contours with bores via steel and sand cores.
Heat treatment T1/T5/T6/T7 (DIN EN 1706)
Tempering by solution annealing, quenching and artificial ageing; T7 for maximum electrical conductivity.
CNC machining
Dimensionally accurate, ready-to-install production incl. thread tapping, turning of bearing seats and attaching rivet pins.
Powder coating
Protective surface coating of the castings.
KTL coating
Cathodic dip painting for uniform corrosion protection.
Locations
Solingen
DEHeadquarters with foundry, CNC machining and coating (800 m² production floor space)
- Part weight / size
- Components from approx. 0.75 kg to approx. 3.85 kg, wall
- Lot size
- One-off to approx. 10,000 pieces
- Materials
- AlSi12, AlSi0,5Mg, AlSi8Cu3, copper-based alloys, brass
- Gravity die casting machine
- 1 melting furnace of 600 kg
- 5 melting furnaces of 300 kg
- CNC-controlled machining machines
Reference Components
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Permanent mould casting (machine casting with/without sand core)Casting | – | – | – | One-off – approx. 10,000 pieces | AlSi12, AlSi12(230), AlSi0,5Mg, AlSi8Cu3, copper-based alloys |
| Permanent mould casting (hand casting with/without sand core)Casting | – | – | – | One-off – approx. 10,000 pieces | AlSi12, AlSi12(230), AlSi0,5Mg, AlSi8Cu3, copper-based alloys |
| Sand castingCasting | – | – | – | – | Aluminium alloys, copper-based alloys |
| CNC machining (machining, ready-to-install: thread tapping, turning of bearing seats, rivet pinsMachining | – | – | – | – | AlSi12, AlSi0,5Mg, AlSi8Cu3, copper-based alloys |
| Tempering/heat treatment T1 per DIN EN 1706 (controlled cooling, naturally aged)Heat treatment | – | – | – | – | Aluminium alloys |
| Tempering/heat treatment T5 per DIN EN 1706 (artificially aged without overageing)Heat treatment | – | – | – | – | Aluminium alloys |
| Tempering/heat treatment T6 per DIN EN 1706 (solution annealing, fully artificially aged)Heat treatment | – | – | – | – | Aluminium alloys |
| Tempering/heat treatment T7 per DIN EN 1706 (solution annealing and over-ageing for maximumHeat treatment | – | – | – | – | Aluminium alloys |
| Powder coatingSurface | – | – | – | – | Aluminium alloys |
| KTL coatingSurface | – | – | – | – | Aluminium alloys |
| Design consulting / casting-optimised shape designEngineering | – | – | – | – | – |
| Solidification simulation and finite element analysisEngineering | – | – | – | – | – |
| Prototyping (models and first samples)Engineering | – | – | – | – | – |
4 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| Gravity die casting machine | – | – | – | – | Solingen |
| Melting furnace | – | 1 | 600 kg | – | Solingen |
| Melting furnace | – | 5 | 300 kg | – | Solingen |
| CNC-controlled machining machines | – | – | – | – | Solingen |
Additional services
Reference customers
Quality
The quality management system is certified to DIN EN ISO 9001:2015 and is continuously developed further through independent audits. Upon request, the company delivers works certificates 2.2 or acceptance inspection certificates 3.1 B per DIN EN 10204.
| Evidence | Solingen |
|---|---|
| ISO 9001 |
History
- 1994
Founded as a specialist in the design, development and production of demanding castings; today a family business run by the second generation