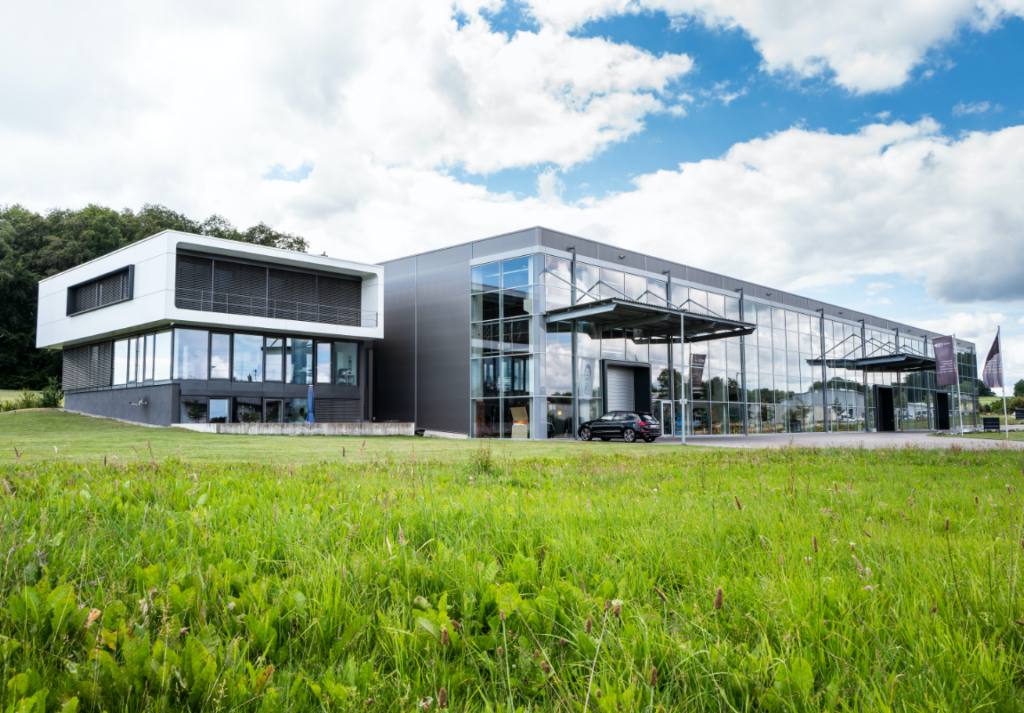
Heat treatment shop for all heat treatment processes – from pulse plasma nitriding to vacuum hardening.
Pro Ion Härtetechnik GmbH
Fronreute-Baienbach (DE)New on Amplifa
Hardening processes for the metalworking industry
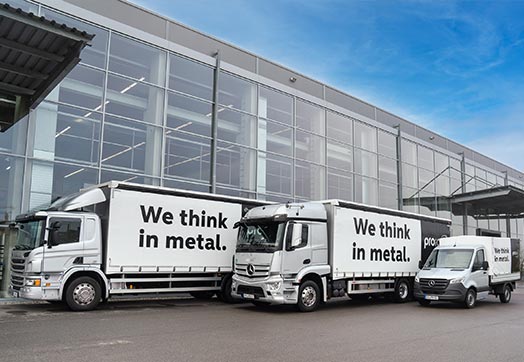
Pro Ion Härtetechnik GmbH is an independent, medium-sized company based in Fronreute-Baienbach near Ravensburg and, as a service provider, offers the full range of heat treatment for the metalworking industry. The starting point in 1998 was pulse plasma nitriding; today the portfolio includes gas nitrocarburizing, case hardening, carbonitriding, carburizing, vacuum hardening, flame hardening, protective gas hardening, tempering, and annealing processes under atmosphere, protective gas or vacuum. On 3,000 m² of production space, components from a few grams to 25 t are processed, from single parts to series production. The material range comprises steels, stainless steels, cast iron and sintered steel; treated components are used in automotive engineering, aerospace, mechanical and tool engineering, hydraulics, drive technology, gear and pump manufacturing as well as environmental technology and plant engineering. Heat treatment is complemented by an in-house materials testing laboratory, component cleaning, plant engineering, and the company's own weekly delivery service up to 200 km.
- Site
- Fronreute-Baienbach
- Processes
- Pulse plasma nitriding, Gas nitriding / gas nitrocarburizing, Case hardening, Carbonitriding, Vacuum hardening, Flame hardening, Annealing under atmosphere / protective gas / vacuum, Protective gas hardening
- Materials
- C10, 16MnCr5, 18CrNi8, 20MoCr4, 25MoCr4, 1.2379, 1.2080, 1.2436
- Founded
- 1998
- Industries
- Automotive engineering, Aerospace industry, Mechanical engineering, Environmental technology, Tool engineering, Mould making
- 01
Technical consulting / field service
- 02
FMEA (Failure Mode and Effects Analysis)
- 03
Collection service
- 04
Component cleaning
- 05
Finishing using various hardening processes
- 06
Component testing and documentation
- 07
Metallurgical and metallographic examinations
- 08
Delivery service
Materials and hardening processes
Pulse plasma nitriding
Thermochemical surface hardening without microstructural transformation at 380–580 °C, emission-free, for steel, cast iron, sintered steel and stainless steel.
Gas nitriding / gas nitrocarburizing
Low-distortion surface layer treatment at 510–580 °C for unalloyed and medium-alloy steels, also possible as bulk material.
Case hardening
Carburizing and quenching of low-carbon steels such as C10 or 16MnCr5 to a case depth of approx. 2 mm for a hard surface layer with a tough core.
Carbonitriding
Case hardening with additional nitrogen, case depths 0.1–0.8 mm, preferably for gear and machine engineering.
Vacuum hardening
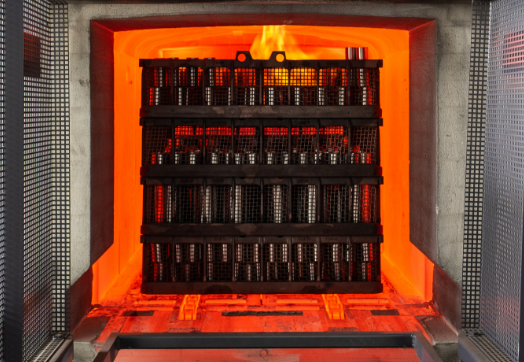
Scale-free hardening of air-hardenable medium- and high-alloy steels with nitrogen quenching up to 1,180 °C.
Flame hardening
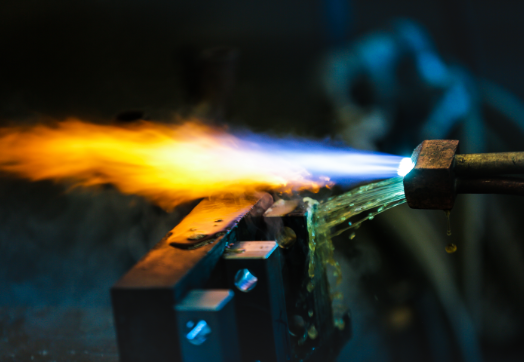
Local surface layer hardening up to 10 mm depth on steels with a carbon content above 0.4%, also partial.
Tempering
Hardening and tempering of temperable steels such as 42CrMo4 for the combination of strength and toughness.
Protective gas hardening
Through and surface hardening of steels from 0.2% carbon content as well as cast iron under protective gas.
Carburizing
Increase of the carbon content in the surface layer of unalloyed and low-alloy steels to 0.25–0.9% at 850–950 °C.
Annealing (atmosphere/protective gas/vacuum)
Stress-relief annealing, soft annealing and normalizing for microstructure improvement and stress reduction.
Site
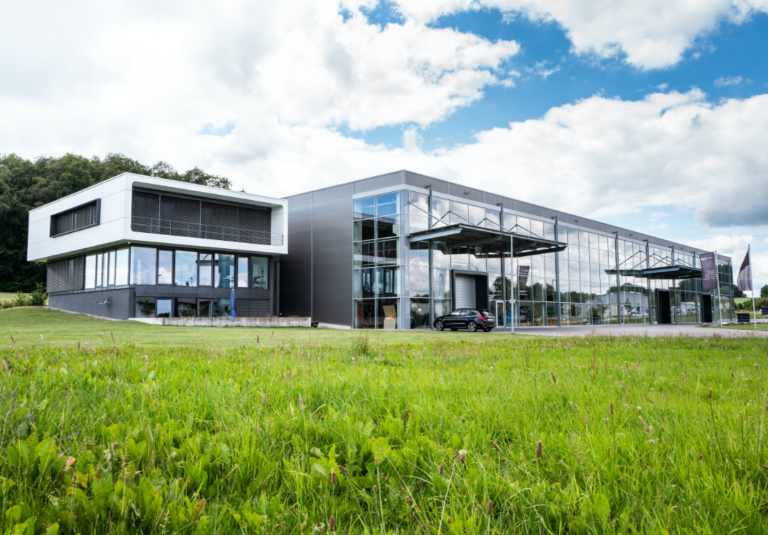
Fronreute-Baienbach
DEProduction / company headquarters
- Part weight / size
- a few grams to 25 t
- Lot size
- Single parts to series, bulk material for gas nitrocarburizing
- Materials
- Steel, stainless steel, cast iron, sintered steel
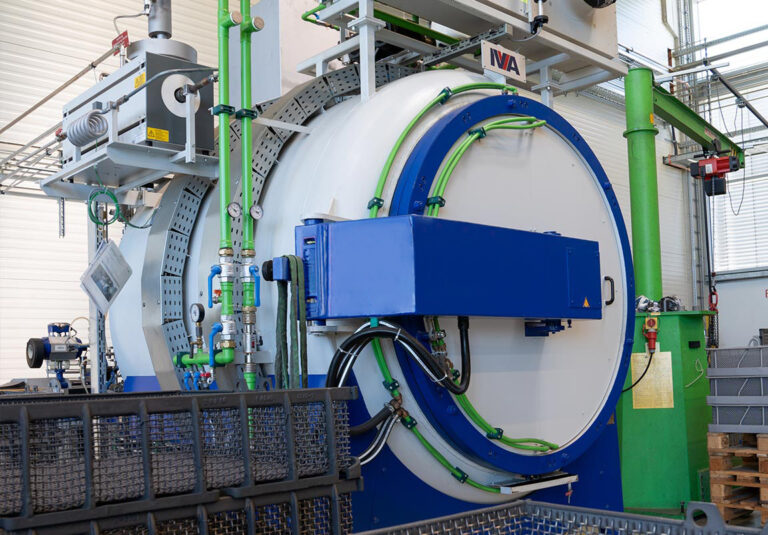
- Fully automatic hardening system with loading stations (Ipsen)
- Gas nitriding system
- Pulse plasma nitriding systems (vacuum chambers)
- Vacuum hardening furnaces
- Annealing furnaces
Heat-treated components
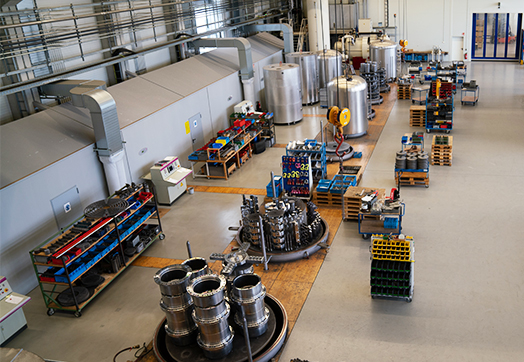
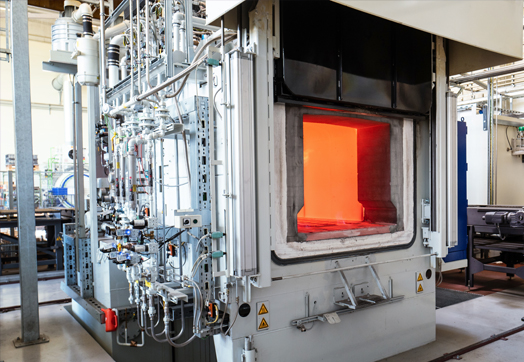
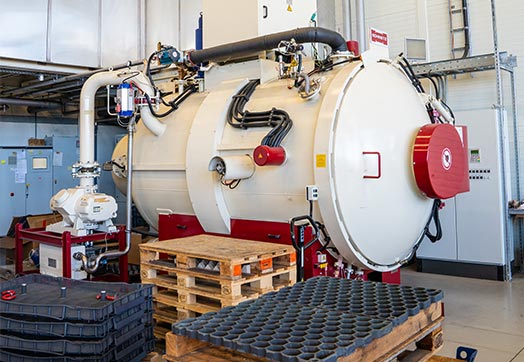
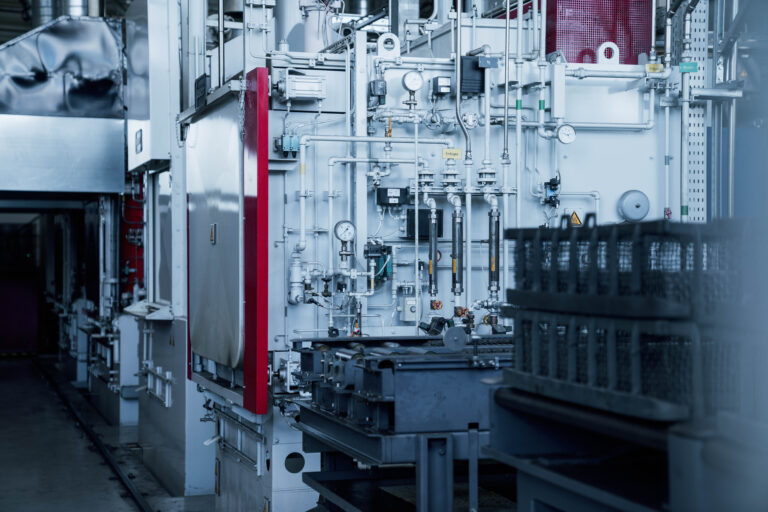
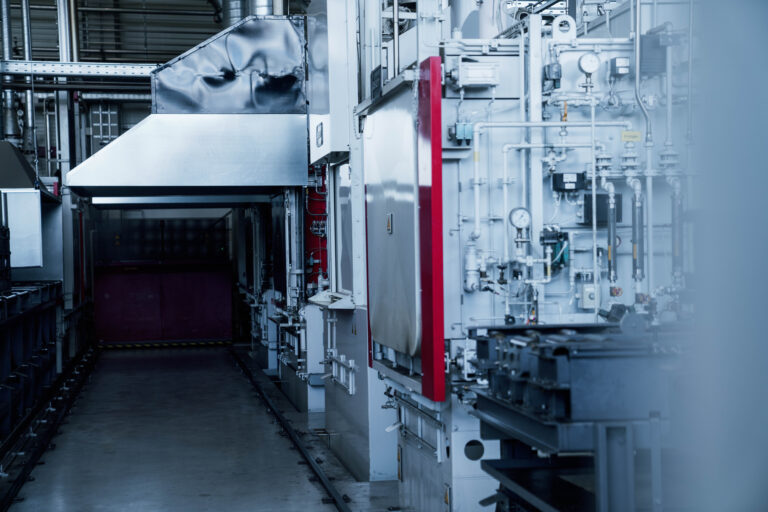
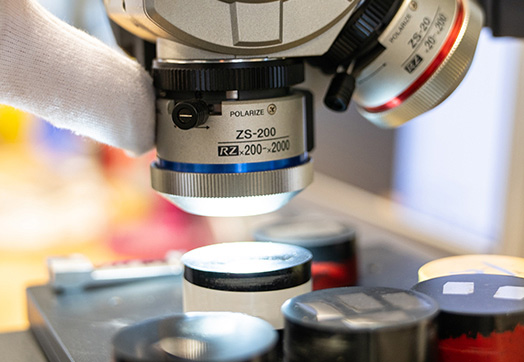
Inside the production
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Pulse plasma nitridingHeat treatment | – | 5,200 mm × Ø 2,600 mm | a few grams – 25 t | – | Steel, Cast iron, Sintered steel, Stainless steel |
| Gas nitriding / gas nitrocarburizingHeat treatment | – | 1,200 mm × 800 mm × 800 mm | 1.2 t | Bulk material possible | unalloyed steels, medium-alloy steels |
| Case hardeningHeat treatment | – | 1,200 mm × 800 mm × 800 mm | 2 t | – | C10, 16MnCr5, 18CrNi8, 20MoCr4, 25MoCr4, free-cutting steels |
| CarbonitridingHeat treatment | – | 1,200 mm × 800 mm × 800 mm | 2 t | – | C10, 16MnCr5, 18CrNi8, 20MoCr4, 25MoCr4, unalloyed structural steels, free-cutting steels |
| Vacuum hardeningHeat treatment | – | 1,200 mm × 800 mm × 700 mm | 800 kg | – | 1.2379, 1.2080, 1.2436, 1.4034, 1.4112, 1.4122, 1.4021, 1.2083, 1.3244, 1.3343, 1.2767, 1.2343 |
| Flame hardeningHeat treatment | – | 2,500 mm × Ø 340 mm | 3 t | – | C45, C70, 42CrMo4, Cf53, 1.2363, 1.2379, 1.2436 |
| Annealing under atmosphere / protective gas / vacuumHeat treatment | – | 5,200 mm × Ø 2,700 mm | a few grams – 25 t | – | Steels |
| Protective gas hardeningHeat treatment | – | – | – | – | Steels with carbon content from 0.2%, Cast iron |
| CarburizingHeat treatment | – | – | – | – | unalloyed steels, low-alloy steels |
| TemperingHeat treatment | – | – | – | – | 42CrMo4, C45, 34CrNiMo6, 30CrNiMo8, 50CrV4, 55NiCrMoV7 |
| Laboratory technology / materials testingTesting | – | – | – | – | – |
| Delivery service / logisticsEngineering | – | – | – | – | – |
5 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| fully automatic hardening system with loading stations | Ipsen | 1 | – | 2013 (erwe | Fronreute-Baienbach |
| Gas nitriding system | – | 1 | – | 2017 | Fronreute-Baienbach |
| Plasma nitriding systems (vacuum chambers) | – | – | Ø 900 x 2,000 mm to Ø 2,600 x 5,200 mm | – | Fronreute-Baienbach |
| Vacuum hardening furnaces | – | – | 800 x 1,200 x 700 mm | – | Fronreute-Baienbach |
| Annealing furnace | – | – | – | – | Fronreute-Baienbach |
Additional services
History
- 1998
Foundation of Pro Ion Härtetechnik GmbH by Reiner Bodenmüller, Karsten Franke and Manfred Schieber; start of plasma nitriding in a garage in Blitzenreute.
- 1999
Move into the purpose-built business premises in Blitzenreute; production start on May 15.
- 2003
Expansion of production in Fronreute-Blitzenreute by 400 m².
- 2005
Introduction of vacuum hardening.
- 2010
Purchase of the heat treatment shop of Müller-Weingarten AG; addition of conventional hardening processes.
- 2012
Groundbreaking for the new building in Baienbach; expansion from 1,200 to 3,000 m² of production space at a volume of €6 million.
- 2013
Move into the new company headquarters Fronreute-Baienbach in July.
- 2015
Investment in a fully automatic hardening system with loading stations from Ipsen.
- 2017
Portfolio expansion through the acquisition of a gas nitriding system.
- 2021
Expansion of the Ipsen system and implementation of a new order management system.
- 2022
Restructuring of the management: Manfred Schieber (Technology) and Moritz Plattner (Finance & Sales).