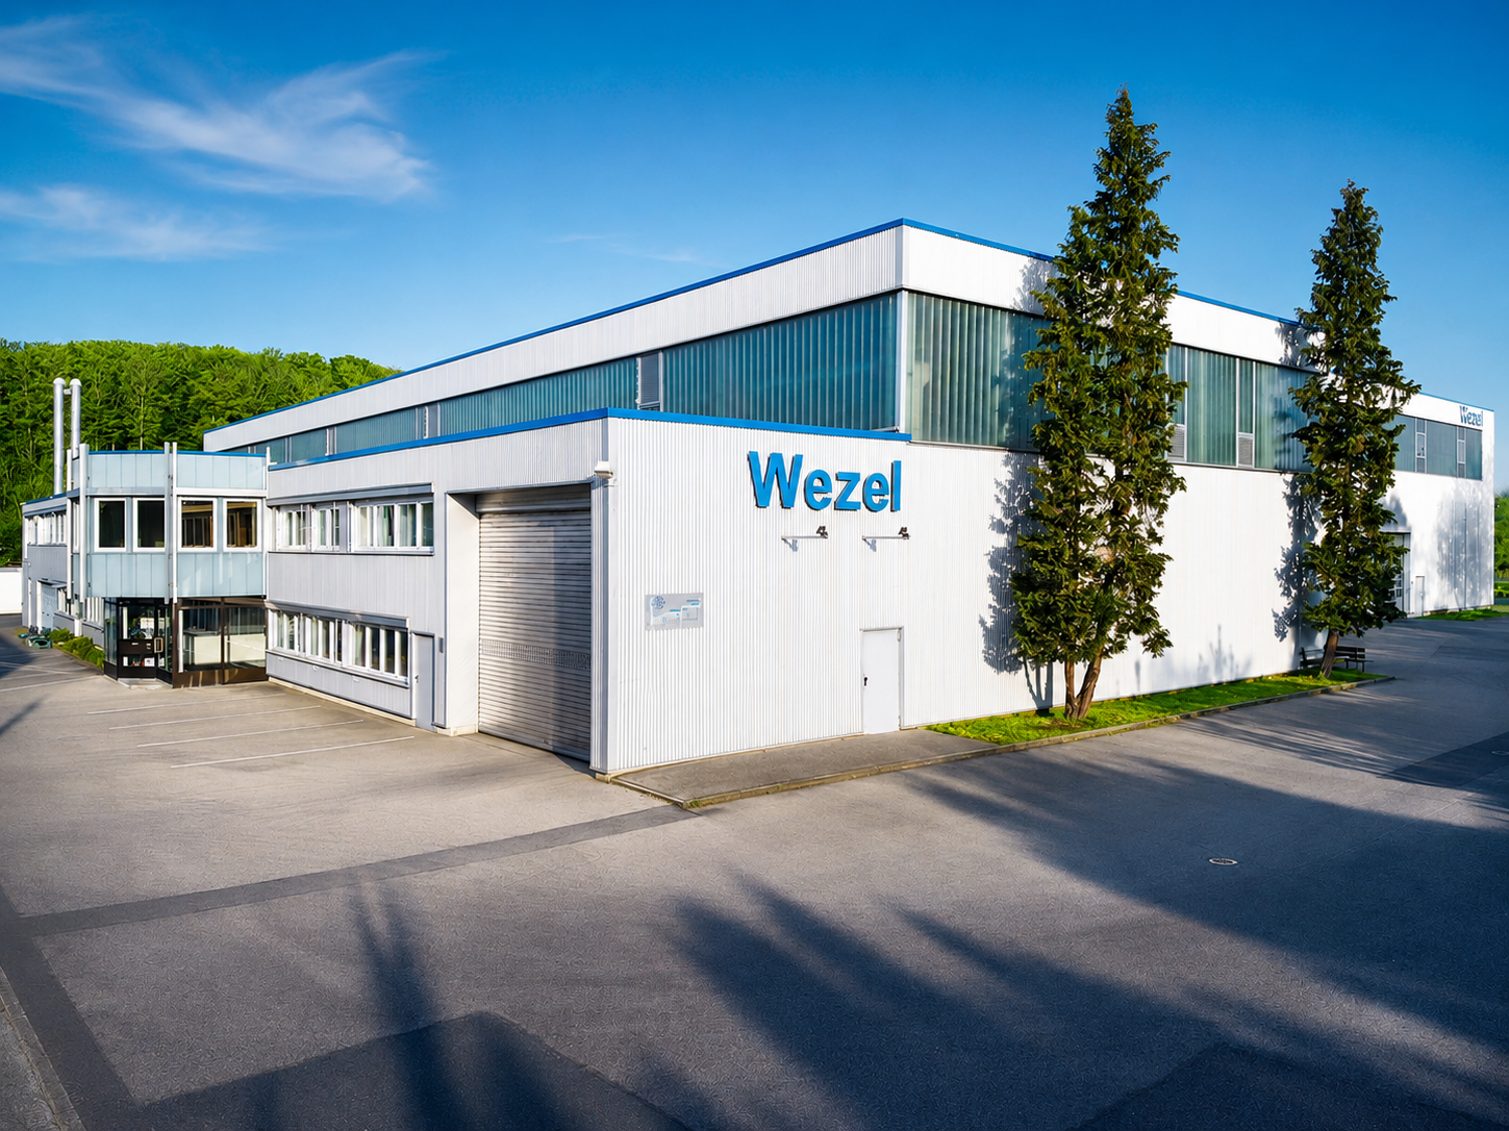
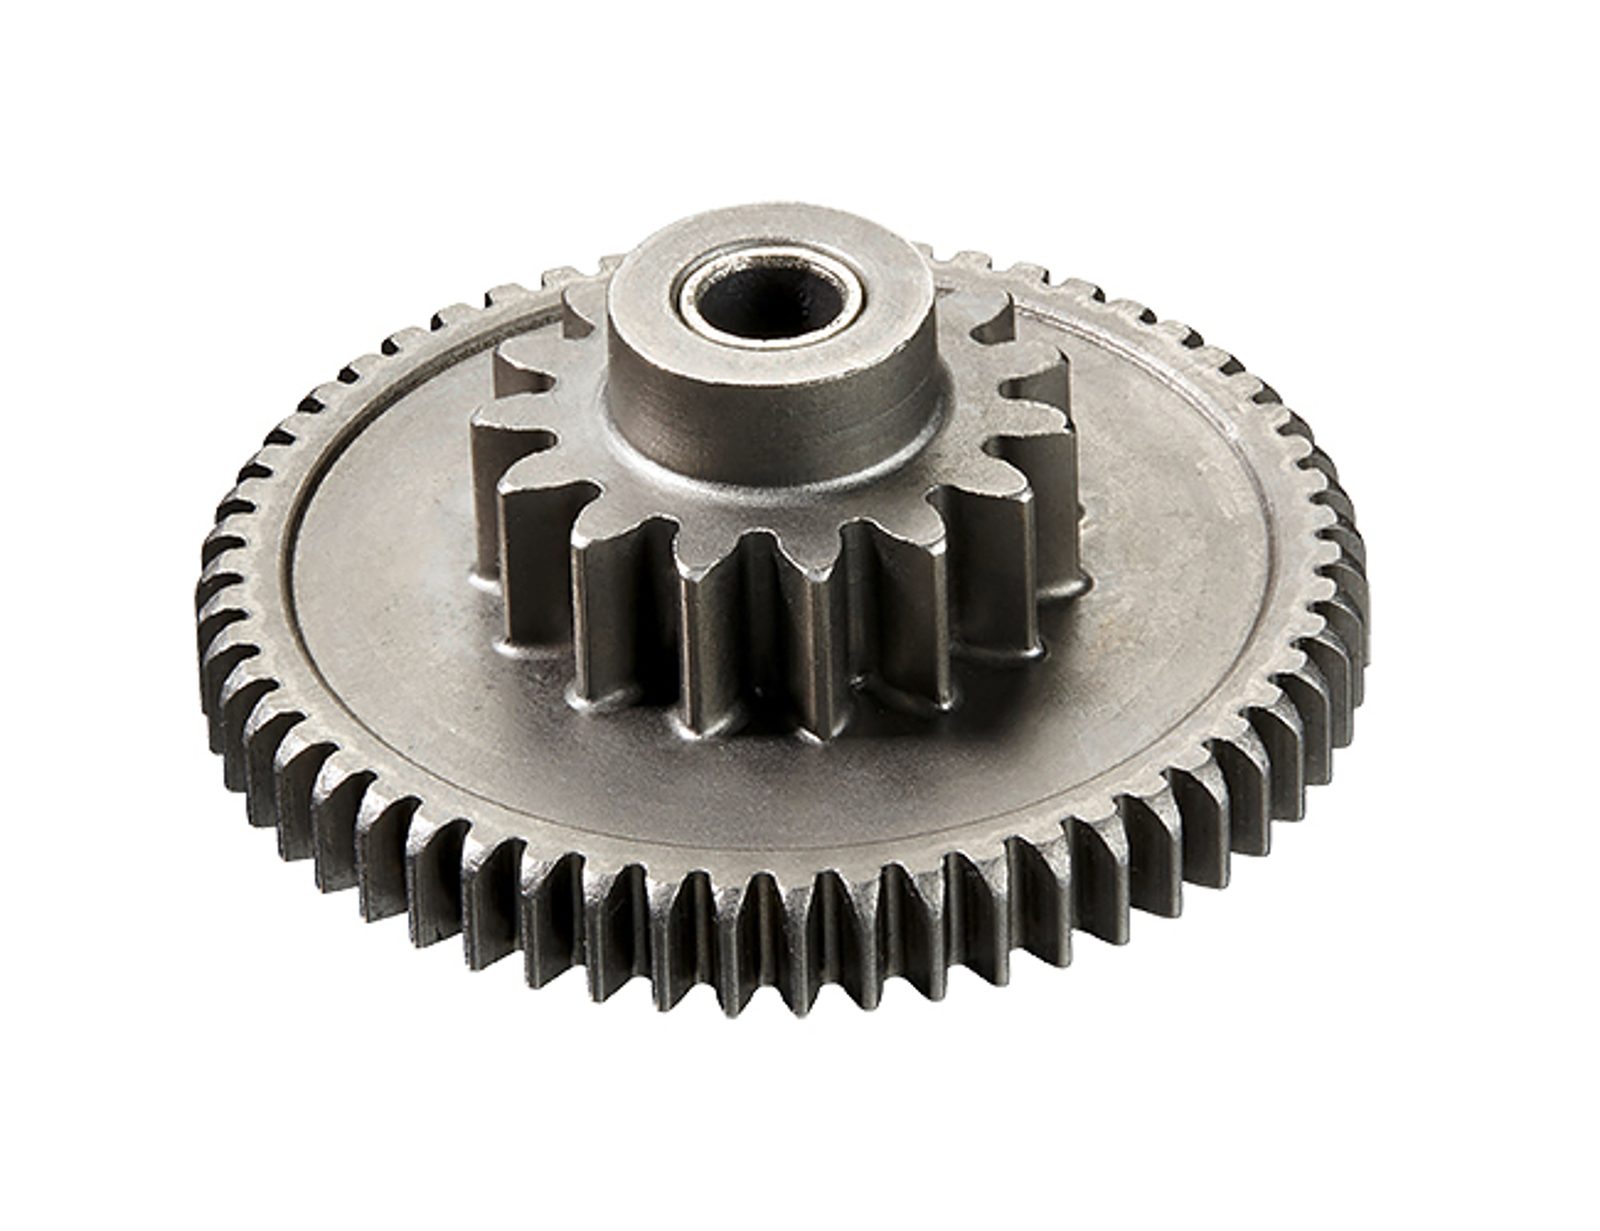
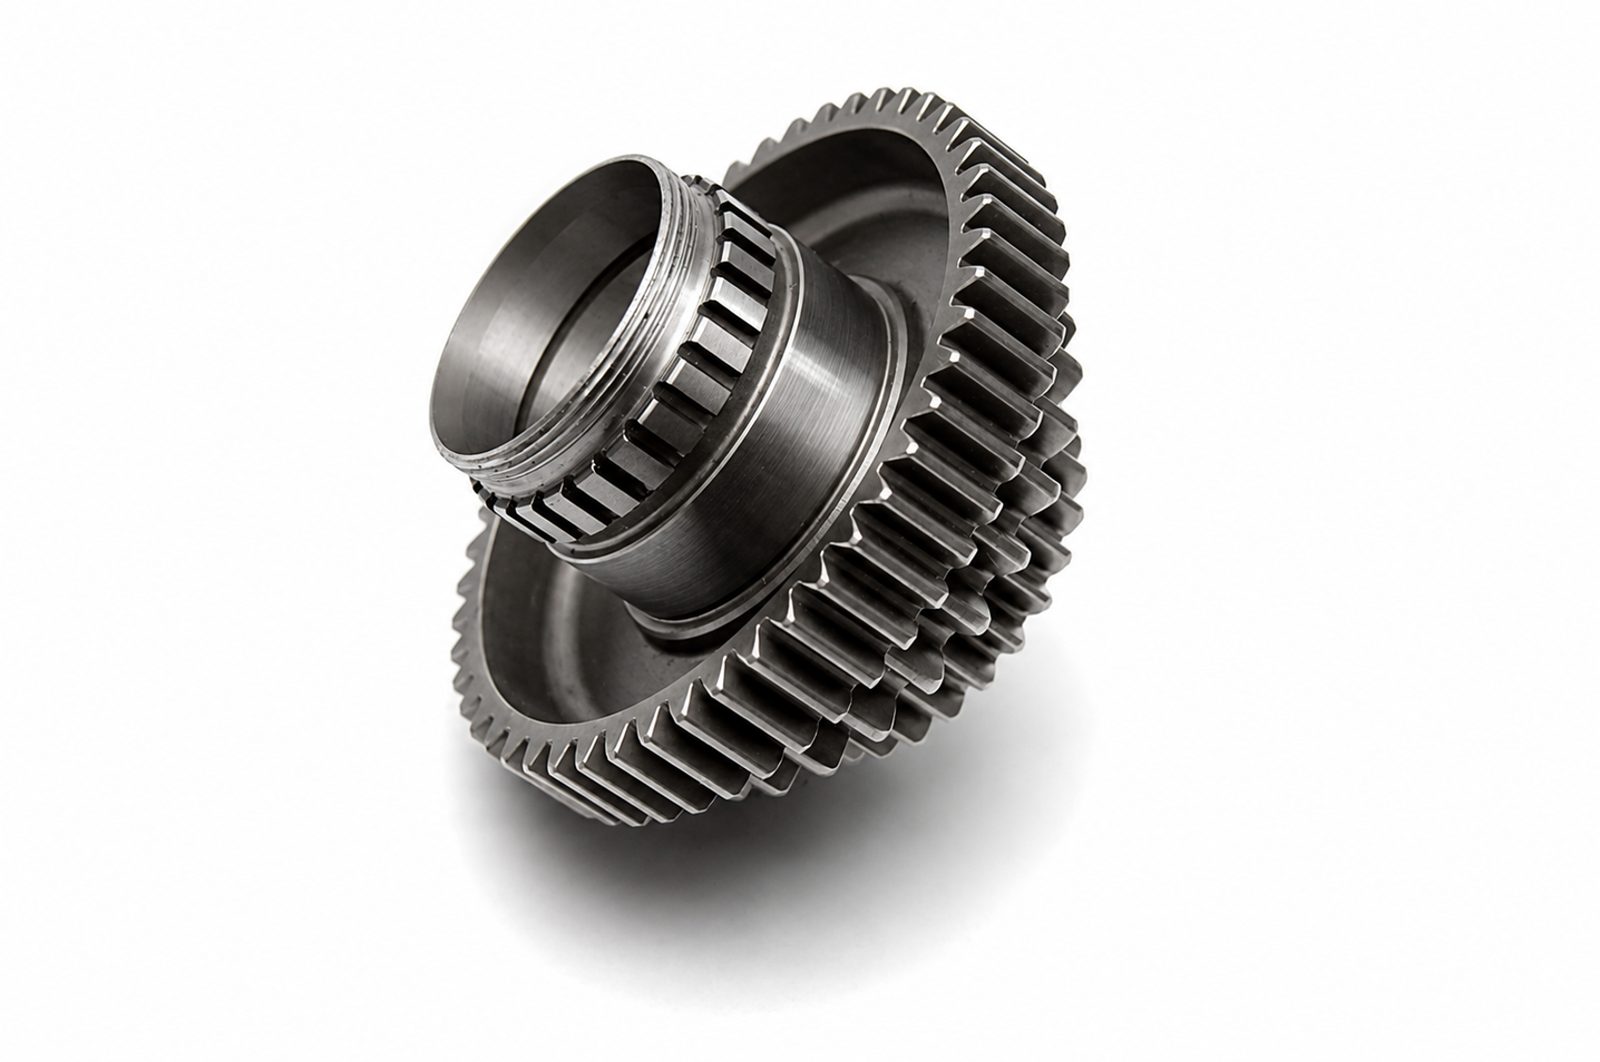
Cold extrusion-pressed precision gears, gearing components and clutch geometries from Frickenhausen – from prototype to 500,000 units.

Wezel GmbH Kaltumform-Technik
Frickenhausen (Baden-Württemberg)New on Amplifa
About Wezel GmbH Kaltumform-Technik
Wezel GmbH Kaltumform-Technik is a family-run SME founded in 1948 by Erich Wezel in Frickenhausen that manufactures highly precise gearing components, clutch geometries, gear blanks and clamping tools. Around 100 employees produce on 10,000 m² of production floor space using cold forming (cold extrusion pressing), 3- and 5-axis milling, soft and hard machining, induction hardening and in-house metrology. Extrusion-pressed gear teeth with uninterrupted grain flow offer higher root load capacity than machined gear teeth. Lot sizes range from prototype (from 1 unit, using in-house toolmaking) to series production of 500,000 units; aluminium is manufactured up to Ø 240 mm, steel and copper up to Ø 160 mm. Wezel supplies nine industries, including E-Mobility & Automotive (series supplier for over 20 years), motorcycles, convertible-top gearboxes, mobile hydraulics, power tools, rail brake systems, medical technology and clamping technology. Reference customers include BMW, Bosch, Porsche, Schaeffler and Festool; the company is ISO 9001:2015 certified and a member of IMU, GCFG and ICFG.
- Site
- Frickenhausen
- Processes
- Cold forming (cold extrusion pressing) of gearing components, Extrusion pressing of profiles, cams, spur and helical gear teeth (up to 4 gear teeth per, Toolmaking (manufacture of toothed extrusion pressing dies), 3- and 5-axis milling, Soft machining (turning), Hard machining: grinding / hard turning (internal + external), Laser cutting, Induction hardening / induction tempering
- Materials
- EN AW-6082 (AlMgSi1), 16MnCr5, 20MnCr5, 31CrMoV9, 18CrNiMo7-6, 42CrMo4, C8C, X17CrNi16-2
- Certificates
- DIN EN ISO 9001:2015, ÖKOPROFIT Company 2025, 100 Companies for Resource Efficiency, ISO 9001, ÖKOPROFIT
- Founded
- 1948
- Employees
- ~100
- Industries
- E-Mobility & Automotive, Motorcycles, Convertible tops & tailgates, Mobile hydraulics, Industrial drives, Power tools
- 01
Design & Engineering
- 02
Toolmaking (toothed extrusion pressing dies)
- 03
Cold extrusion pressing
- 04
Measuring & Testing
- 05
Soft and hard machining
- 06
Induction hardening / soft annealing
- 07
Coating technology (phosphating, lubricant)
- 08
Assembly of ready-to-install assemblies
- 09
Delivery
Materials & Processes
Cold extrusion pressing
Cold forming of profiles, cams, spur/helical gear teeth (up to 4 gear sets per component), bevel gears and crown gears with preserved grain flow and high fatigue strength.
Aluminium AlMgSi1
Lightweight gears and housings up to Ø 240 mm, pore-free and cold-work hardened, e.g. for e-bike drives.
16MnCr5
Main grade of case-hardening steel for highly stressed gear teeth in automotive, motorcycle and industrial gearboxes.
20MnCr5
Case-hardening steel for high-fatigue-strength gearing components in series production.
31CrMoV9
Nitriding steel for wear-stressed gear teeth and gearbox components.
18CrNiMo7-6
Case-hardening steel for gears under heavy dynamic loads.
42CrMo4
Quenched and tempered steel for highly stressed drive components.
X17CrNi16-2
Martensitic stainless steel on request for corrosion- and wear-resistant components.
X46Cr13
Martensitic stainless steel on request, e.g. for clamping tool sleeves.
Pure copper E-Cu
Extrusion-pressed contact bushings for high-voltage technology with reduced chip generation during machining.
Machining (turning, milling, grinding)
3- and 5-axis milling, soft turning, hard turning and grinding machined to IT6/IT7.
Induction hardening / induction tempering
In-house heat treatment for hardened, ready-to-install gear teeth; hardening, nitriding and gear grinding via fixed partners.
Locations
Frickenhausen
DECompany headquarters, production, press plant
- Part weight / size
- Aluminium Ø 240 mm, steel/copper Ø 160 mm
- Lot size
- 1 – 500,000 units
- Materials
- Aluminium, steel, stainless steel, copper
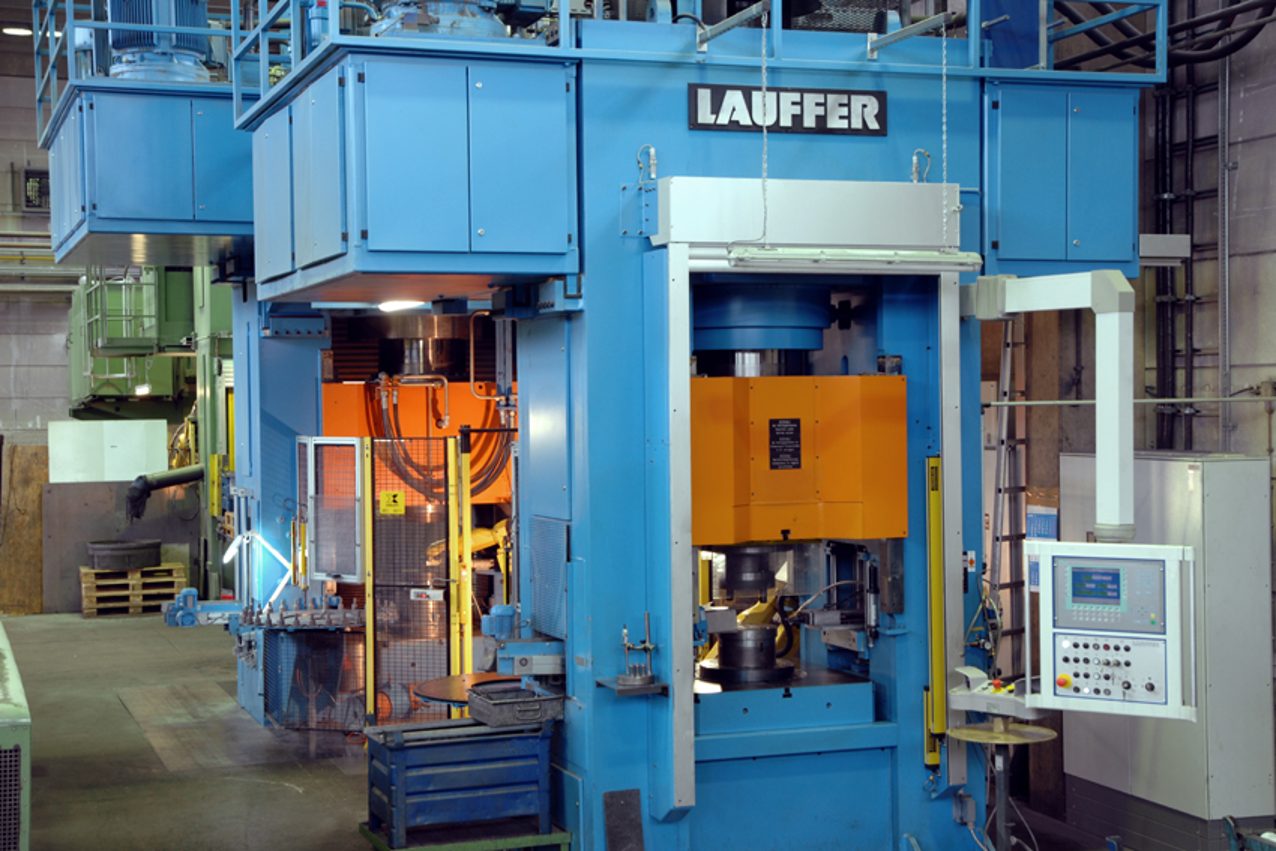
- LAUFFER cold extrusion presses
- Automated production lines
- 3-/5-axis milling machines
- Klingelnberg gear measuring machine
- ZEISS DuraMax coordinate measuring machine
- Hardness testing devices
Components
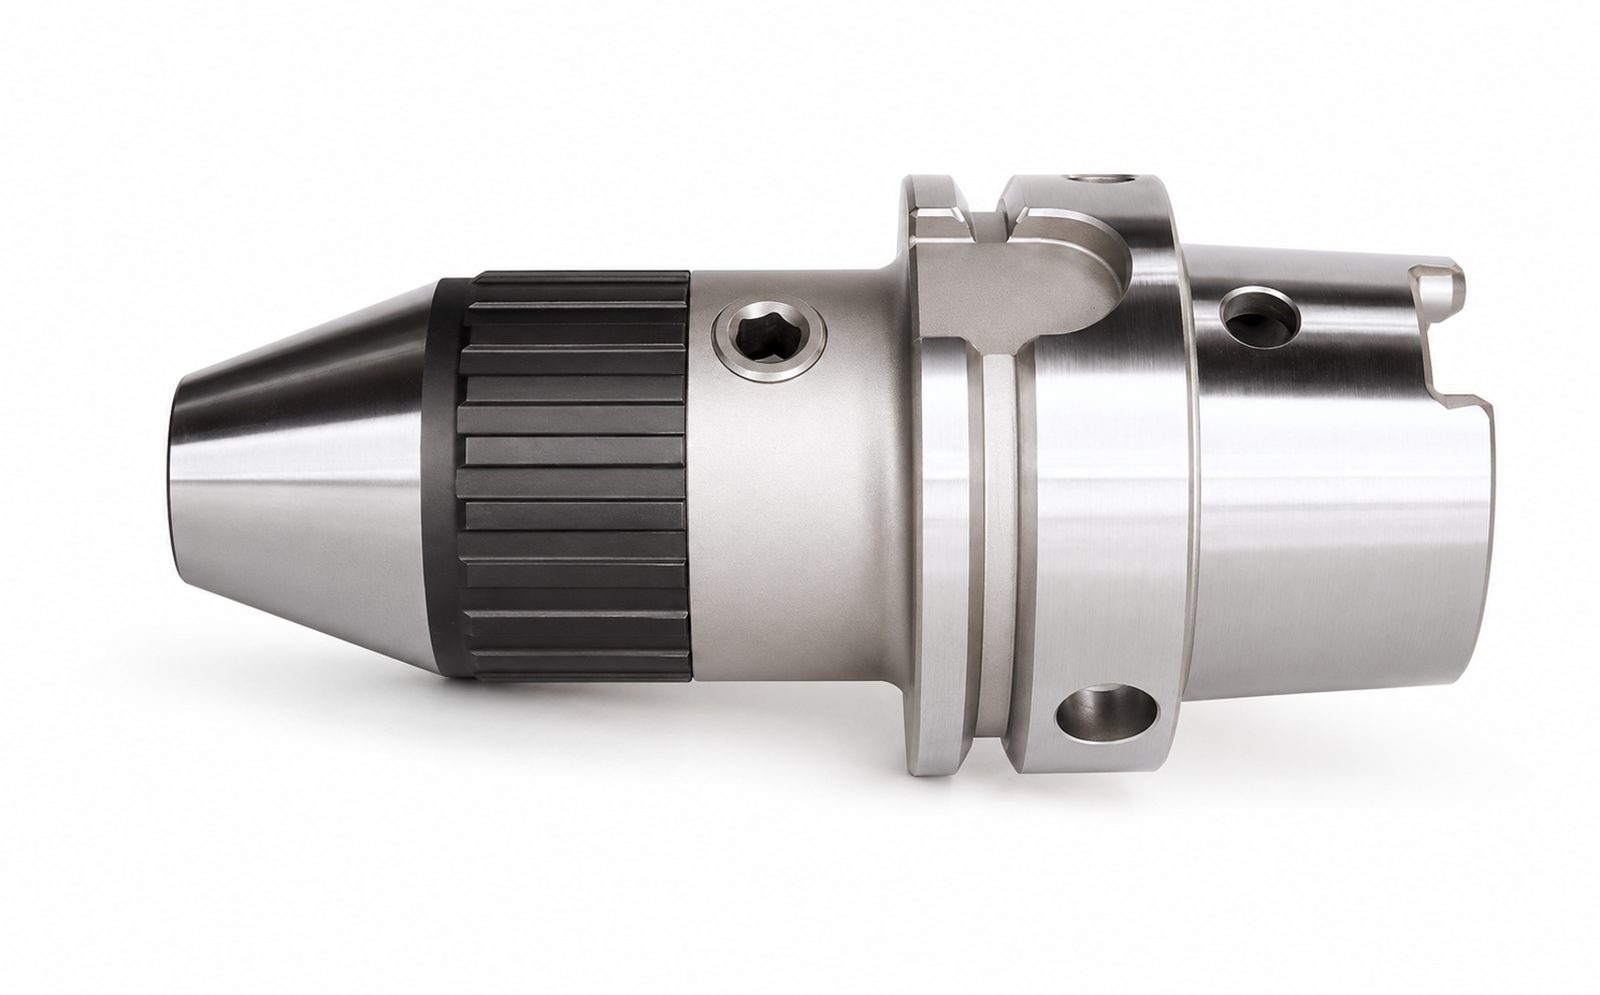
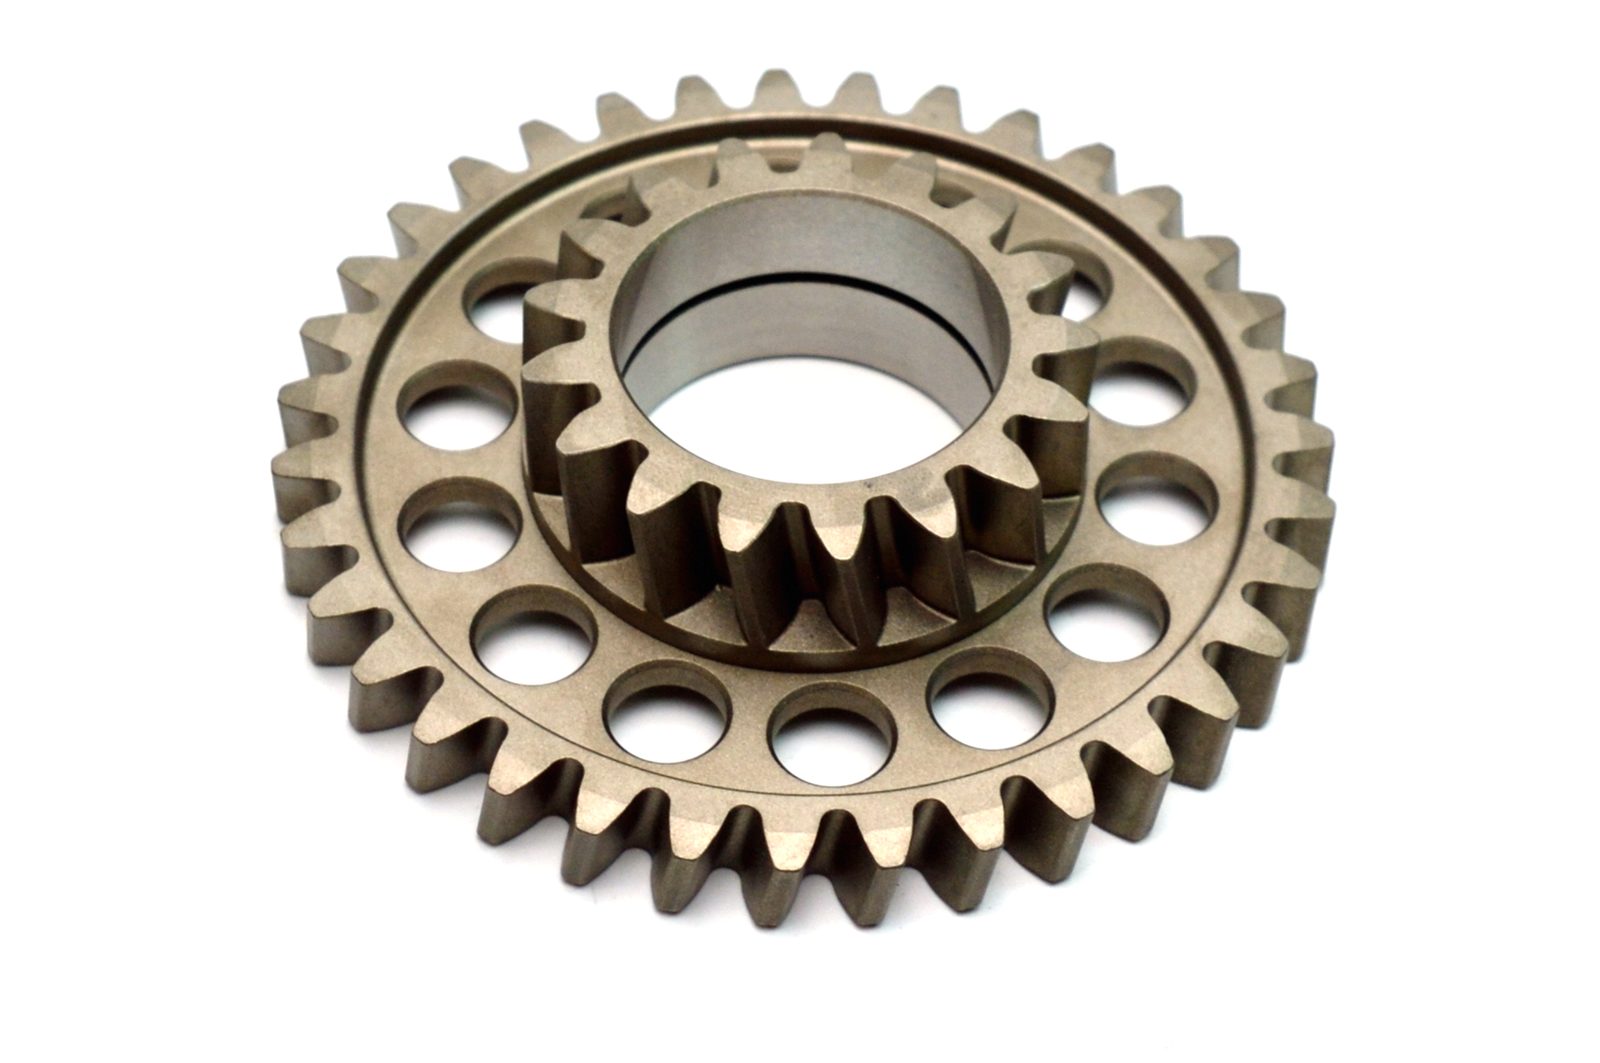
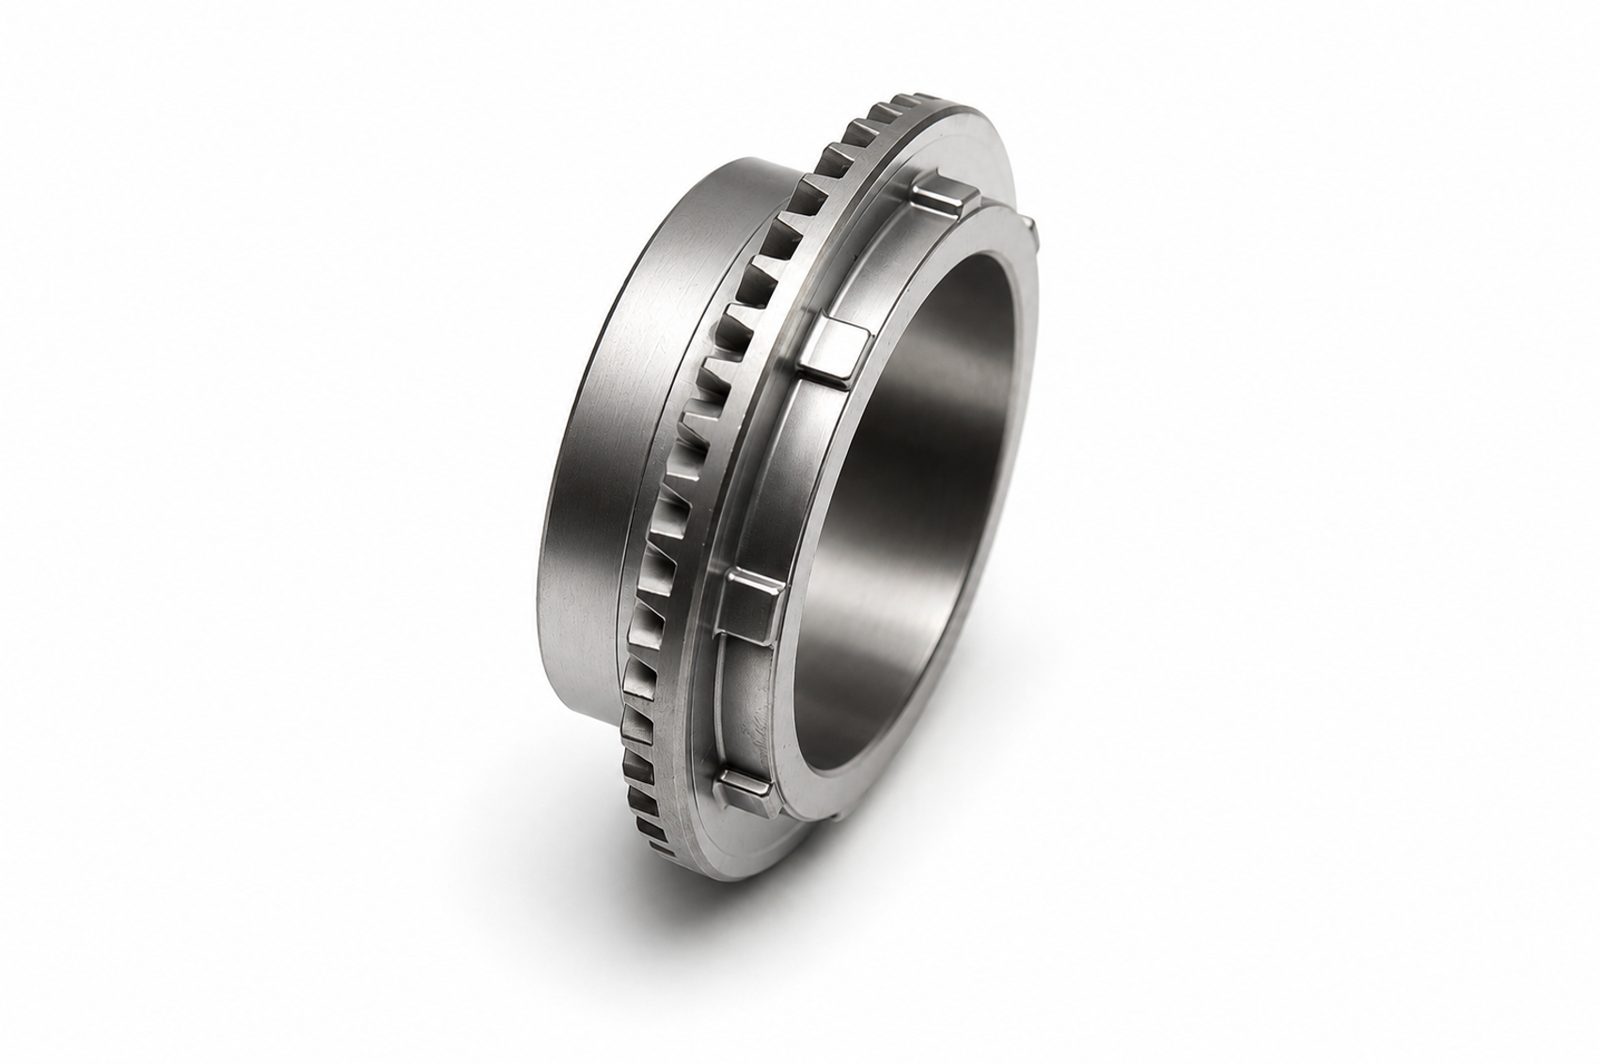
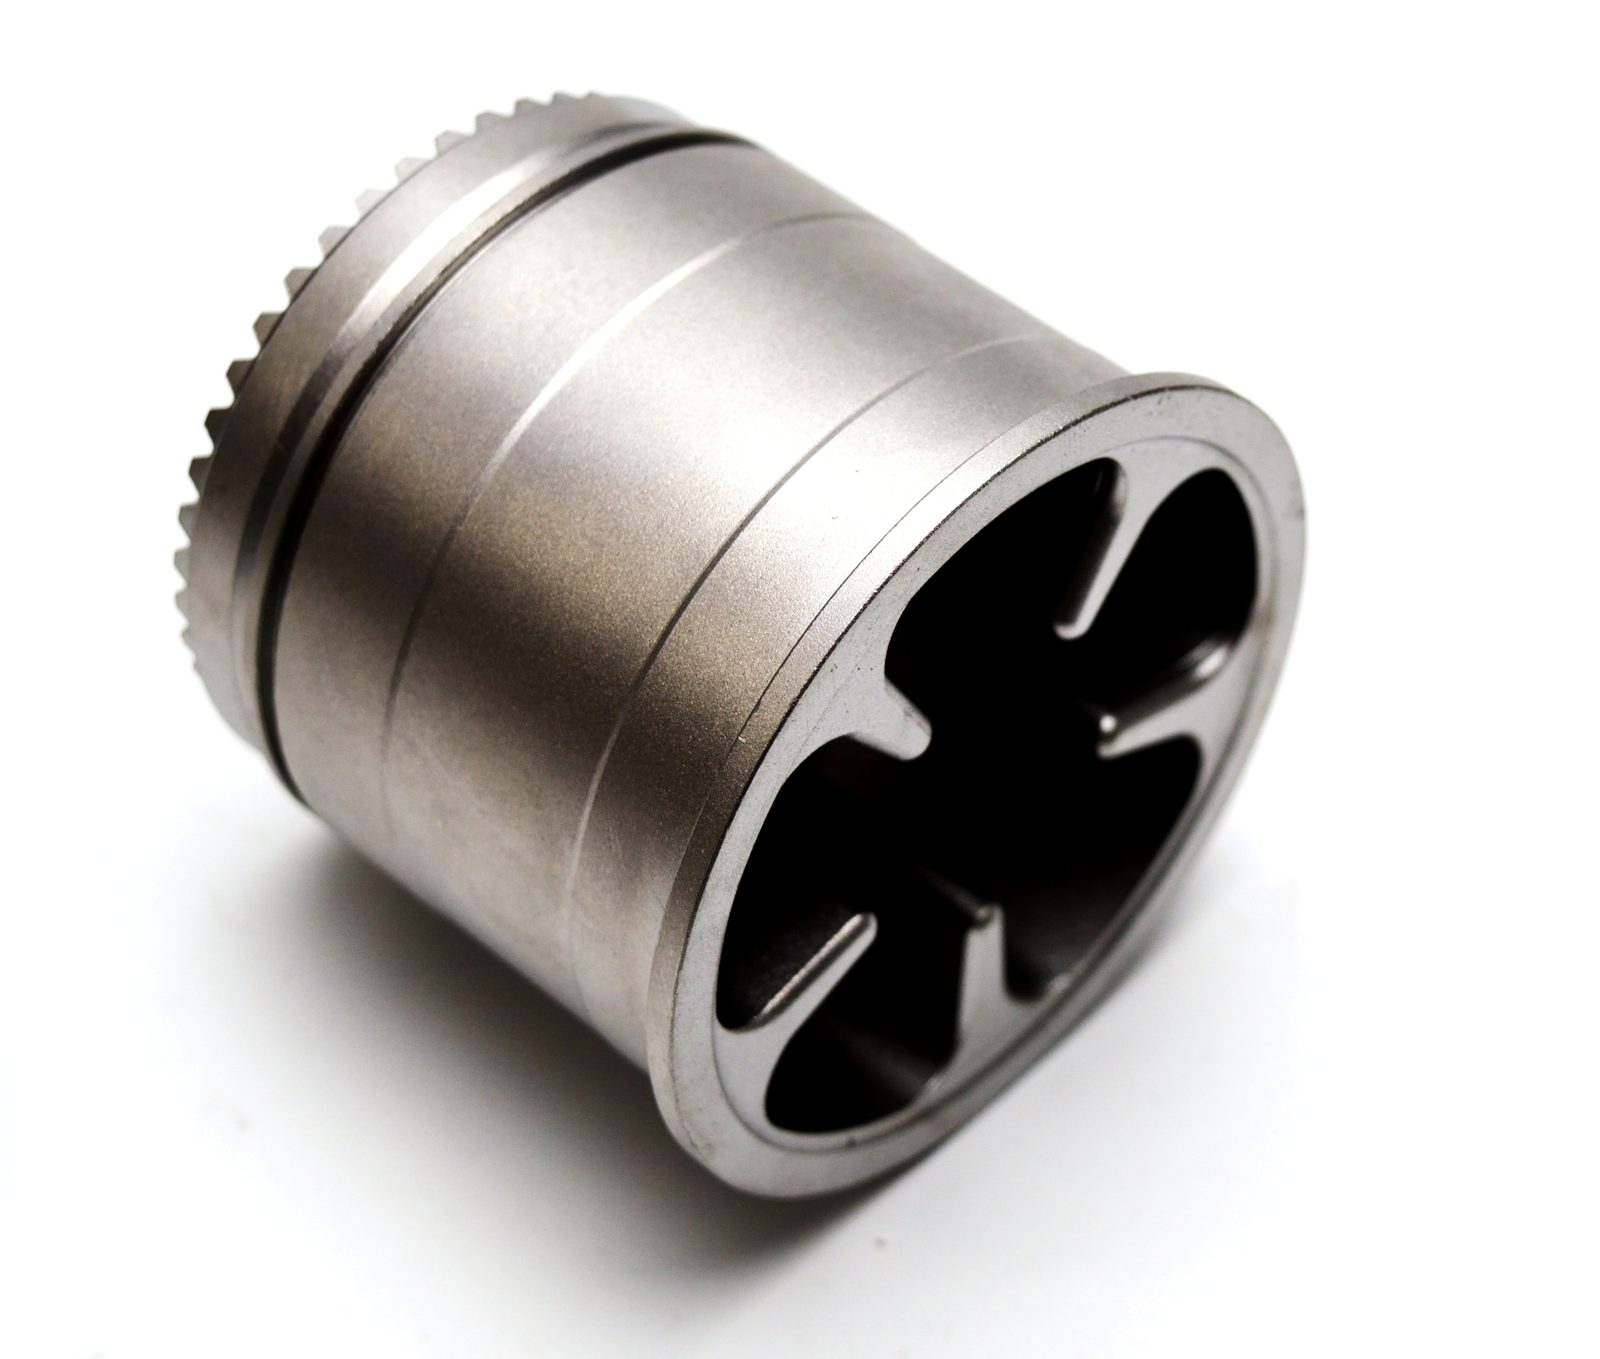
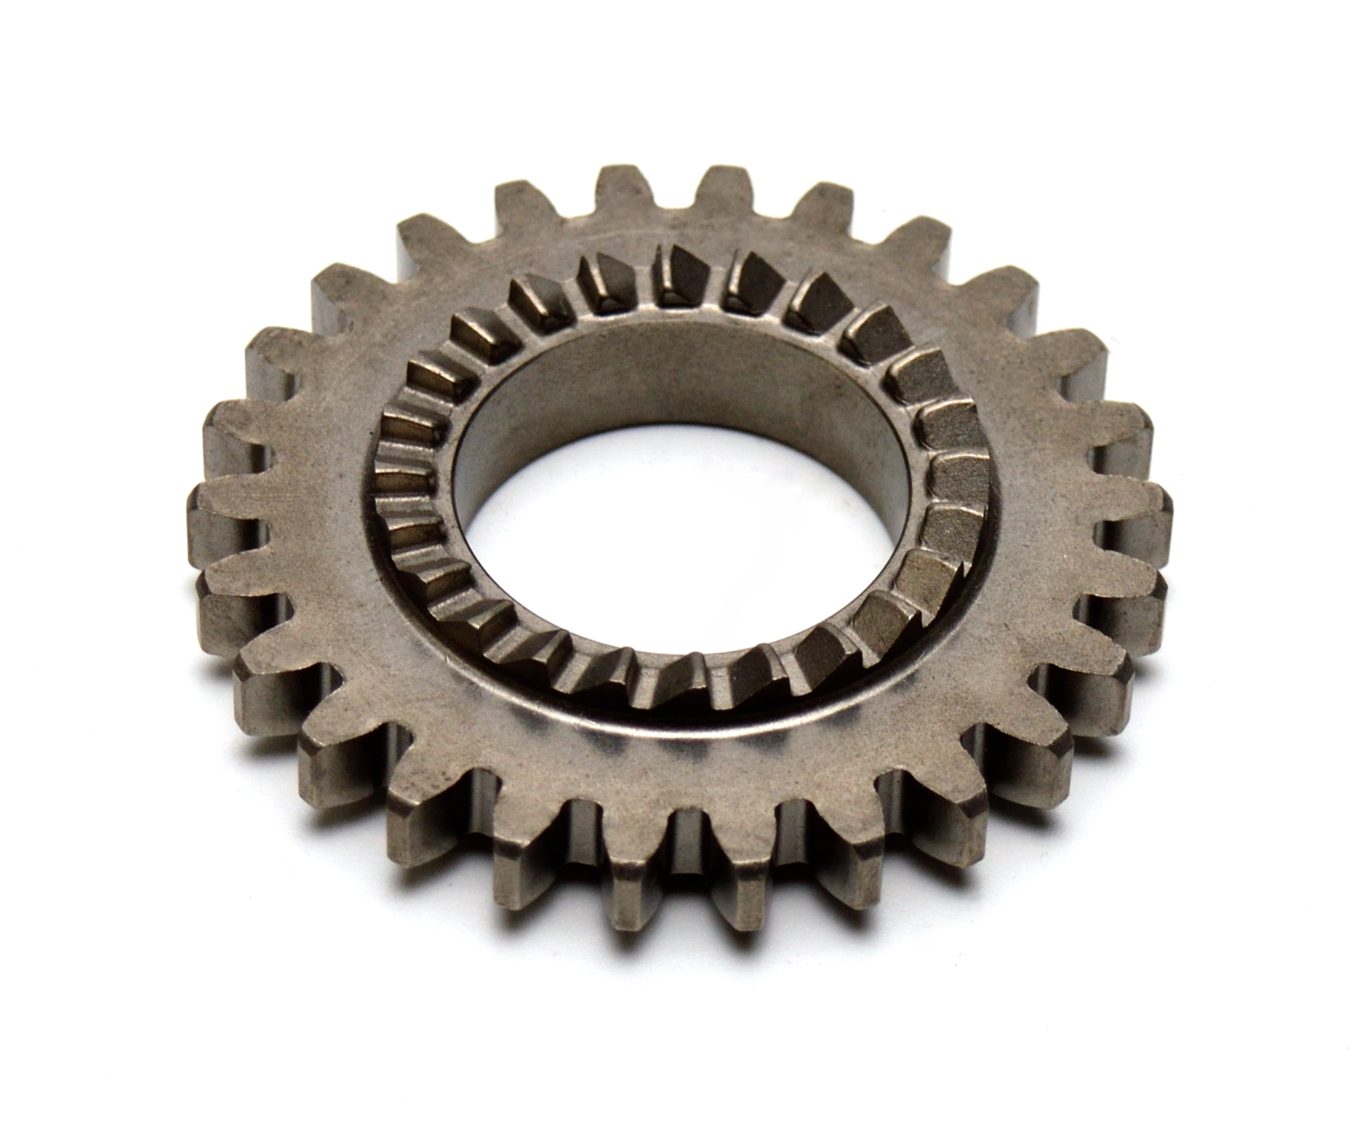
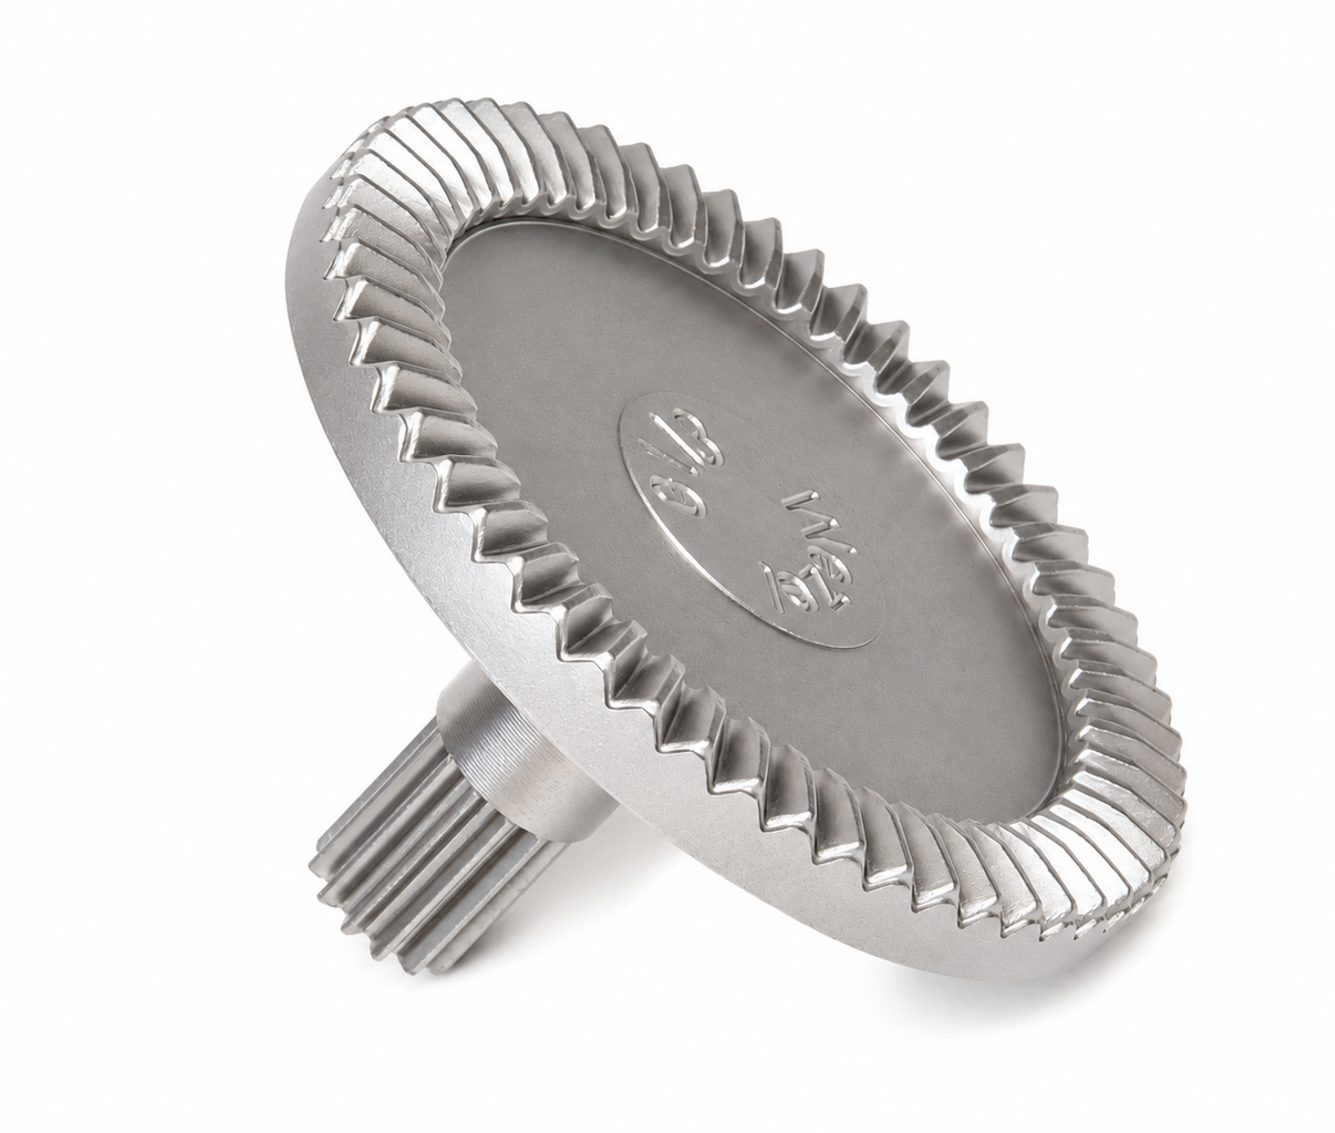
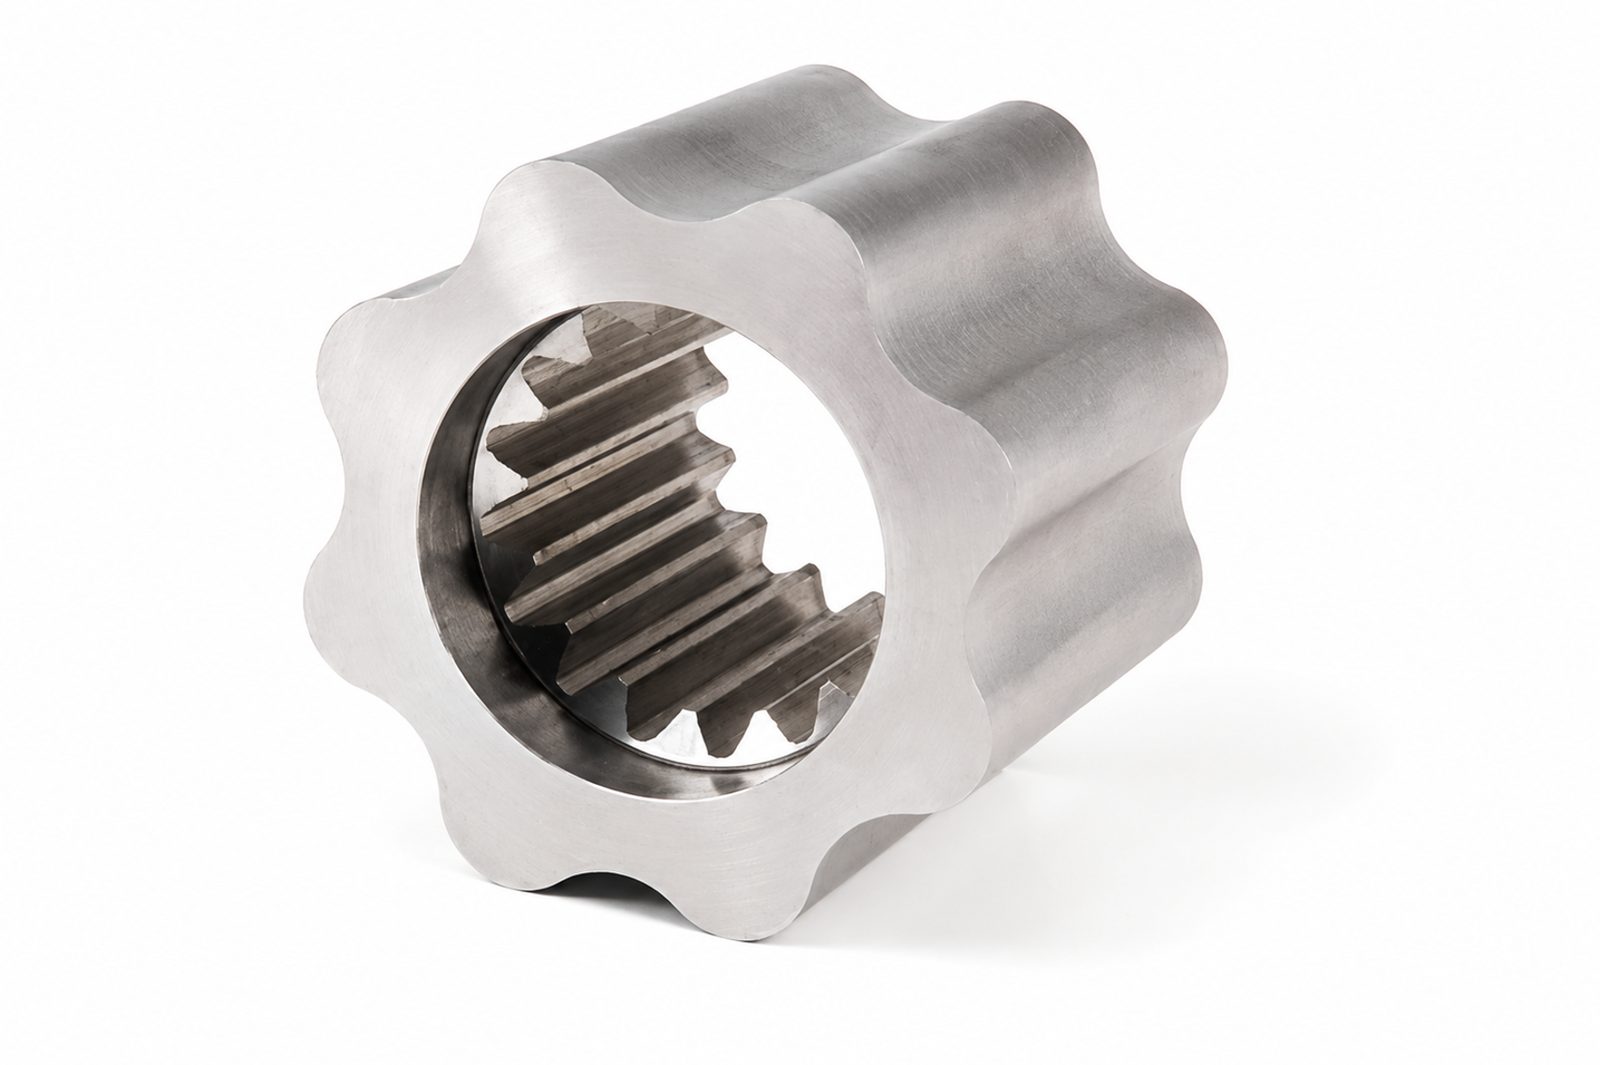
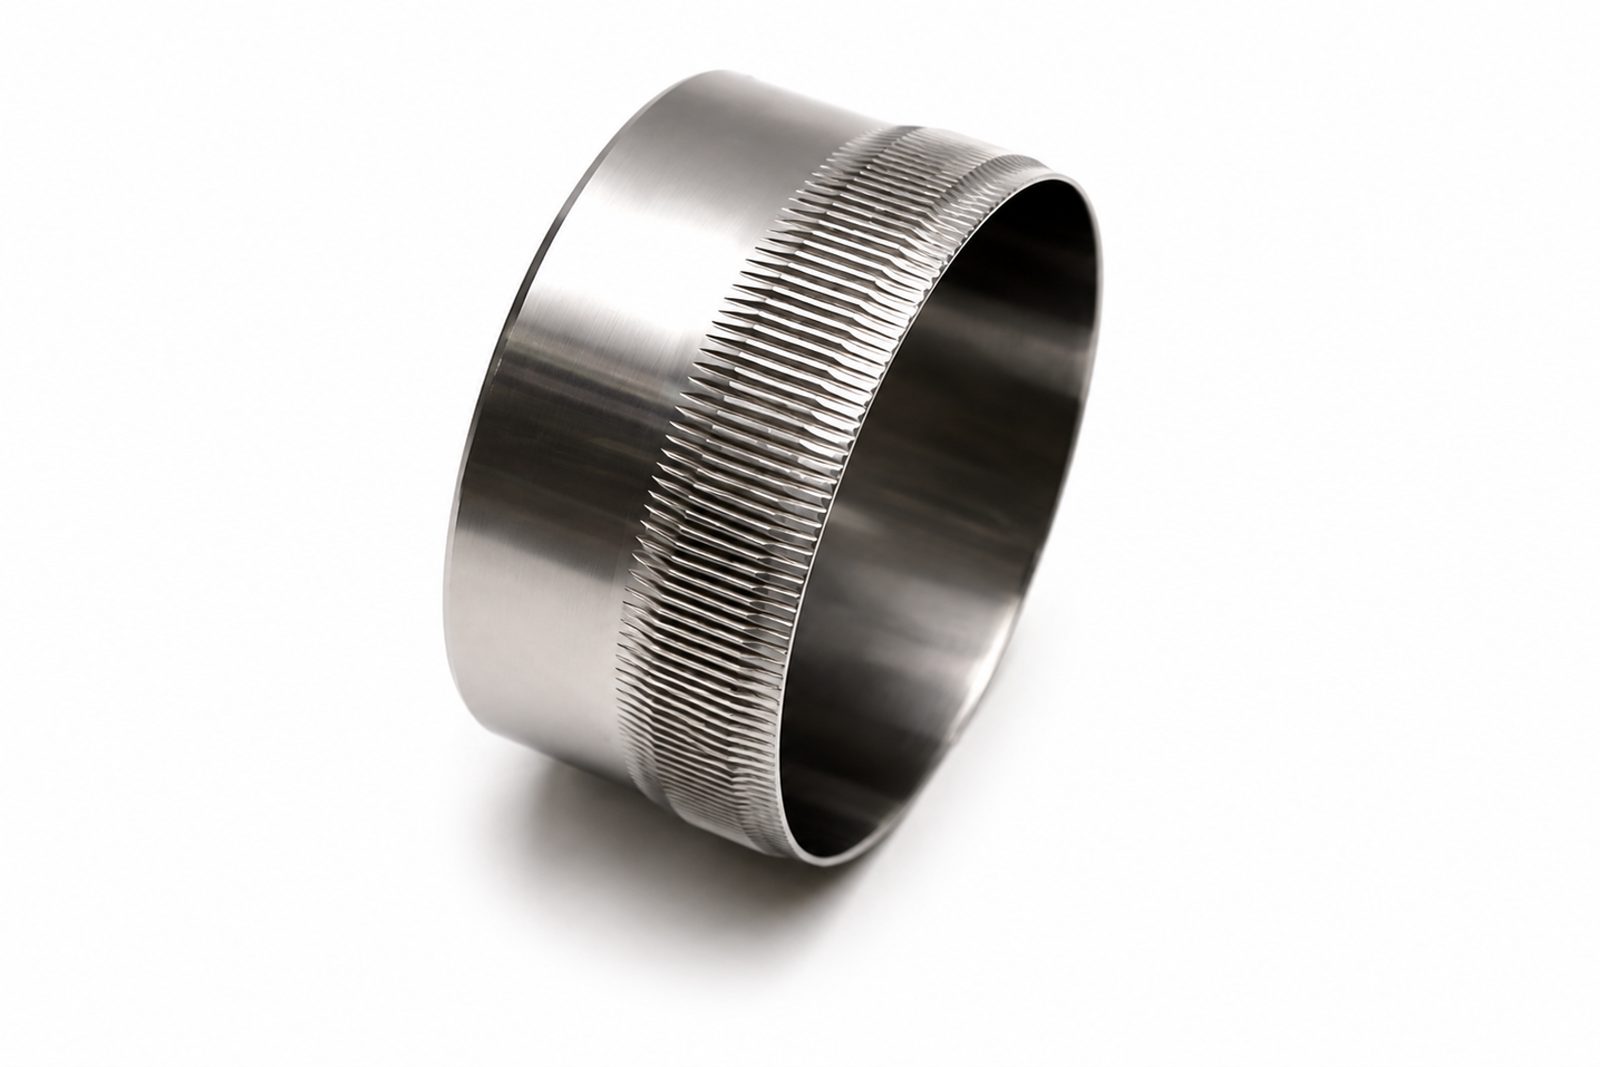
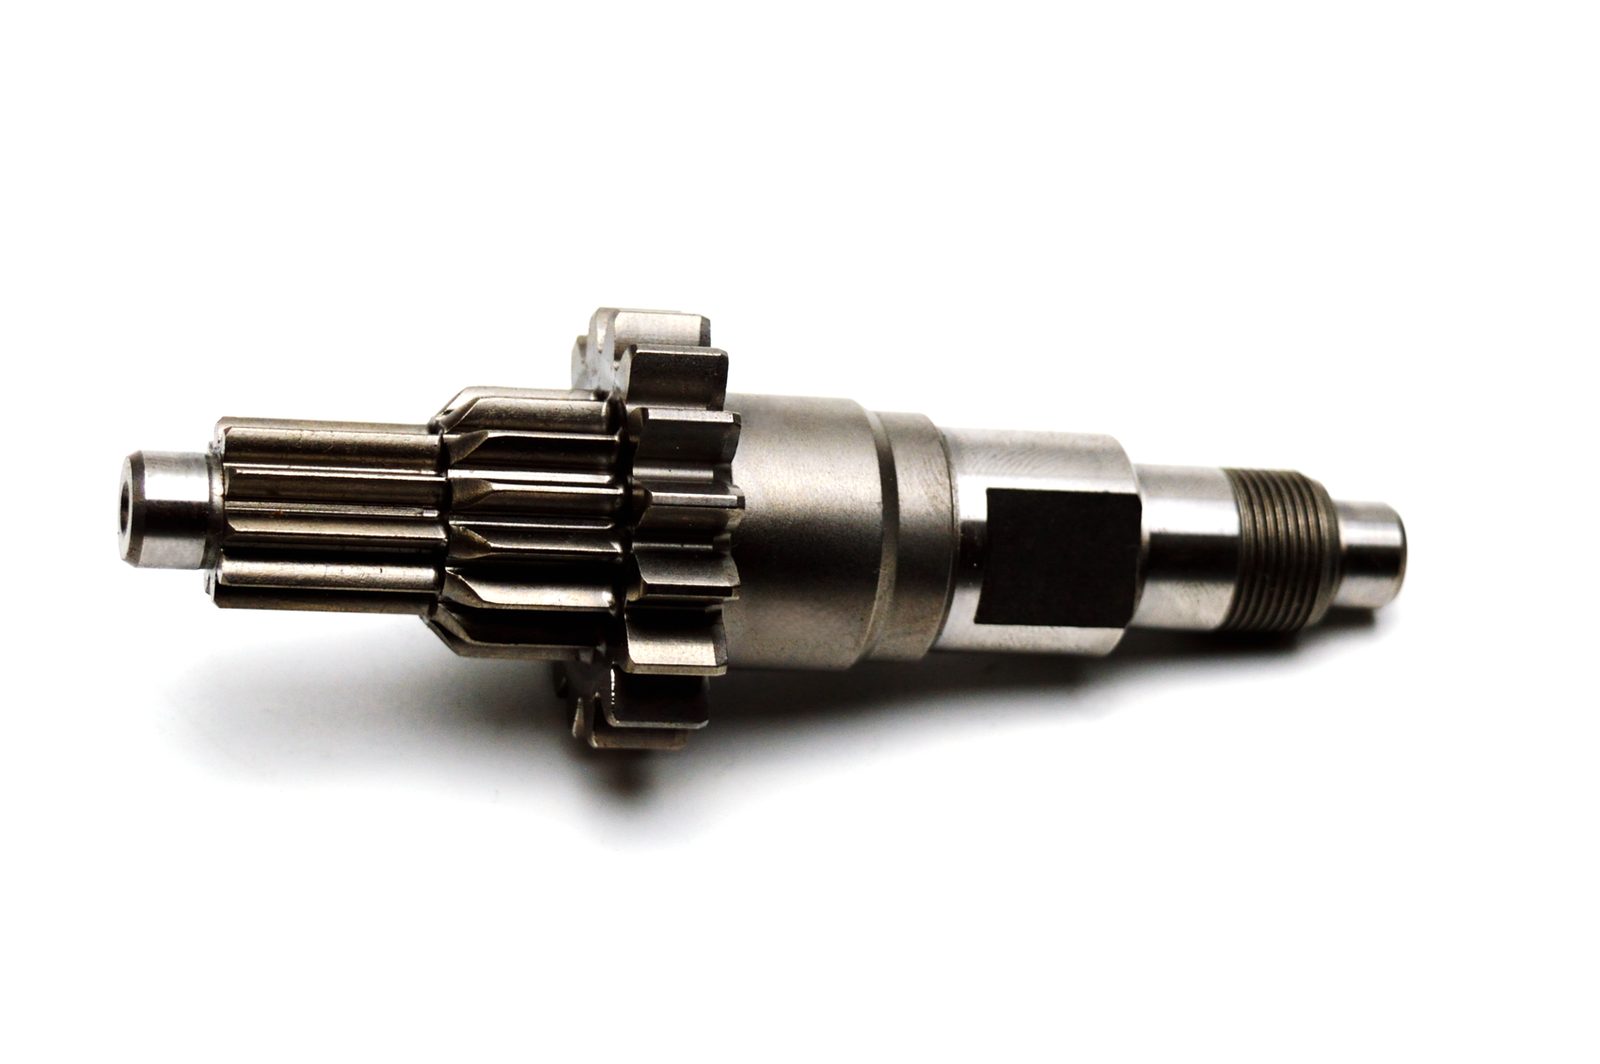
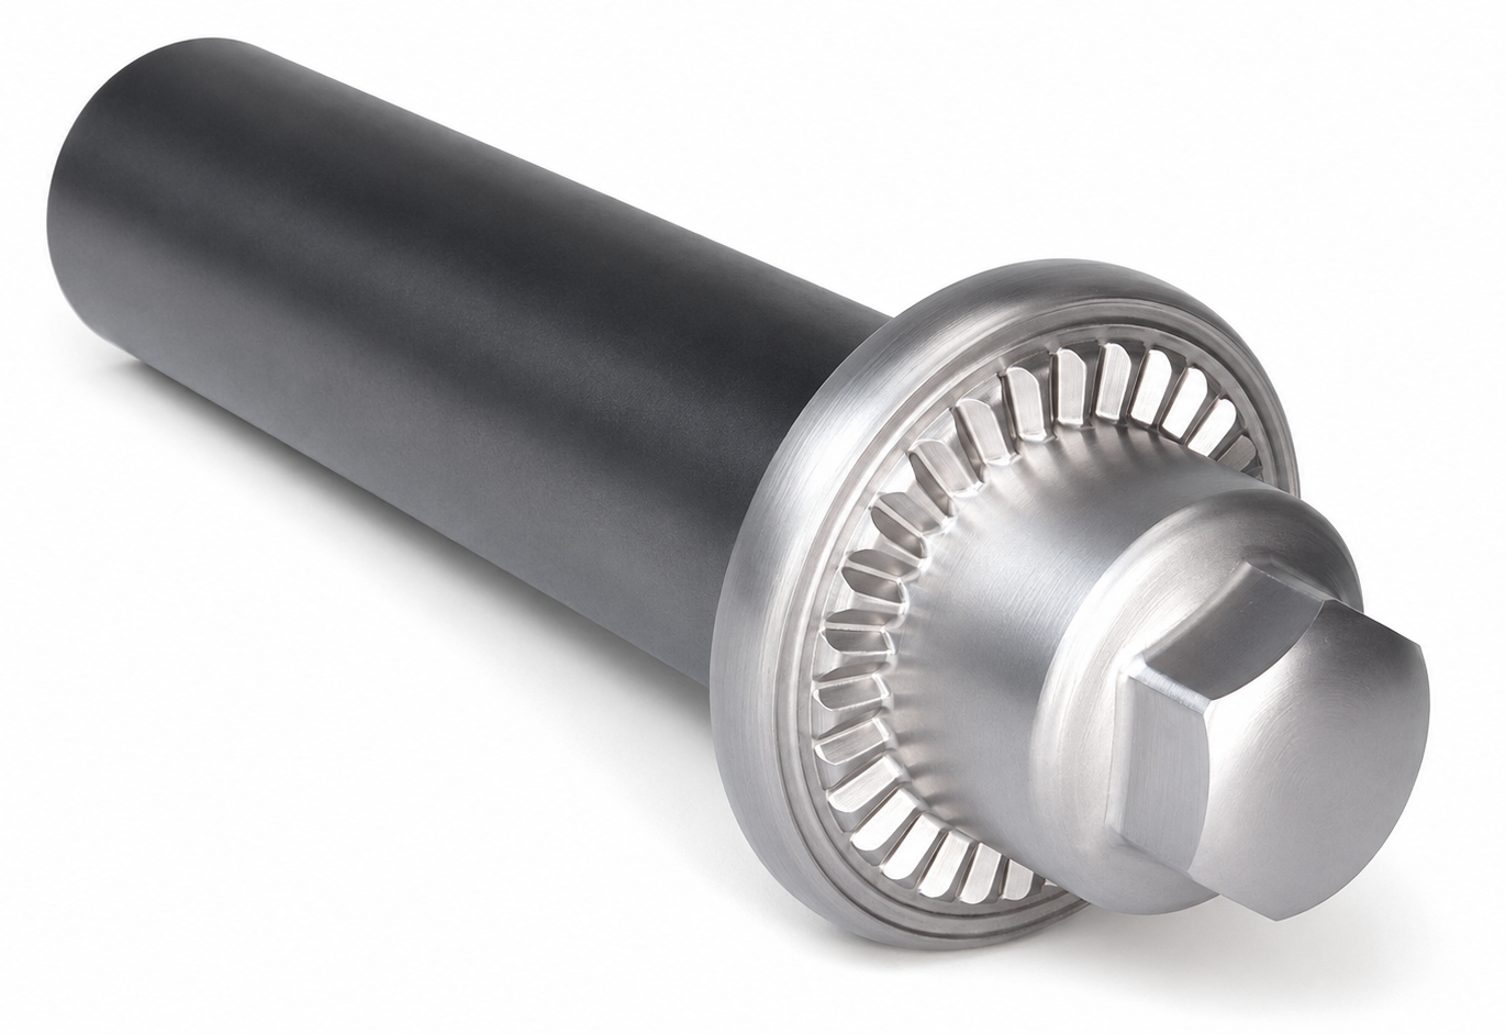
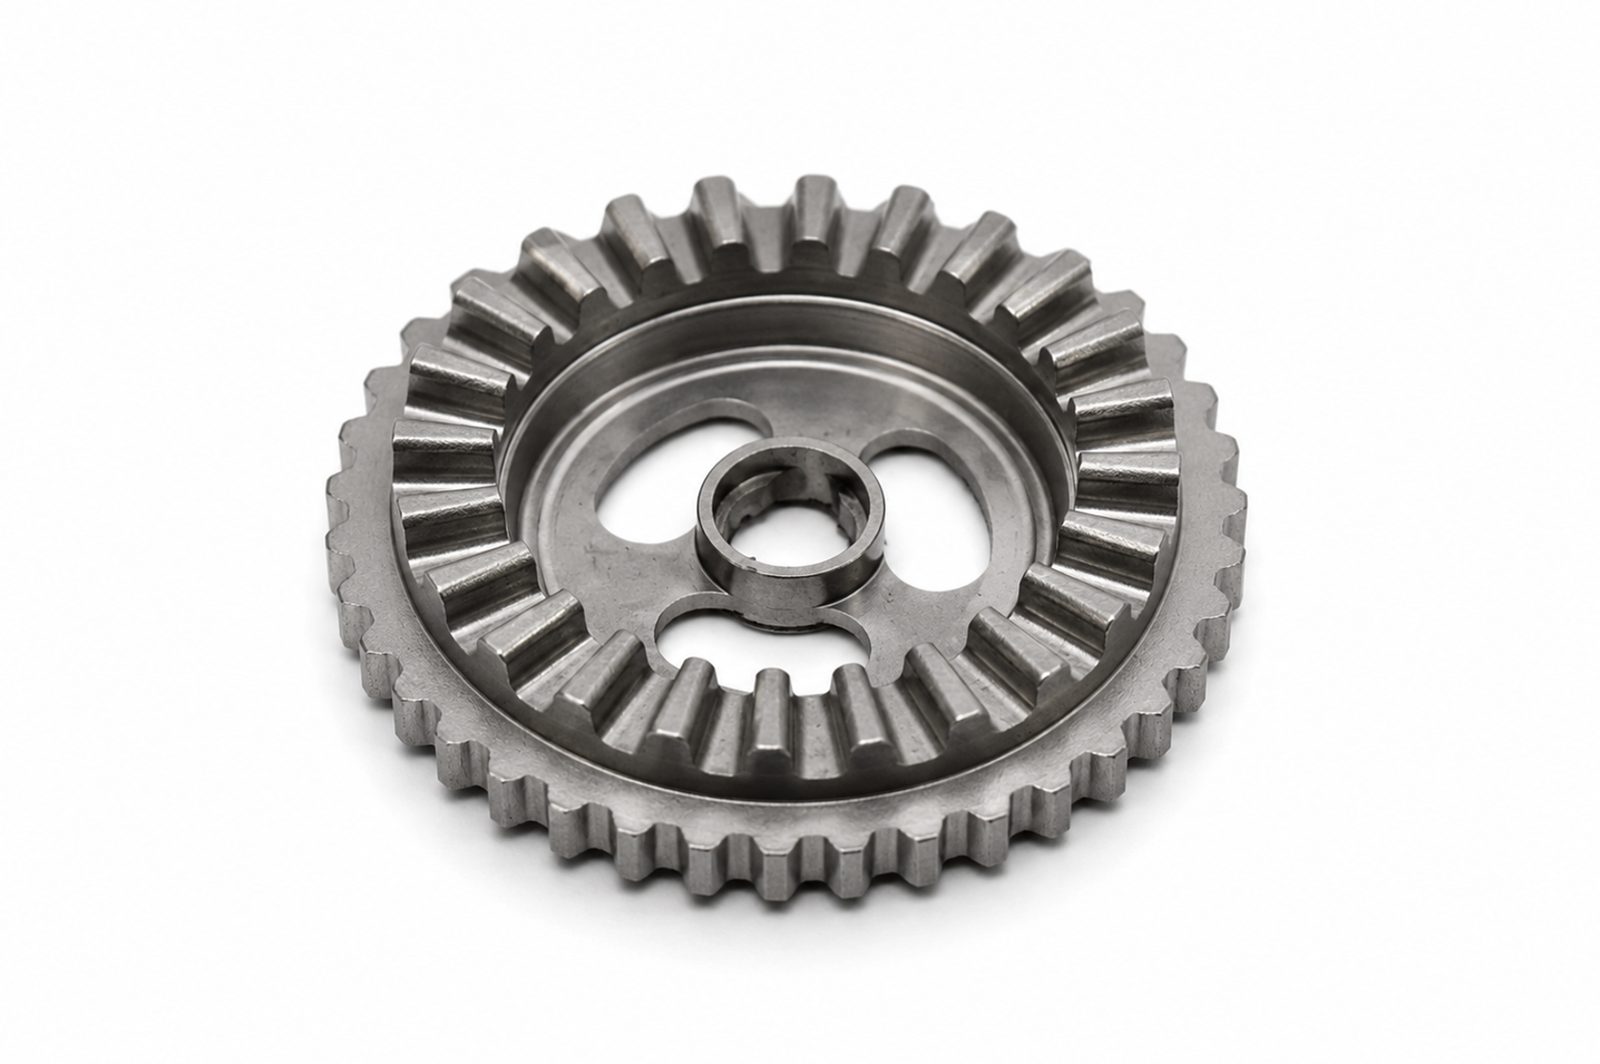
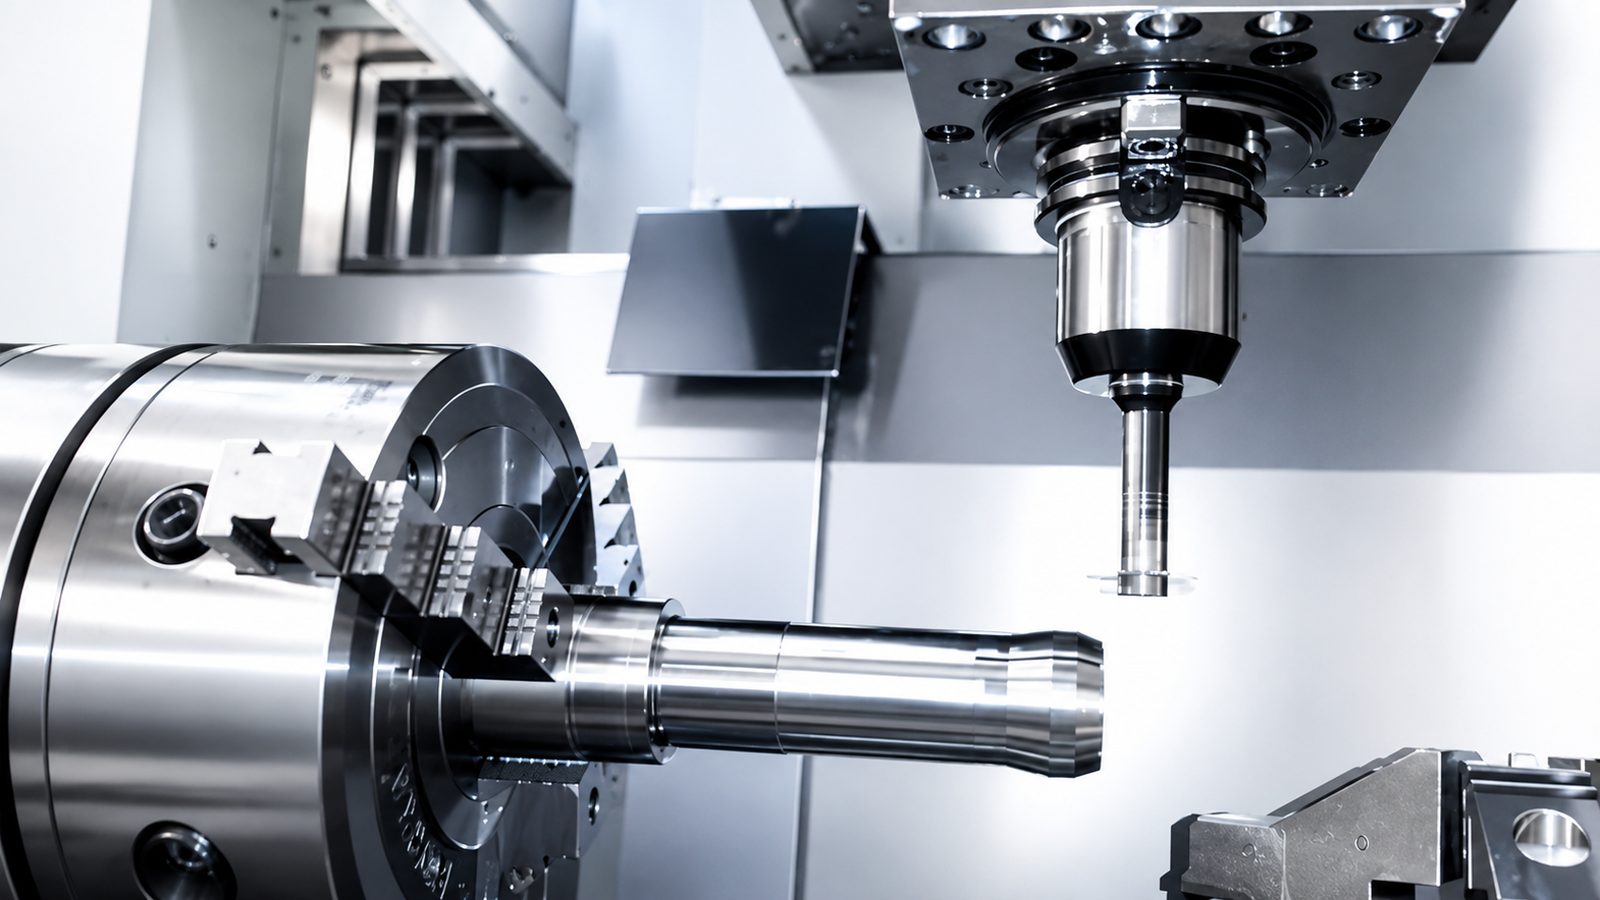
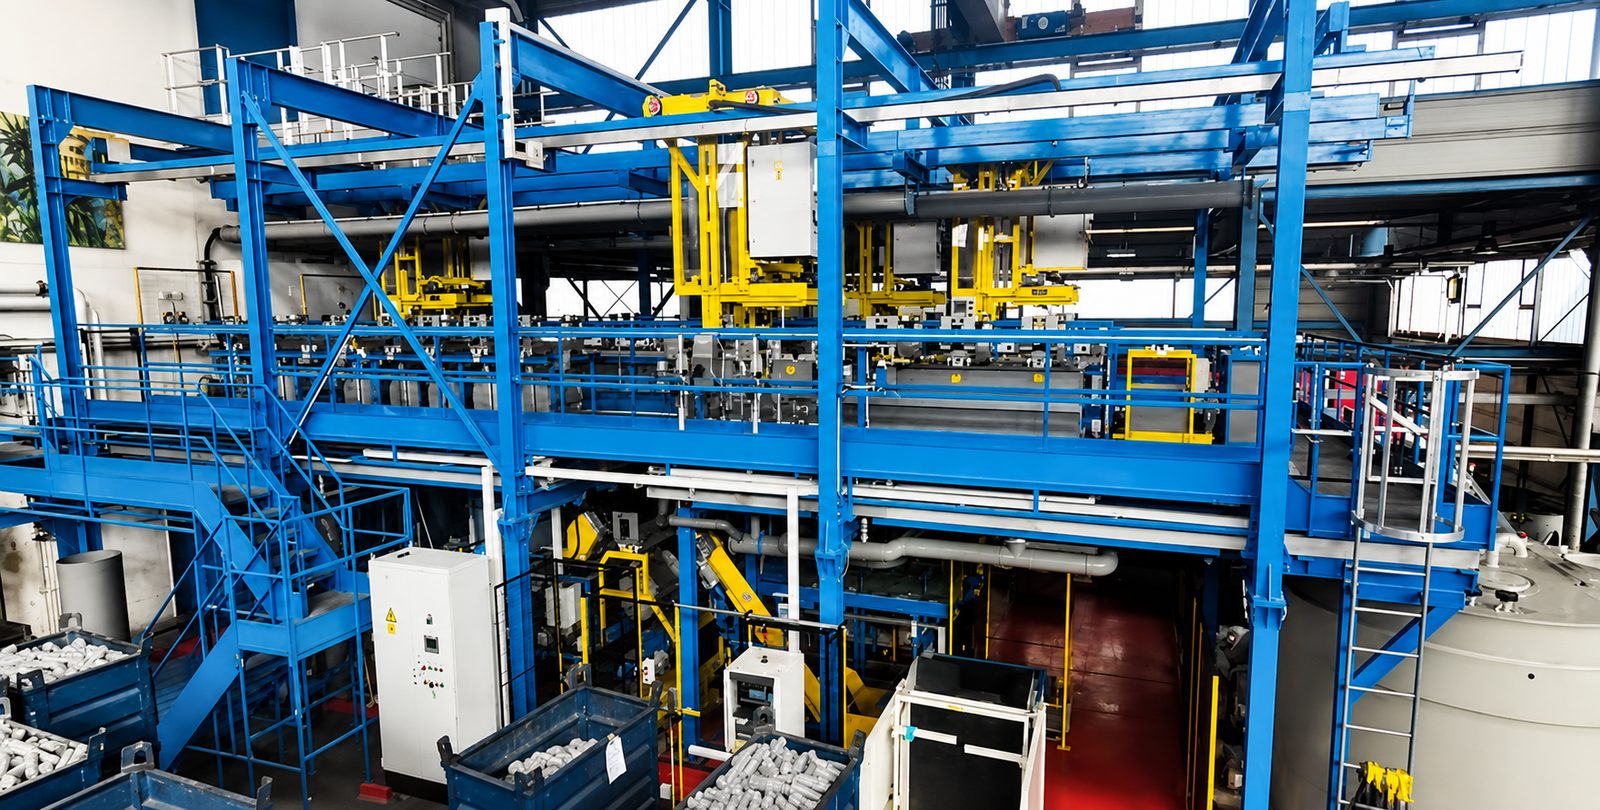
Inside the production
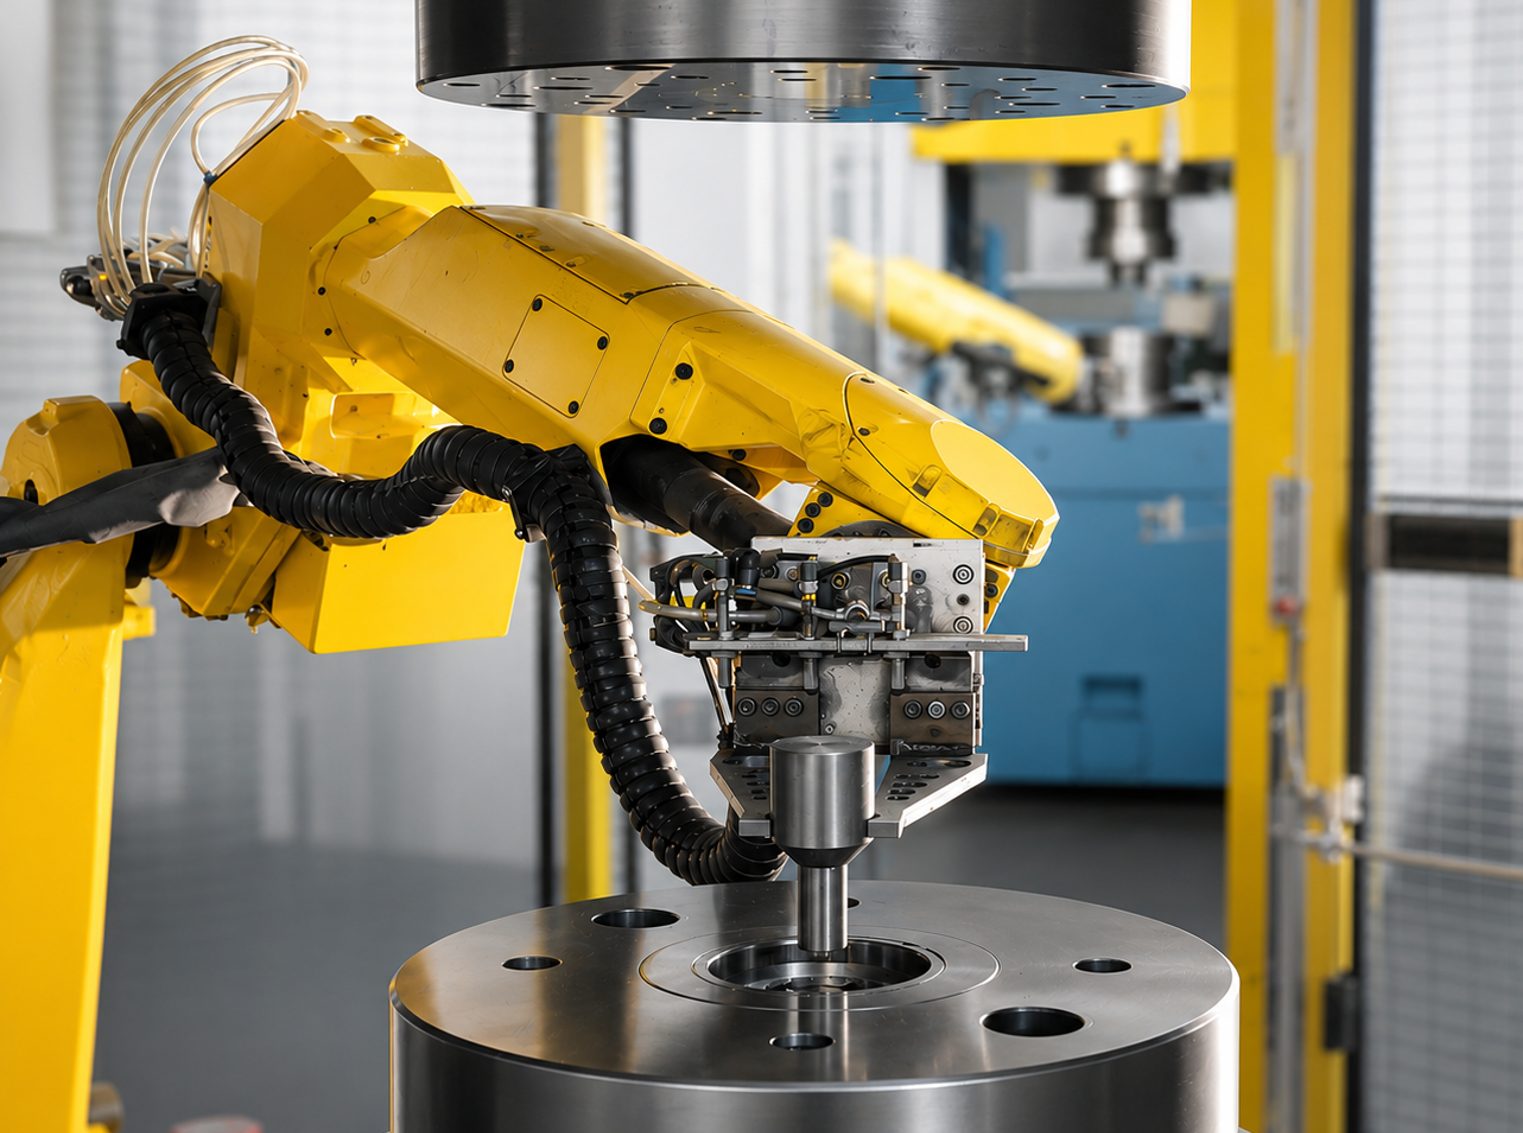
Industries
Processes & technical limits
| Processes | Tolerance | Max. part | Weight | Lot size | Materials |
|---|---|---|---|---|---|
| Cold forming (cold extrusion pressing) of gearing componentsForming | Gear teeth IT8/IT9 after hardening | Ø 240 mm (aluminium), Ø 160 mm | – | 1 unit – 500,000 units | Case-hardening steels, Quenched and tempered steels, Nitriding steels, Stainless steels, EN AW-6082, Pure copper E-Cu |
| Extrusion pressing of profiles, cams, spur and helical gear teeth (up to 4 gear teeth perForming | IT8/IT9 after hardening, machined IT6/IT7 | Ø 240 mm (aluminium), Ø 160 mm | – | 1 unit – 500,000 units | Aluminium wrought alloys (EN AW-6082), Case-hardening, quenched and tempered, nitriding steels, Stainless steels, Pure copper E-Cu |
| Toolmaking (manufacture of toothed extrusion pressing dies)Engineering | – | – | – | – | – |
| 3- and 5-axis millingMachining | IT6/IT7 machined | – | – | – | Quenched and tempered steel, Case-hardening steels |
| Soft machining (turning)Machining | IT6/IT7 machined | – | – | – | Steel, Aluminium, Copper |
| Hard machining: grinding / hard turning (internal + external)Machining | – | – | – | – | Steel |
| Laser cuttingMachining | – | – | – | – | Steel |
| Induction hardening / induction temperingHeat treatment | – | – | – | – | Steel |
| Soft annealing (heat treatment)Heat treatment | – | – | – | – | Steel |
| Washing, preservation, degreasing, molybdenum coating, dephosphating, phosphating (in-houseSurface | – | – | – | – | – |
| Gear tooth millingMachining | – | – | – | – | Steel |
| Gear tooth broachingMachining | – | – | – | – | Steel |
| Gear tooth rollingForming | – | – | – | – | Steel |
| Gear tooth grindingMachining | Quality 6 ground | – | – | – | Steel |
| Hardening / nitridingHeat treatment | – | – | – | – | Steel |
| Controlled shot peeningSurface | – | – | – | – | – |
| Electrochemical polishingSurface | – | – | – | – | – |
| Capacitor discharge weldingJoining | – | – | – | – | – |
| Surface technology (externally via partners)Surface | – | – | – | – | – |
| Design & engineering (gears, gearboxes, tools, clamping fixtures, measuring and testing fixtures)Engineering | – | – | – | – | – |
| Tactile and optical metrology, gear measurement, functional testing, process acceptancesTesting | – | – | – | – | – |
| Assembly of ready-to-install assembliesAssembly | – | – | – | – | – |
8 Anlagen & Maschinen
| Machine | Manufacturer / model | Quantity | Working area | Year built | Site |
|---|---|---|---|---|---|
| Gear measuring machine | Klingelnberg | – | – | – | Frickenhausen |
| Coordinate measuring machine | ZEISS DuraMax | – | – | – | Frickenhausen |
| Optical 3D macroscope | – | – | – | – | Frickenhausen |
| Digital 2D microscope | – | – | – | – | Frickenhausen |
| Double-flank rolling tester (spur and bevel gears) | – | – | – | – | Frickenhausen |
| Contour measuring device | – | – | – | – | Frickenhausen |
| Surface measuring device | – | – | – | – | Frickenhausen |
| Hardness testing devices | – | – | – | – | Frickenhausen |
Additional services
Reference customers
Quality & Metrology
Quality assurance is based on DIN EN ISO 9001:2015 with tactile and optical metrology from Klingelnberg and ZEISS – including a gear measuring machine, CMM DuraMax, double-flank rolling tester, contour, surface and hardness testing devices, functional testing and process acceptances with complete documentation.
| Evidence | Frickenhausen |
|---|---|
| ISO 9001 | |
| ÖKOPROFIT | |
| 100 Companies for Resource Efficiency |
History
- 1948
Founded by Erich Wezel in Frickenhausen
Series supplier in the automotive sector for over 20 years; more than 20 years of experience in aluminium and copper extrusion pressing; e-bike and e-mobility components on the market for over 8 years